Calcium carbonate is a widely used industrial material, and the efficient handling of this material is crucial for many production processes. Pneumatic conveying equipment has emerged as a key solution for transporting calcium carbonate, offering advantages in terms of safety, flexibility, and operational efficiency. This article explores the fundamental principles behind calcium carbonate pneumatic conveying systems and highlights the specific characteristics of their working scenes, providing insights into how these technologies are applied in industrial settings.
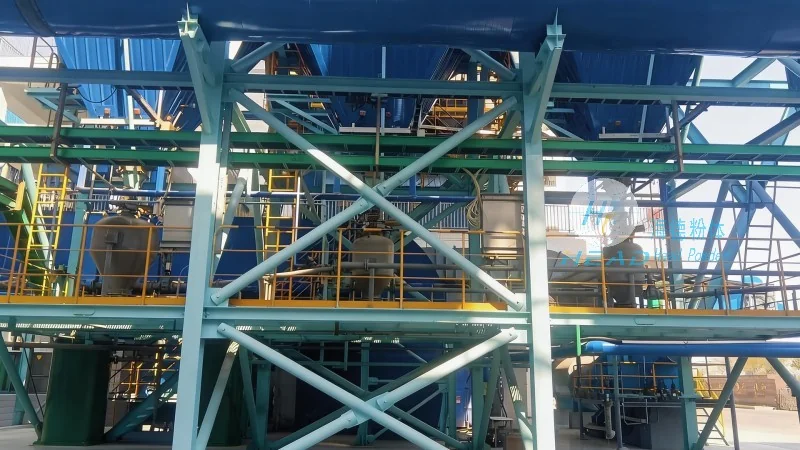
The operation of calcium carbonate pneumatic conveying equipment is based on the principle of transporting bulk materials through a pipeline using a gas stream, typically air. The system works by creating a pressure differential between the inlet and outlet of the conveying line. As air is introduced into the system, it flows through the pipeline, carrying the calcium carbonate particles along with it. This process relies on the interaction between the air flow and the material particles, ensuring that the material is moved from the source to the destination without the need for mechanical components like belts or buckets.
There are two primary types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems operate at higher air velocities, typically moving material in a dispersed state, while dense-phase systems use lower air velocities and higher material concentrations, often requiring a venturi or other pressure-building components. For calcium carbonate applications, the choice between these systems depends on factors such as material properties, distance to be conveyed, and desired flow rates. The dilute-phase system is commonly used for short to medium distances and low to medium material loads, whereas the dense-phase system is preferred for longer distances or when handling fine powders that are prone to clogging.
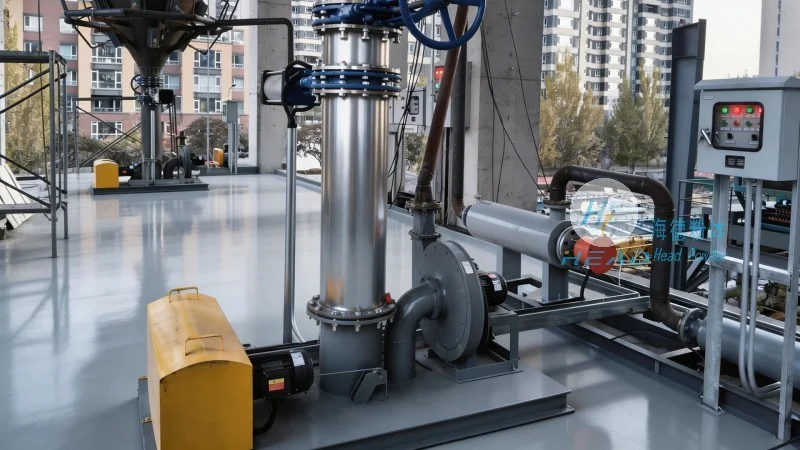
The working scene characteristics of calcium carbonate pneumatic conveying equipment are closely tied to the specific industrial environments where they are deployed. These systems are typically found in processing plants, mining operations, and manufacturing facilities that handle large volumes of calcium carbonate. The key characteristics of these working scenes include high material throughput, the need for dust control, and the requirement for reliable, continuous operation.
In processing plants, calcium carbonate is often used as a filler or a raw material in the production of plastics, paper, and coatings. The pneumatic conveying equipment is integrated into the production line to transport the material from storage silos to processing equipment, such as grinding mills or mixing units. The working scene in these environments is characterized by a clean, controlled atmosphere, with the equipment designed to minimize dust emissions and maintain product purity. The system must also be capable of handling varying material feed rates, as production demands can fluctuate throughout the day.
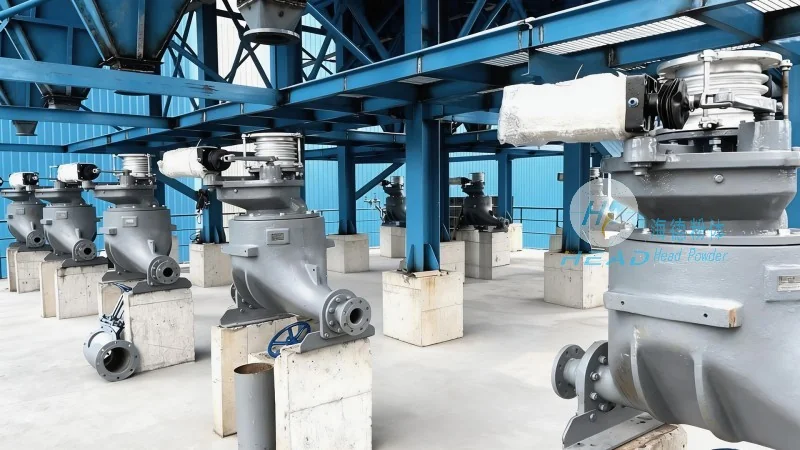
In mining operations, calcium carbonate is extracted from quarries and then transported to processing facilities. The pneumatic conveying equipment is used to move the material from the extraction site to the processing plant, often over long distances. The working scene in this context is more rugged and demanding, with the equipment exposed to harsh environmental conditions, including dust, moisture, and temperature variations. The system must be robust and durable to withstand these conditions while maintaining consistent performance. Additionally, the equipment is often designed to handle coarser material fractions, which may require adjustments to the air velocity and pipeline diameter to ensure efficient transport.
In manufacturing facilities, calcium carbonate is used in the production of various products, including construction materials, food additives, and pharmaceuticals. The working scene in these settings is characterized by a need for precise material control and adherence to strict quality standards. The pneumatic conveying equipment is typically integrated with automated control systems that monitor flow rates, pressure, and material levels. This integration ensures that the material is delivered to the processing equipment at the correct time and in the correct quantity, minimizing waste and optimizing production efficiency. The equipment is also designed to be easy to clean and maintain, as frequent cleaning is often required to prevent material buildup and contamination.
Calcium carbonate pneumatic conveying equipment offers several advantages over traditional mechanical conveying methods. One of the primary benefits is the reduction in labor costs, as the system requires minimal manual intervention for operation and maintenance. Additionally, the equipment is less prone to material degradation, as the material is not subjected to friction or impact during transport. The system also provides better dust control, which is essential for maintaining a safe working environment and complying with environmental regulations.
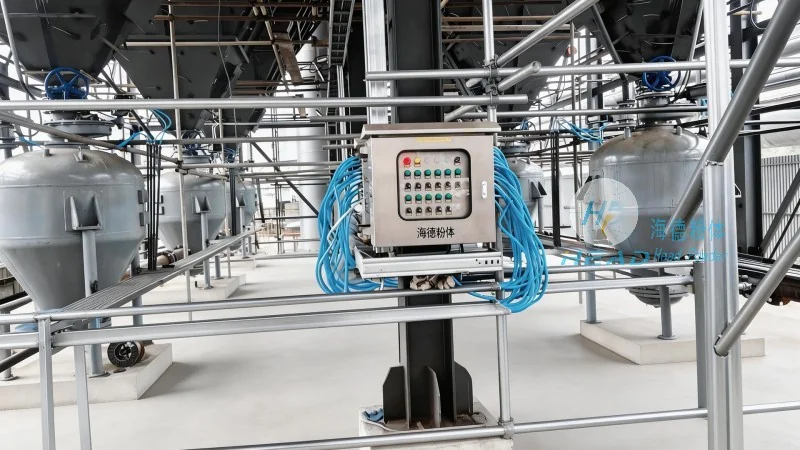
However, there are also considerations to keep in mind when implementing pneumatic conveying systems for calcium carbonate. The initial investment cost can be higher compared to mechanical systems, and the energy consumption is typically higher due to the need to maintain air pressure. The system also requires regular maintenance to ensure optimal performance, including cleaning of the pipeline and replacement of air filters. Furthermore, the choice of system type (dilute-phase or dense-phase) must be carefully evaluated based on the specific application requirements to avoid operational issues such as clogging or reduced efficiency.
Calcium carbonate pneumatic conveying equipment plays a vital role in the efficient handling of this important industrial material. By understanding the core principles of pneumatic conveying and the characteristics of the working scenes where these systems are applied, manufacturers and operators can select the most appropriate equipment for their needs. The technology offers significant advantages in terms of safety, flexibility, and operational efficiency, making it an essential component of modern industrial processes. As the demand for calcium carbonate continues to grow, the importance of reliable and effective pneumatic conveying systems will only increase, driving further innovation in this field.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top