Magnesium oxide (MgO), a crucial industrial material, often requires efficient and reliable transportation systems to ensure smooth production processes. Pneumatic conveying equipment has emerged as a preferred solution for handling MgO due to its ability to transport powders in a dust-free and controlled manner. This article delves into the fundamental principles of pneumatic conveying systems designed for magnesium oxide, alongside an exploration of the specific working scene characteristics that define their application in industrial settings.
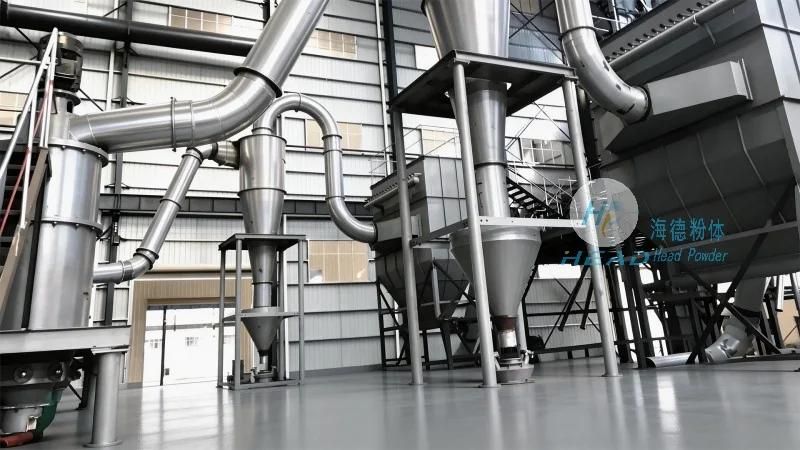
The operation of pneumatic conveying equipment for magnesium oxide is based on the fundamental principle of using air flow to transport particulate materials. Unlike traditional mechanical conveying methods, which rely on belts, buckets, or screws, pneumatic systems utilize compressed air to move powders through a pipeline. This method is particularly advantageous for MgO because it is a fine powder that can be prone to dust generation and requires a system that minimizes contamination and loss. The process typically involves a hopper or feeder that feeds the MgO into a pipeline, where a fan or blower generates a high-velocity air stream. The air stream carries the MgO particles through the pipeline to the discharge point, such as a silo or processing unit. The key to efficient operation lies in maintaining the correct air-to-solid ratio, which ensures that the particles are fully suspended and transported without clogging or degradation.
Several critical components work in tandem to enable the effective pneumatic conveying of magnesium oxide. These include the hopper or feeder, which provides a controlled feed of the material; the air compressor or blower, which generates the necessary air pressure and flow; the pipeline system, which transports the material and air; and the control valves and sensors, which regulate the system's operation. The hopper is designed to prevent material bridging and ensure a consistent feed rate, while the compressor ensures a stable air supply. The pipeline is typically made of materials like stainless steel or plastic to withstand the corrosive nature of MgO and prevent contamination. Control systems, often integrated with sensors that monitor pressure, flow, and material level, allow for real-time adjustments to maintain optimal performance. This integrated approach ensures that the system operates efficiently and safely, minimizing downtime and maximizing material throughput.
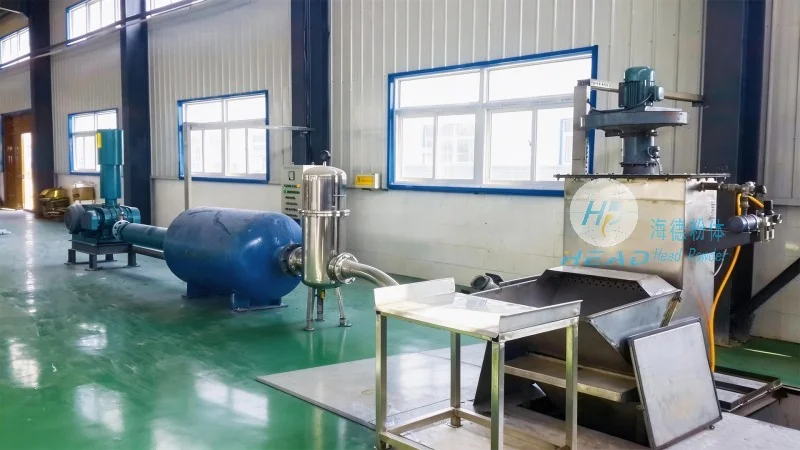
The working scene characteristics of magnesium oxide pneumatic conveying equipment are tailored to meet the specific demands of industrial applications. These systems are commonly used in industries such as chemical manufacturing, pharmaceuticals, and food processing, where the handling of fine powders is critical. The primary benefits of using pneumatic conveying for MgO include dust-free operation, which enhances workplace safety and reduces environmental impact; reduced material loss, as the system minimizes spillage and leakage; and improved process control, as the equipment allows for precise regulation of material flow. Additionally, pneumatic systems are adaptable to various production scales, from small-scale laboratory applications to large-scale industrial operations. The flexibility of these systems enables them to be integrated into existing production lines or used as standalone units, depending on the specific requirements of the facility. In industrial settings, the ability to transport MgO from storage silos to processing equipment without manual handling significantly improves operational efficiency and reduces labor costs.
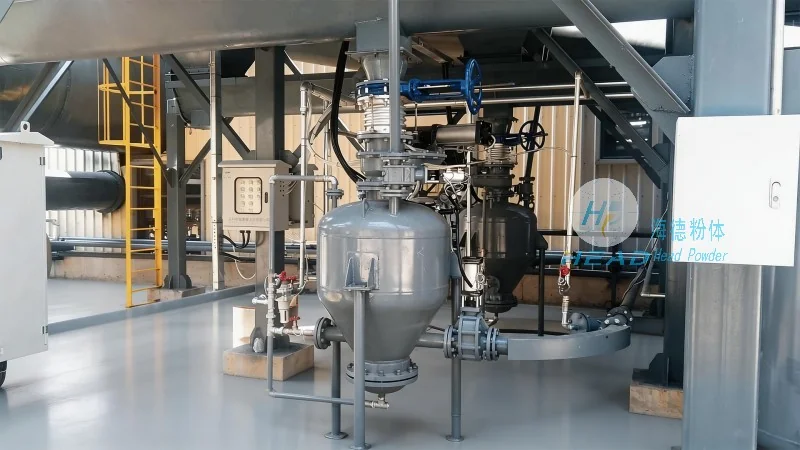
Consider a chemical plant that processes magnesium oxide for use in refractory materials. The plant uses a pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. (commonly known as headpowder) to transport MgO from a storage silo to a mixing and grinding unit. The system consists of a stainless steel pipeline, a high-capacity blower, and a control panel that monitors the air flow and material level. The plant operators report that the system has significantly reduced dust exposure, as the enclosed pipeline prevents the release of fine particles into the air. Additionally, the system has minimized material loss, as the hopper and feeder ensure a consistent feed rate and prevent clogging. The control system allows for precise adjustment of the air flow, which optimizes the conveying efficiency and reduces energy consumption. This case study illustrates how the working scene characteristics of the pneumatic conveying equipment are tailored to the specific needs of the chemical plant, resulting in improved safety, efficiency, and cost-effectiveness.
In conclusion, pneumatic conveying equipment plays a vital role in the efficient and safe handling of magnesium oxide. The fundamental principles of air flow and particle suspension, combined with specialized components and tailored working scene characteristics, make these systems ideal for industrial applications. The benefits of dust-free operation, reduced material loss, and improved process control are significant advantages that contribute to enhanced workplace safety and operational efficiency. As industries continue to rely on magnesium oxide for various applications, the importance of reliable and effective conveying systems will only grow. Companies like Shandong HeadPowder Engineering Co., Ltd. (headpowder), with their expertise in designing and manufacturing pneumatic conveying equipment, are instrumental in meeting the evolving needs of the industry. By understanding the core principles and working scene characteristics of these systems, industrial facilities can optimize their material handling processes and achieve greater productivity and safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top