Shandong HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in the design, development, and application of slurry and powder conveying systems. The company, commonly known as HeadPowder, focuses on providing efficient and reliable solutions for material transportation in various industrial sectors.
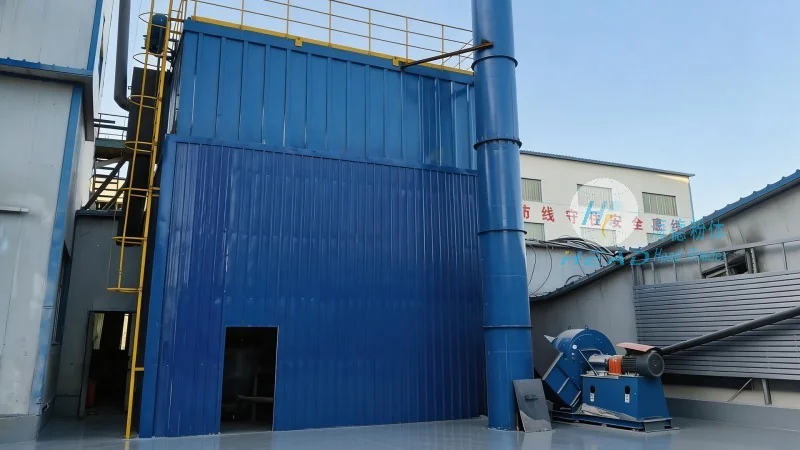
At the heart of slurry and powder conveying systems lies a sophisticated integration of fluid dynamics, mechanical engineering, and material science. These systems are engineered to handle a wide range of materials, from fine powders to dense slurries, ensuring consistent and controlled transport. The fundamental principle involves the use of pumps, pipelines, and sometimes pneumatic or hydraulic components to move materials through a closed or semi-closed system. Key factors such as viscosity, particle size, and flow rate are carefully considered during the design phase to optimize performance and minimize energy consumption.
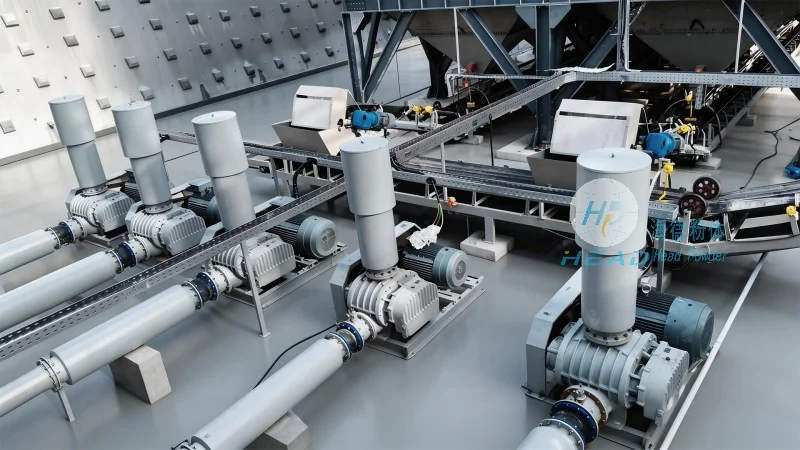
Slurry and powder conveying systems are widely employed across diverse industrial applications, each presenting unique challenges and requirements. For instance, in mining operations, these systems are crucial for transporting ore slurries from processing plants to storage facilities, ensuring a continuous flow of raw materials. In the chemical industry, they facilitate the handling of reactive powders and viscous slurries, maintaining safety and operational efficiency. Additionally, in the food and pharmaceutical sectors, specialized conveying systems are used to transport bulk ingredients and finished products, adhering to stringent hygiene and quality standards.
HeadPowder's slurry and powder conveying systems are designed with flexibility and adaptability in mind. The company offers a range of solutions tailored to specific operational needs, including high-pressure pumps, flexible hoses, and modular pipeline configurations. Advanced materials, such as corrosion-resistant alloys and food-grade plastics, are utilized to ensure durability and compliance with industry regulations. Moreover, the systems can be integrated with automation and control technologies, enabling real-time monitoring and adjustment of flow rates, pressure, and other critical parameters. This level of customization allows clients to achieve optimal performance while reducing downtime and maintenance costs.
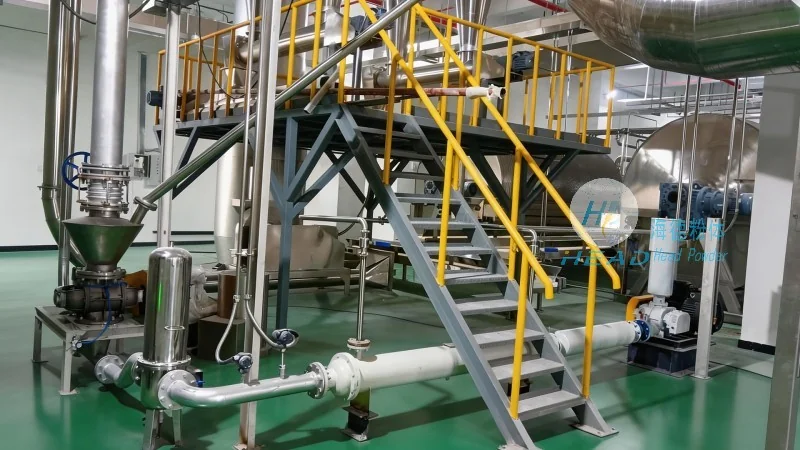
Reliability is a top priority in the design and operation of slurry and powder conveying systems. HeadPowder employs rigorous testing and quality control measures to ensure that each system meets or exceeds industry standards. Regular maintenance and service programs are also available to keep the equipment in peak condition, minimizing the risk of breakdowns and maximizing operational uptime. By leveraging their expertise in fluid dynamics and material handling, HeadPowder provides solutions that enhance productivity and reduce operational costs for their clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top