Positive pressure dilute phase pneumatic conveying systems represent a sophisticated method for transporting bulk materials through a pipeline using pressurized air. This technology is widely utilized across various industries due to its efficiency, flexibility, and ability to handle a broad range of materials. The fundamental principle involves the creation of a high-pressure air stream that propels particles through the conveying line, ensuring consistent and reliable material transport. The system operates by introducing the material into the pipeline at a controlled rate, often with a feeding device such as a rotary valve or a screw feeder, while maintaining a positive pressure environment that prevents air leakage and maintains material flow. The air pressure is typically maintained above atmospheric levels, ensuring that the material is continuously carried along the pipeline without settling or clogging. This method is particularly effective for materials that are fine, powdery, or have a tendency to agglomerate, as the high-velocity air stream helps to keep particles suspended and prevents blockages. The system's design allows for long-distance transport with minimal pressure drop, making it suitable for applications where material needs to be moved over significant distances. The positive pressure aspect also ensures that the conveying line remains sealed, reducing the risk of dust emissions and environmental contamination. Overall, the principle of positive pressure dilute phase pneumatic conveying is centered on the efficient use of air as a conveying medium, combined with precise control of material feed and air pressure to achieve optimal performance.
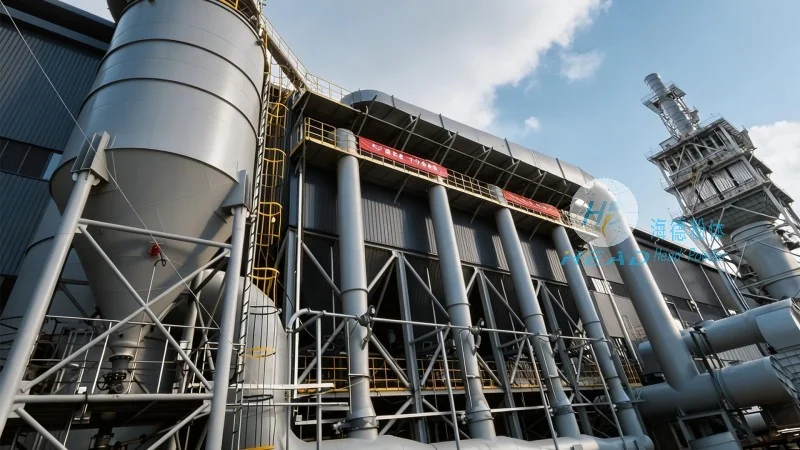
The core working principle of a positive pressure dilute phase pneumatic conveying system revolves around the generation of a high-pressure air stream that is used to transport particulate materials. The system operates by creating a pressure differential between the inlet and outlet of the conveying line. At the inlet, the material is introduced into the pipeline, often mixed with the pressurized air stream. The air velocity is maintained at a level sufficient to keep the particles in suspension, typically ranging from 20 to 40 meters per second, depending on the material properties and pipeline diameter. The positive pressure is maintained throughout the system, ensuring that the air and material mixture remains under pressure, which prevents the material from settling and reduces the risk of blockages. The system typically includes components such as a blower or compressor to generate the necessary air pressure, a feeder to control the material feed rate, and a conveying line with appropriate diameter and length. The design of the system is crucial for ensuring efficient material transport, as the air velocity and pressure must be optimized for the specific material being conveyed. The principle also involves the use of a receiver or discharge device at the end of the pipeline to collect the material, which may include a cyclone separator or a filter to separate the material from the air stream. The air is then typically returned to the blower or released into the atmosphere, depending on the system configuration. This closed-loop or open-loop system ensures that the material is transported efficiently and with minimal loss or contamination.
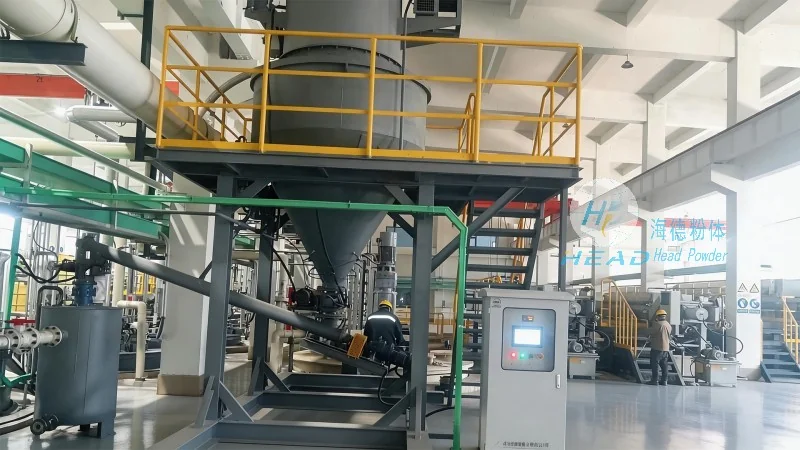
Positive pressure dilute phase pneumatic conveying systems are employed in a variety of industrial applications, each with specific characteristics that make them suitable for particular scenarios. One of the primary applications is in the food and pharmaceutical industries, where the system is used to transport powders and granules that require strict contamination control. The positive pressure environment helps to maintain a clean and sterile environment, preventing the ingress of external contaminants and ensuring product quality. In these industries, the system is often used for transporting ingredients such as flour, sugar, or pharmaceutical powders from storage silos to processing equipment. The ability to maintain a positive pressure and control the material flow rate is critical for meeting regulatory requirements and ensuring product consistency. Another key application is in the chemical and petrochemical sectors, where the system is used to transport various powders and granules, including chemicals, catalysts, and raw materials. The high-pressure air stream allows for the efficient transport of these materials over long distances, often with minimal degradation or change in properties. The system's flexibility also makes it suitable for handling a wide range of materials, from fine powders to larger granules, making it a versatile solution for chemical processing plants. In the mining and minerals industry, positive pressure dilute phase pneumatic conveying is used to transport bulk materials such as ores, minerals, and coal from processing facilities to storage or further processing units. The system's ability to handle abrasive and heavy materials makes it ideal for these applications, as it can withstand the wear and tear associated with transporting such materials. The positive pressure aspect also helps to prevent dust emissions, which is important for environmental compliance in mining operations. Additionally, the system is used in the agricultural sector for transporting grain, feed, and other agricultural products. The ability to maintain a positive pressure and control the material flow rate ensures that the grain is transported efficiently and without damage, which is crucial for maintaining product quality. The system's design allows for the transport of large quantities of material over long distances, making it suitable for agricultural processing facilities and grain elevators. Overall, the application characteristics of positive pressure dilute phase pneumatic conveying systems are tailored to meet the specific needs of various industries, ensuring efficient and reliable material transport while maintaining product quality and environmental standards.
When considering the operational scenarios for positive pressure dilute phase pneumatic conveying systems, several advantages and considerations come into play. One of the primary advantages is the ability to transport materials over long distances with minimal pressure drop, which reduces the energy consumption and operating costs of the system. The positive pressure environment also ensures that the conveying line remains sealed, preventing dust emissions and reducing the risk of environmental contamination. This is particularly important in industries where dust control is a regulatory requirement, such as in the food and pharmaceutical sectors. Another advantage is the system's flexibility, which allows for the transport of a wide range of materials, from fine powders to larger granules, without the need for significant modifications to the system. The ability to adjust the air pressure and material feed rate allows for precise control over the material flow, ensuring consistent and reliable transport. However, there are also several considerations that must be taken into account when operating such systems. The high-pressure air stream can generate significant noise and vibration, which may require noise reduction measures and vibration control equipment. Additionally, the system's components, such as the blower and conveying line, may require regular maintenance to ensure optimal performance and prevent breakdowns. The material properties, such as particle size, density, and moisture content, can also affect the system's performance, requiring careful selection of the system design and operating parameters. The positive pressure aspect also means that the system must be properly sealed to prevent air leakage, which can reduce the efficiency of the system and increase energy consumption. Overall, the operational scenarios for positive pressure dilute phase pneumatic conveying systems require careful consideration of the material properties, system design, and maintenance to ensure optimal performance and efficiency.
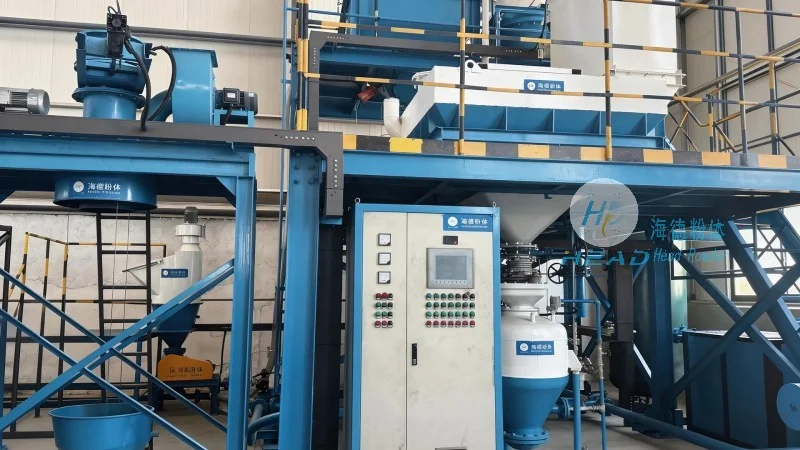
Positive pressure dilute phase pneumatic conveying systems offer a reliable and efficient method for transporting bulk materials in various industrial applications. The system's ability to maintain a positive pressure environment, combined with precise control of material feed and air pressure, ensures consistent and reliable material transport. The system is widely used across industries such as food, pharmaceutical, chemical, mining, and agriculture, due to its versatility and ability to handle a broad range of materials. The advantages of the system, including long-distance transport, minimal pressure drop, and reduced dust emissions, make it a preferred choice for many applications. However, the operational scenarios require careful consideration of material properties, system design, and maintenance to ensure optimal performance. As a leading provider of engineering solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of positive pressure dilute phase pneumatic conveying systems. With years of experience and expertise in the field, the company offers customized solutions tailored to the specific needs of its clients. The company's commitment to quality and innovation ensures that its systems meet the highest standards of performance and reliability. Based in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. serves clients globally, providing comprehensive support from system design to installation and maintenance. The company's focus on customer satisfaction and technical excellence has made it a trusted partner for businesses seeking efficient and reliable material transport solutions. Whether for short or long-distance transport, the positive pressure dilute phase pneumatic conveying system remains a viable and effective solution for bulk material handling. With the right system design and operational parameters, businesses can achieve optimal performance and efficiency in their material transport processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top