HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling bentonite and other fine powders. This article delves into the fundamental principles of bentonite pneumatic conveying equipment and highlights the key characteristics of its working scenarios, providing a comprehensive overview for industry professionals seeking efficient material transport solutions.
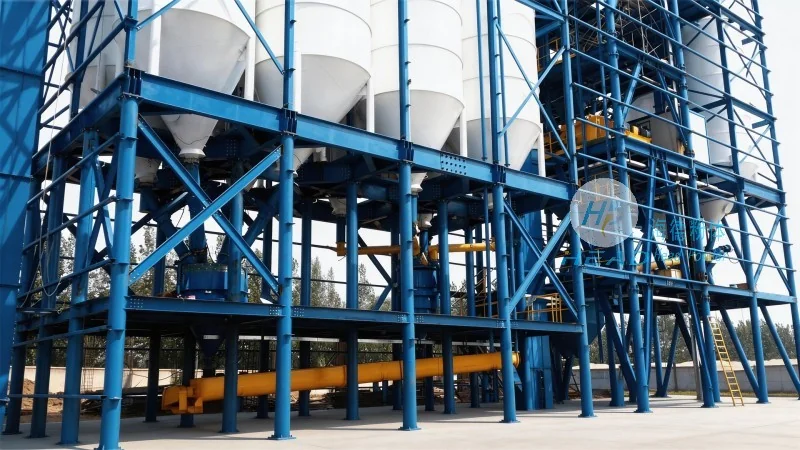
Bentonite, a natural clay mineral widely used in various industrial applications such as drilling fluids, foundry sand, and environmental remediation, presents unique challenges when it comes to material handling due to its fine particle size and hygroscopic properties. Traditional methods like belt conveyors or bucket elevators often struggle with dust generation, material degradation, and operational inefficiencies. Pneumatic conveying offers a solution by utilizing air flow to transport powders through a sealed system, minimizing contamination and ensuring consistent product quality.
The fundamental principle of bentonite pneumatic conveying involves the creation of a controlled air stream that lifts and transports the powder particles. This process can be categorized into two main types: aspiration (suction) systems and compression (pressure) systems. Aspiration systems use a vacuum at the receiving end to draw material from the source, while compression systems employ a positive pressure at the discharge end to push material through the pipeline. Both systems rely on the balance between air velocity and particle size to achieve stable transport, with the air velocity typically maintained above the minimum fluidization velocity to prevent particle settling.
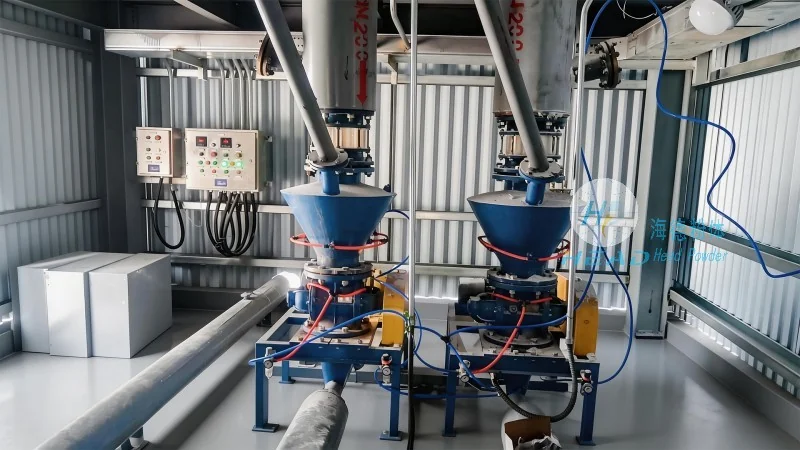
A typical bentonite pneumatic conveying system consists of several critical components that work in tandem to ensure reliable operation. The primary components include the feed hopper, airlock feeder, conveying pipeline, separator, and dust collector. The feed hopper stores the bentonite material and regulates the flow rate, while the airlock feeder prevents air leakage and ensures a consistent feed to the pipeline. The conveying pipeline, often made of stainless steel or plastic, transports the material and air mixture. The separator, usually a cyclone or bag filter, separates the bentonite particles from the air stream, and the dust collector captures any residual dust to meet environmental regulations.
The working scene characteristics of bentonite pneumatic conveying equipment are defined by its adaptability to diverse industrial environments and the specific requirements of bentonite handling. These characteristics include high efficiency in material transport, minimal dust generation, and the ability to handle fine powders without degradation. In the chemical industry, bentonite is used as a thickener or filter aid, and pneumatic conveying ensures that the material is delivered to processing units without contamination. In the construction sector, bentonite is used in foundry sand and concrete additives, where the system's ability to maintain particle integrity is crucial for product performance.
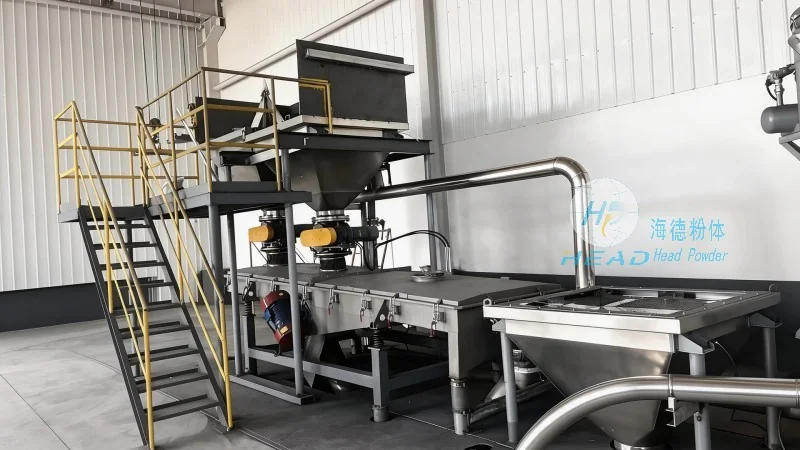
One of the key advantages of bentonite pneumatic conveying is its flexibility in handling varying material properties. The system can be configured to accommodate different particle sizes, moisture contents, and flow rates, making it suitable for both small-scale laboratory applications and large-scale industrial production. Additionally, the sealed system design reduces the risk of material exposure to the environment, enhancing safety and compliance with occupational health standards. This makes the equipment particularly valuable in industries where dust control and product purity are paramount.
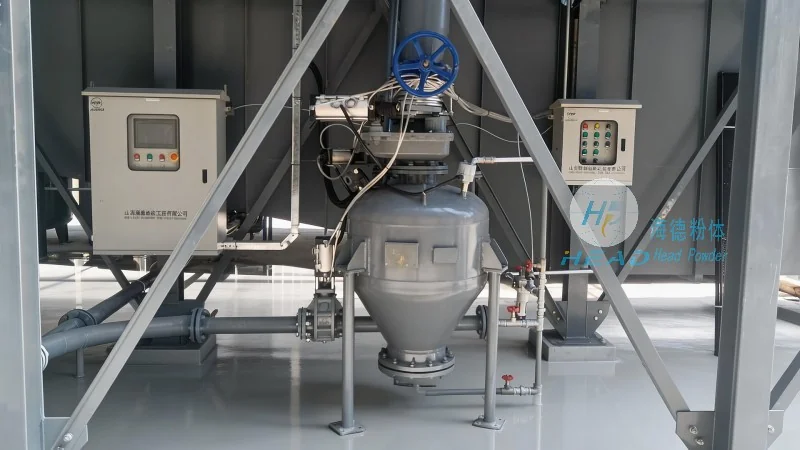
Efficient operation of bentonite pneumatic conveying equipment depends on proper system design and regular maintenance. The air velocity must be optimized to prevent particle deposition on pipeline walls, which can lead to blockages and reduced system performance. Regular cleaning of the separator and dust collector is essential to maintain airflow efficiency and prevent dust accumulation. Additionally, the feed hopper and airlock feeder should be checked for wear and tear to ensure consistent material flow. HeadPowder, with its expertise in pneumatic conveying systems, provides comprehensive support, including system design, installation, and maintenance services to ensure optimal performance and longevity of the equipment.
In conclusion, bentonite pneumatic conveying equipment, as exemplified by the solutions offered by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated and efficient approach to handling fine powders. By understanding the fundamental principles and working scene characteristics, industry users can leverage these systems to improve operational efficiency, maintain product quality, and comply with environmental regulations. The adaptability and reliability of pneumatic conveying make it an indispensable technology in the modern handling of bentonite and other similar materials.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top