HeadPowder, a leading provider in the field, specializes in advanced pneumatic conveying solutions. The company, Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China, and has established itself as a key player in the industrial automation and material handling sector. This article delves into the core principles of intelligent pneumatic conveying systems and explores their diverse application scenarios, highlighting how these technologies enhance operational efficiency and reliability in various industrial settings.
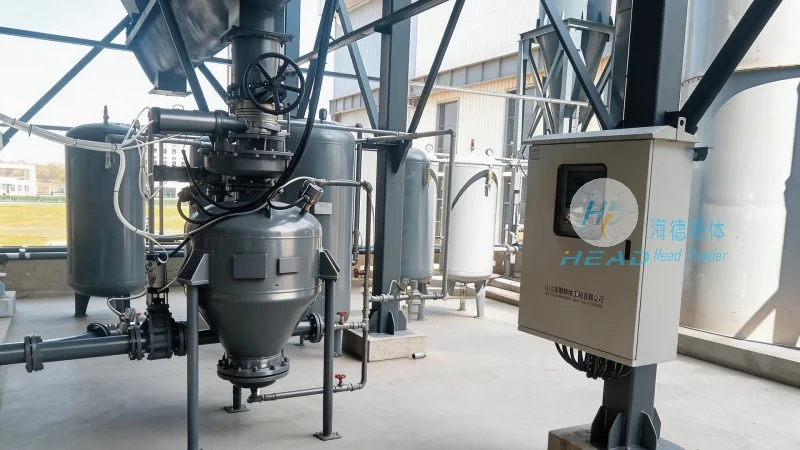
Intelligent pneumatic conveying systems operate on the fundamental principle of using air pressure to transport bulk materials. Unlike traditional methods that rely on mechanical components like belts or buckets, these systems utilize a closed-loop air flow to move powders, granules, and other particulate materials from one location to another. The system typically consists of a series of components, including a material hopper, a conveying line (often equipped with bends and filters), a control unit (featuring programmable logic controllers and sensors), and a discharge device (such as a rotary valve or cyclone separator). The intelligent aspect lies in the advanced control algorithms and sensors that monitor and adjust the air pressure, flow rate, and material feed rate in real-time. This dynamic adjustment ensures optimal performance, minimizes material degradation, and reduces energy consumption. The system's ability to handle a wide range of materials—from fine powders to bulk granules—makes it versatile for various industrial applications. For instance, in the chemical industry, the system can handle corrosive powders with specialized materials of construction, while in the food industry, it can be designed to meet sanitary standards with stainless steel components and CIP (clean-in-place) capabilities.
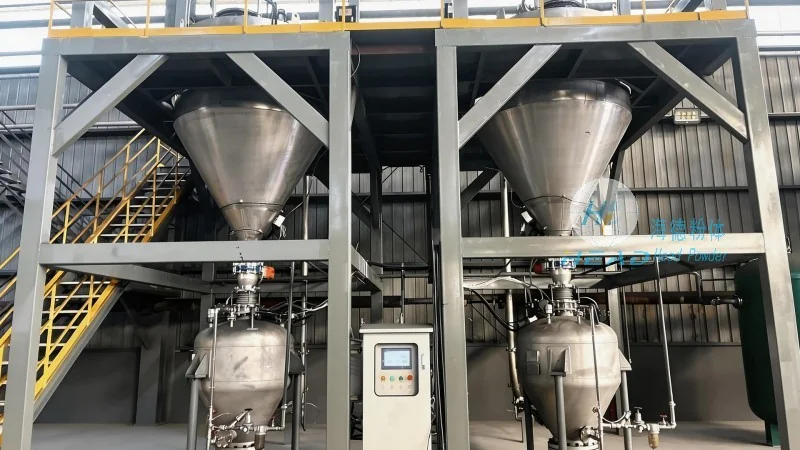
Intelligent pneumatic conveying systems are widely adopted across multiple industries due to their adaptability and efficiency. In the pharmaceutical industry, for example, these systems are used to transport sensitive powders with high precision, ensuring minimal contamination and maintaining product integrity. The food processing sector benefits from the hygienic design of these systems, which prevents cross-contamination and complies with stringent regulatory standards. In the chemical industry, the systems handle hazardous materials safely, with integrated safety features that automatically shut down the system in case of pressure or flow abnormalities. Another significant application is in the cement and construction materials industry, where large volumes of bulk materials are efficiently transported over long distances. The flexibility of the system allows it to be customized for different material types and process requirements, making it a reliable choice for both new installations and retrofitting existing facilities. Additionally, the systems are suitable for applications requiring dust-free environments, such as in the electronics manufacturing sector, where particulate contamination must be strictly controlled.
Compared to traditional mechanical conveying methods, intelligent pneumatic conveying systems offer several advantages. The primary benefit is the reduction in maintenance costs, as there are fewer moving parts and less wear and tear. The systems also provide better control over material flow, which leads to improved product quality and reduced waste. Additionally, the closed-loop design minimizes dust emissions, contributing to a cleaner and safer working environment. The intelligent control systems enable remote monitoring and diagnostics, allowing for proactive maintenance and quick troubleshooting. This not only enhances operational uptime but also extends the lifespan of the equipment. For industries that require high throughput and consistent material handling, these systems are particularly advantageous, as they can handle large volumes with minimal downtime. Furthermore, the systems are energy-efficient, with the ability to adjust air pressure and flow based on real-time demand, reducing overall operational costs.
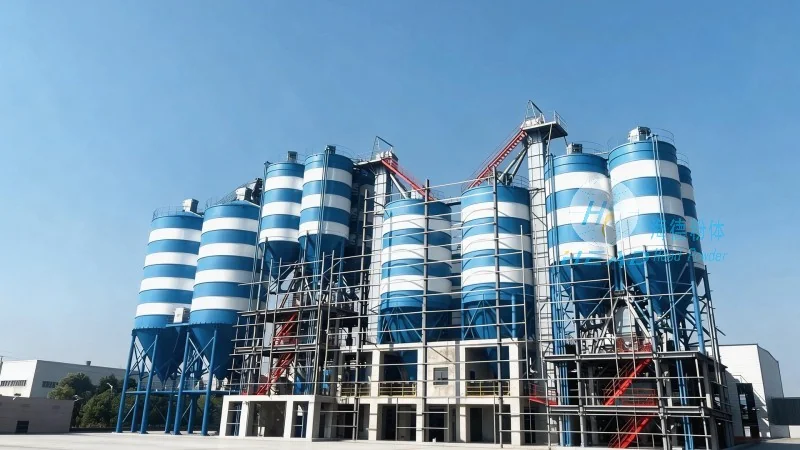
As industries continue to demand more efficient and reliable material handling solutions, intelligent pneumatic conveying systems remain a top choice. HeadPowder's expertise in designing and implementing these systems ensures that clients receive tailored solutions that meet their specific needs. The integration of advanced technology, such as AI-driven control and predictive maintenance, further enhances the performance and longevity of these systems. With a focus on innovation and customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. is positioned to lead the way in the evolution of pneumatic conveying technologies, providing sustainable and efficient solutions for the future of industrial material handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top