HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced solutions for material handling, particularly in the field of pneumatic conveying systems designed for stone materials. This article delves into the working principle and key features of such equipment, offering insights into how these systems efficiently transport bulk materials like gravel, crushed stone, and other similar granular substances.
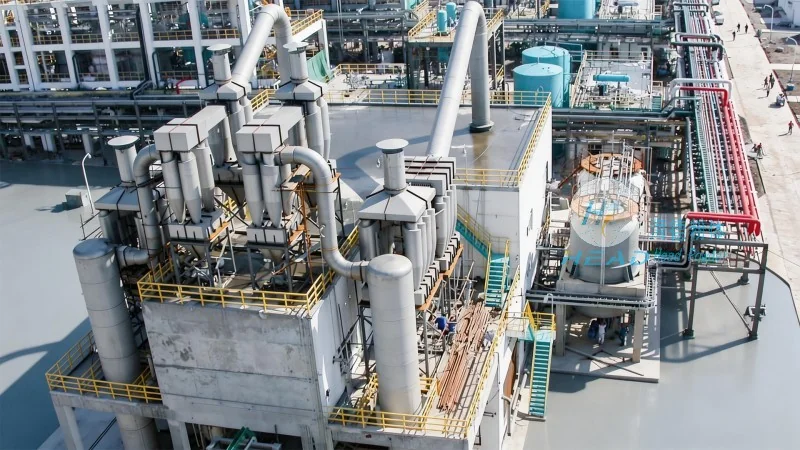
Pneumatic conveying equipment operates by utilizing air or gas to transport solid materials through a pipeline. In the case of stone materials, the system typically involves a combination of positive and negative pressure zones to move the material from the source to the destination. The process begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. Air is then introduced into the system, either by creating a vacuum (negative pressure) or by blowing air under pressure (positive pressure). This airflow creates a flow of material along the pipeline, ensuring efficient and continuous transport without the need for mechanical components like belts or buckets.
The core components of a pneumatic conveying system for stone materials include the hopper, feeder, conveying line, and receiver. The hopper stores the stone material and feeds it into the system at a controlled rate. The feeder ensures a consistent flow of material into the conveying line. The conveying line, often made of stainless steel or other corrosion-resistant materials, transports the material through the system. The receiver collects the material at the end of the line, where it is discharged for further processing or storage. The system may also include additional components such as filters, cyclones, or silos to manage dust and ensure proper material handling.
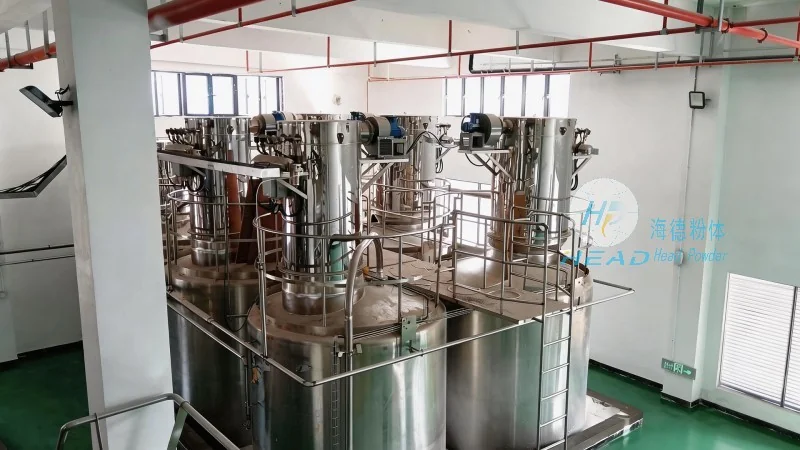
One of the primary advantages of pneumatic conveying systems for stone materials is their ability to handle abrasive and heavy materials without causing wear and tear on the equipment. The design of the conveying line and components is optimized to withstand the impact and friction of moving stone particles, ensuring long-term durability and minimal maintenance. Additionally, these systems are highly flexible, allowing for changes in the layout or direction of the conveying line without significant modifications to the overall system.
Another notable feature is the system's ability to maintain a clean and dust-free environment. By using enclosed pipelines and proper filtration, the equipment minimizes dust emissions, making it suitable for applications where air quality is a concern. This is particularly important in industries such as construction, mining, and aggregate processing, where dust control is essential for safety and regulatory compliance.
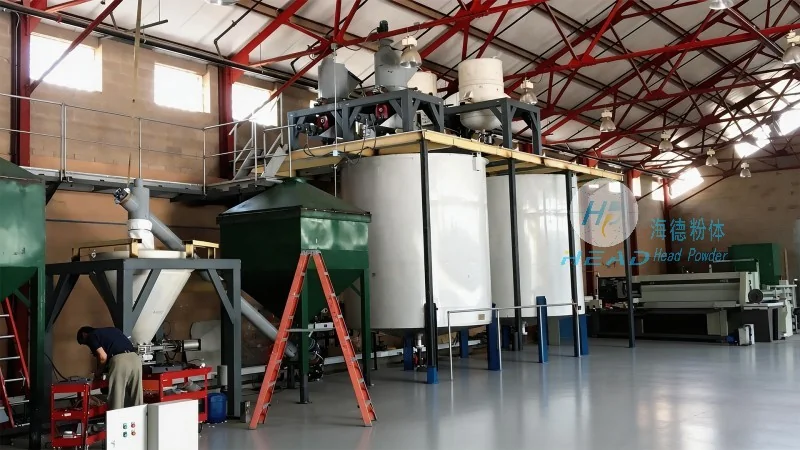
Efficiency is a critical feature of pneumatic conveying systems. The use of air as the conveying medium allows for high-speed transport of materials, reducing the time and labor required for material handling. The system can handle large volumes of stone material, making it ideal for high-throughput applications. Furthermore, the system's ability to operate continuously without the need for frequent stops or maintenance minimizes downtime and increases overall productivity.
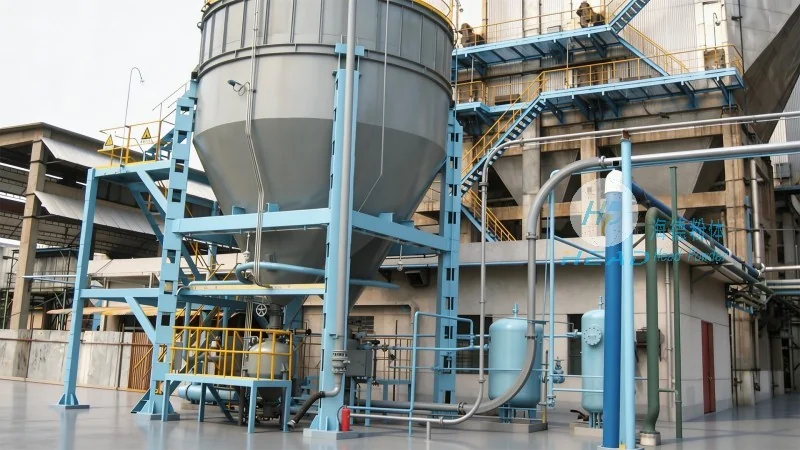
Pneumatic conveying equipment for stone materials is widely used in various industries, including construction, mining, and aggregate processing. In construction, these systems are used to transport gravel, crushed stone, and other aggregates from storage to mixing plants or construction sites. In mining operations, they are employed to move crushed ore or rock from processing facilities to storage areas. The benefits of using such systems include improved safety, reduced labor costs, and increased efficiency in material handling processes.
HeadPowder's expertise in designing and manufacturing pneumatic conveying systems ensures that clients receive customized solutions tailored to their specific needs. The company's commitment to quality and innovation has made it a trusted partner in the industry, providing reliable and efficient equipment for material handling applications. By understanding the working principle and features of these systems, businesses can make informed decisions about implementing pneumatic conveying solutions that enhance their operational efficiency and productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top