Lignite, also known as brown coal, is a crucial energy resource with high moisture content and variable particle size. Traditional transportation methods like belt conveyors or trucks often face challenges such as material degradation, high maintenance costs, and environmental pollution. Pneumatic conveying technology offers a more efficient and flexible solution for handling lignite, enabling companies to optimize their logistics processes and reduce operational expenses. This article explores the application and optimization of pneumatic conveying systems specifically tailored for lignite transportation, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. (hereinafter referred to as HeadPowder) in designing and implementing advanced solutions.
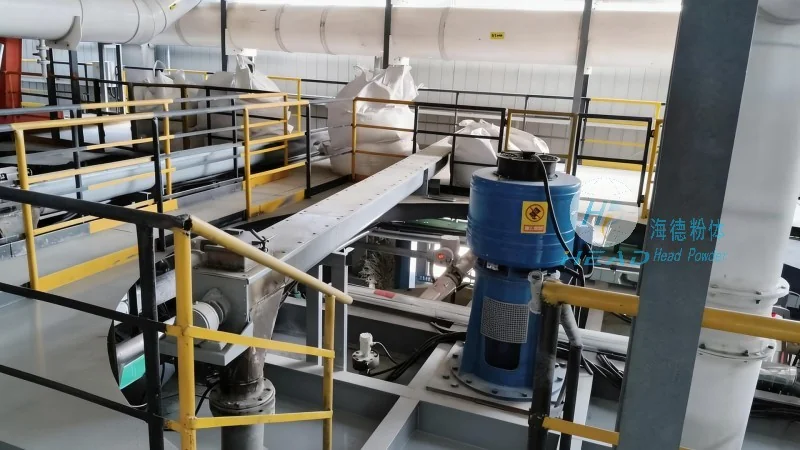
HeadPowder specializes in developing customized pneumatic conveying systems that address the unique characteristics of lignite. The primary advantages include: enhanced material handling efficiency, reduced environmental impact, and improved safety in industrial operations. By using air as the conveying medium, the system minimizes dust generation and prevents material contamination, which is critical for maintaining the quality of lignite. Additionally, pneumatic conveying allows for continuous, automated transport, reducing labor costs and increasing production throughput. The technology also supports flexible routing, enabling seamless integration with existing infrastructure in mining and power generation facilities.
HeadPowder employs a comprehensive approach to design and optimize pneumatic conveying systems for lignite. The process begins with a thorough analysis of the lignite properties, including moisture content, particle size distribution, and bulk density. This data is used to select the appropriate conveying system type—such as dilute-phase or dense-phase systems—based on the specific application requirements. For example, dilute-phase systems are ideal for long-distance transport with low material concentration, while dense-phase systems are preferred for short distances or when high material density is needed. The company also considers factors like energy consumption, system reliability, and maintenance requirements to ensure the final design meets both performance and cost objectives.
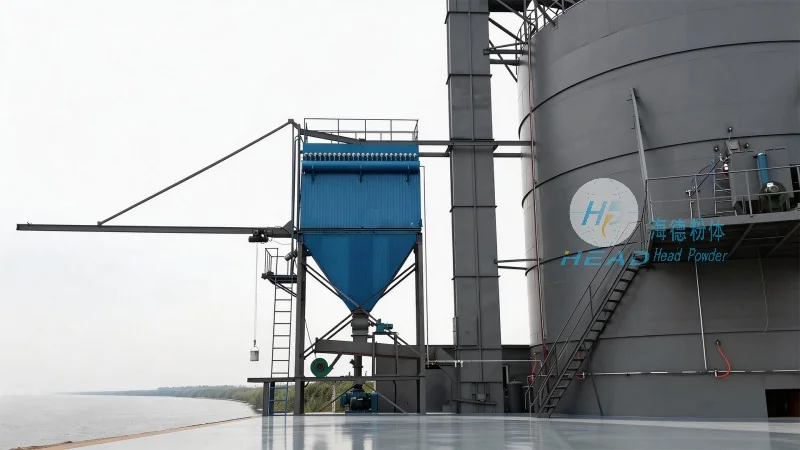
HeadPowder understands that each lignite project has distinct requirements, whether it involves transporting raw lignite from mines to processing plants or delivering finished products to power stations. The company offers tailored solutions that can be adapted to various scenarios. For instance, in a mine-to-power plant setup, a combination of dilute-phase and dense-phase conveying may be used to optimize both efficiency and cost. The system design includes components such as rotary valves, airlocks, and cyclone separators to ensure smooth material flow and prevent blockages. Furthermore, HeadPowder integrates advanced control systems that monitor pressure, flow rate, and material levels in real-time, allowing for immediate adjustments to maintain optimal operation. This level of automation enhances system reliability and reduces downtime, which is essential for continuous production in the energy sector.
One of the significant advantages of pneumatic conveying systems for lignite is their environmental friendliness. Unlike traditional methods that generate dust and require water for dust suppression, pneumatic conveying uses compressed air, which can be filtered and recycled, minimizing waste. The reduced dust emission not only improves air quality at the site but also lowers the risk of respiratory issues for workers. Additionally, the system’s compact design and low noise levels contribute to a safer working environment. From an operational perspective, the automated control systems reduce the need for manual intervention, lowering labor costs and improving overall productivity. HeadPowder’s solutions are designed to meet stringent environmental regulations, ensuring compliance while delivering superior performance.
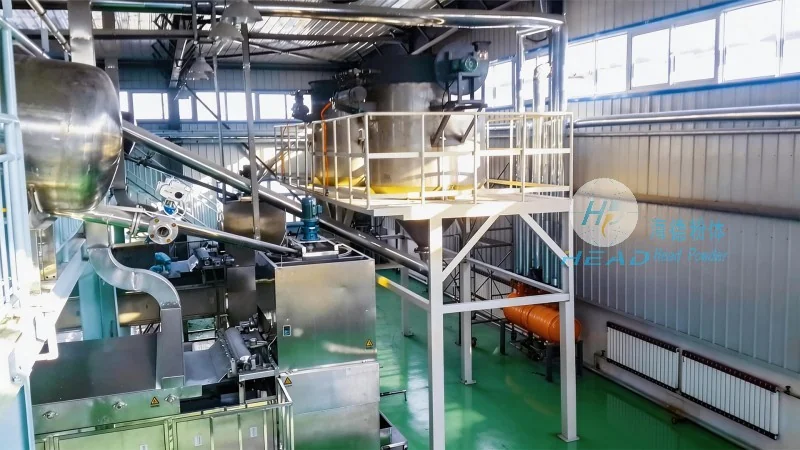
A recent project in Shandong, China, exemplifies HeadPowder’s capabilities in optimizing lignite transportation. The client, a large lignite mine, required a system to transport raw lignite from the mine to a nearby power plant over a distance of 5 kilometers. HeadPowder designed a dilute-phase pneumatic conveying system with a capacity of 200 tons per hour. The system was installed and commissioned within a short timeframe, with minimal disruption to the existing operations. Post-implementation, the client reported a 30% reduction in transportation costs compared to traditional methods, along with improved material quality due to reduced handling. The system’s reliability has also led to a decrease in maintenance downtime, contributing to higher overall plant efficiency. This case study highlights HeadPowder’s ability to deliver customized, efficient, and cost-effective solutions that meet the specific needs of lignite transportation projects.
As the demand for lignite continues to grow, the need for efficient and sustainable transportation methods becomes increasingly critical. Pneumatic conveying technology, when properly designed and optimized, offers a robust solution that addresses the unique challenges of lignite handling. Shandong HeadPowder Engineering Co., Ltd. stands out as a leader in this field, with a proven track record of delivering high-quality, customized systems that enhance operational efficiency and reduce environmental impact. By leveraging advanced engineering and a customer-centric approach, HeadPowder is positioned to meet the evolving needs of the energy industry, ensuring reliable and cost-effective lignite transportation for years to come.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top