Pharmaceutical bulk material pneumatic conveying is a critical process in the pharmaceutical industry, designed to transport powders and granules safely and efficiently. This method uses air or other gases to move materials through a system of pipes and equipment. Understanding the principles behind this technology is essential for optimizing operations in pharmaceutical manufacturing.
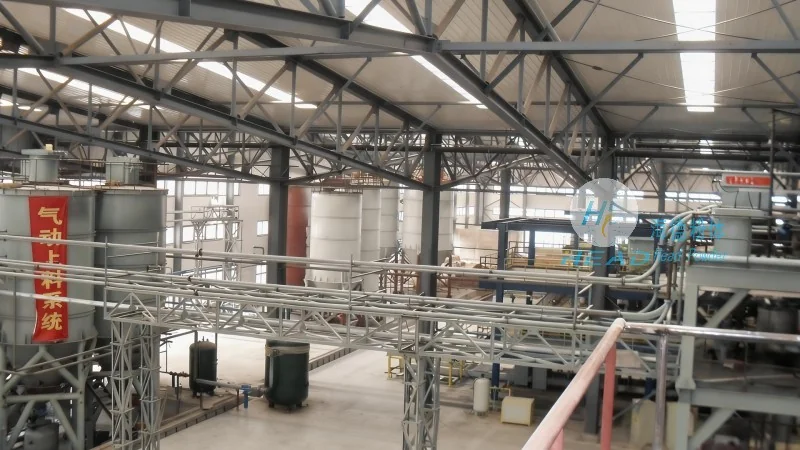
At its core, pneumatic conveying for pharmaceuticals involves the use of air pressure to transport bulk materials. The system typically consists of a hopper, a conveying line, and a receiver. The process begins when the material is fed into the hopper, where it is then drawn into the conveying line by the air flow. This method is particularly advantageous in pharmaceutical applications due to its ability to maintain product integrity, prevent contamination, and ensure a clean transfer process.
The design of a pharmaceutical bulk material pneumatic conveying system must adhere to strict standards to ensure compliance with regulatory requirements. Key principles include maintaining a closed system to prevent contamination, using materials that are compatible with pharmaceutical products, and ensuring the system can handle a wide range of particle sizes and densities. The system must also be designed for easy cleaning and maintenance to meet cGMP (current Good Manufacturing Practice) guidelines.
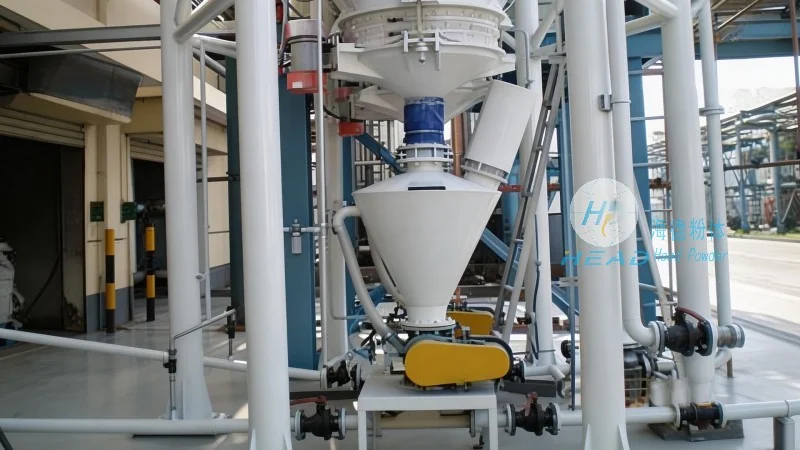
A typical pneumatic conveying system for pharmaceuticals includes several key components. The hopper is used to store and feed the material, while the conveying line transports it to the receiver. The air system, which may include blowers or compressors, provides the necessary pressure to move the material. The receiver is where the material is deposited. Each component must be carefully selected and designed to ensure the system operates efficiently and safely. For example, the use of stainless steel in components is common to prevent corrosion and maintain product purity.
Implementing pneumatic conveying in pharmaceutical manufacturing offers several benefits. It allows for a continuous and automated process, reducing the risk of human error and improving consistency. The closed system design minimizes the risk of cross-contamination, which is critical in pharmaceutical production. Additionally, pneumatic conveying can handle a variety of materials, from fine powders to larger granules, making it versatile for different production needs. The technology also helps in reducing material waste and improving overall production efficiency.
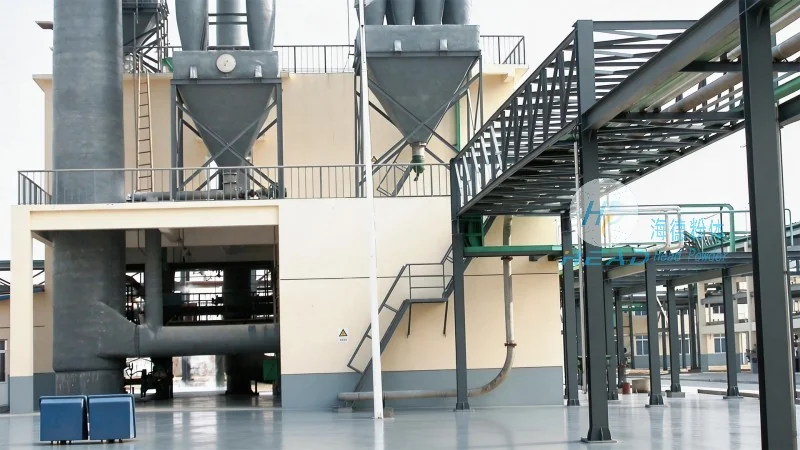
When designing a pneumatic conveying system for pharmaceutical applications, several factors must be considered. The type of material being conveyed is a primary consideration, as different materials have different flow characteristics and may require different conveying methods. The system must also be designed to handle the specific particle size distribution of the material. Additionally, the system must be integrated with other equipment in the manufacturing line to ensure smooth operation. The choice of air pressure and flow rate is also critical, as it directly impacts the system's efficiency and the risk of material degradation.
Pharmaceutical bulk material pneumatic conveying is a sophisticated and essential technology in modern pharmaceutical manufacturing. By adhering to strict design principles and using appropriate components, this system ensures the safe and efficient transfer of materials while maintaining product quality and regulatory compliance. Companies like Shandong HeadPowder Engineering Co., Ltd. specialize in designing and implementing such systems, providing pharmaceutical manufacturers with reliable solutions to meet their production needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top