Calcined sand, a critical material in various industrial applications, requires efficient and reliable transportation methods to ensure smooth operational processes. The calcined sand conveying system plays a pivotal role in managing the movement of this material from production sites to processing units. This article provides an overview of such systems, focusing on the benefits and characteristics of pneumatic conveying for calcined sand.
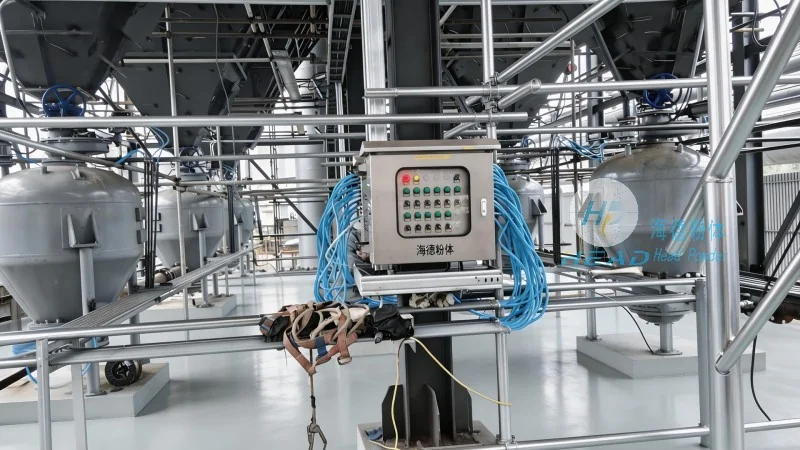
Calcined sand conveying systems are engineered to handle the unique properties of calcined sand, which often involves high temperatures, abrasive characteristics, and varying particle sizes. These systems are designed to ensure safe, efficient, and consistent material transport. The primary components of a typical calcined sand conveying system include the sand storage silo, conveyor lines, and control systems. The storage silo stores the calcined sand, while the conveyor lines transport it to the processing equipment. Control systems manage the flow rate and pressure to maintain optimal operation.
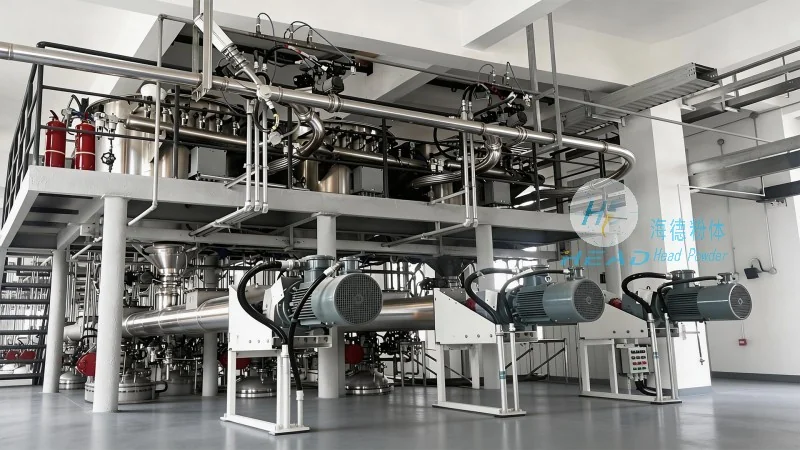
Pneumatic conveying, also known as air conveying, offers several advantages over traditional mechanical conveying methods for calcined sand. One of the key benefits is the ability to transport calcined sand over long distances without the need for intermediate transfer points. This reduces the risk of material degradation and contamination. Additionally, pneumatic conveying systems can handle abrasive materials like calcined sand without causing excessive wear on components, as the material is carried by air rather than mechanical contact. The system also allows for gentle handling of the sand, preserving its quality and preventing particle breakage.
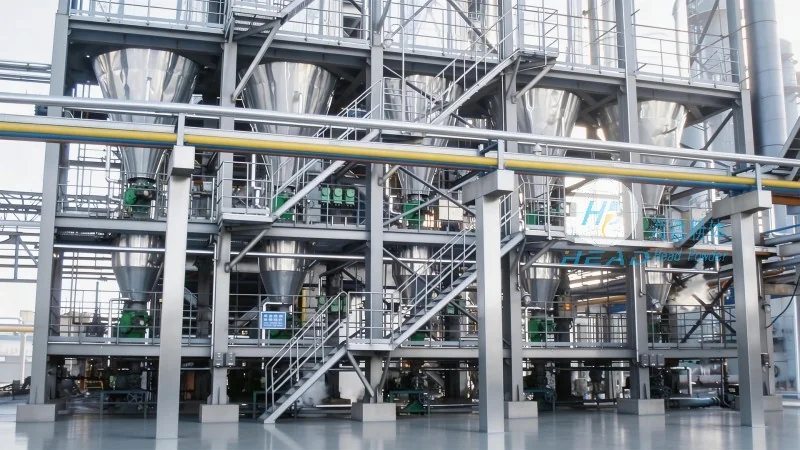
Modern pneumatic conveying systems for calcined sand are equipped with advanced features that enhance performance and reliability. These systems typically use positive pressure or negative pressure to move the material. Positive pressure systems blow air into the conveyor line, pushing the sand forward, while negative pressure systems create a vacuum to draw the material. The choice between these methods depends on the application requirements, such as the distance and the type of material being conveyed. Another important feature is the use of flexible hoses or rigid pipes, which can be adapted to the layout of the facility. This flexibility allows for easy installation and modification of the conveying system.
The use of calcined sand conveying systems is widespread across various industries, including foundries, refractory manufacturing, and construction materials production. In foundries, calcined sand is used as a refractory material in molds and cores, and efficient conveying ensures consistent quality in the final products. In refractory manufacturing, the precise handling of calcined sand is crucial for producing high-quality refractory bricks and other products. The construction industry also benefits from the use of calcined sand in concrete and other building materials, where the consistent supply of this material is essential for meeting production demands.
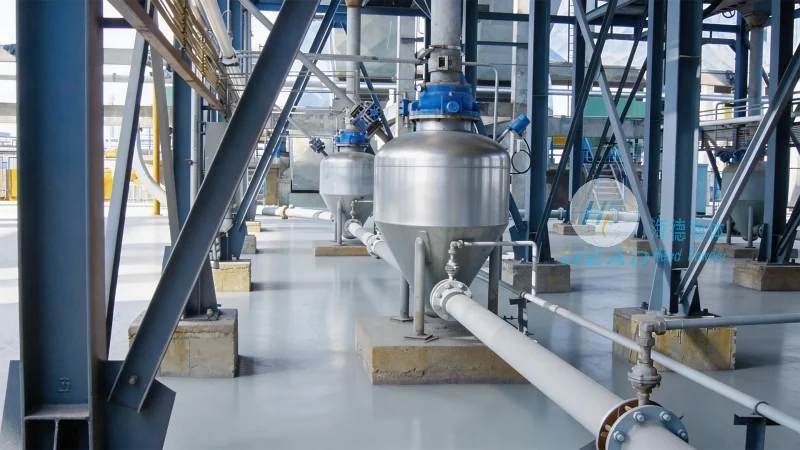
Efficient calcined sand conveying systems, particularly those utilizing pneumatic conveying, are essential for optimizing industrial processes. The advantages of such systems, including long-distance transport, gentle handling, and reduced wear, make them a preferred choice for many industries. For businesses seeking reliable solutions for calcined sand transportation, Shandong HeadPowder Engineering Co., Ltd. offers expert engineering and manufacturing services. Based in Shandong, China, the company specializes in providing customized conveying systems tailored to the specific needs of its clients. With a focus on quality and performance, HeadPowder ensures that its systems meet the highest industry standards, delivering reliable and efficient calcined sand conveying solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top