Dust-free material feeding and conveying equipment are specialized systems engineered to transport bulk materials while maintaining a contamination-free environment. These systems are critical in industries where product purity and operational cleanliness are paramount, such as pharmaceuticals, electronics, and food processing. Understanding their functionality and design principles is essential for businesses seeking to optimize material handling processes while adhering to stringent quality standards.
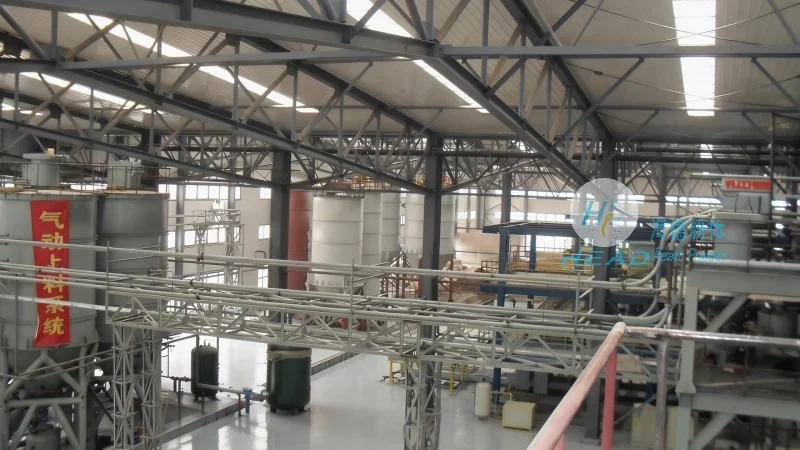
At the core of many industrial operations, the efficient and safe transfer of raw materials is a foundational requirement. Dust-free material feeding and conveying equipment, often referred to as dust-free feeders or conveying systems, are engineered to handle powders, granules, and other particulate materials without generating or allowing dust to escape into the surrounding environment. This is achieved through a combination of sealed components, advanced filtration, and precise control mechanisms. The primary goal of these systems is to ensure that the materials being processed remain uncontaminated and that the workspace remains clean, thereby minimizing health risks and maintaining compliance with industry regulations.
In industries where product integrity is non-negotiable, the role of dust-free material handling systems cannot be overstated. These systems are designed to prevent cross-contamination, protect personnel from airborne particles, and preserve the quality of the end product. For example, in pharmaceutical manufacturing, even trace amounts of dust can compromise the efficacy and safety of medications. Similarly, in the electronics industry, dust particles can cause short circuits or damage sensitive components. By implementing dust-free feeding and conveying equipment, companies can enhance operational efficiency while upholding the highest standards of cleanliness and safety.
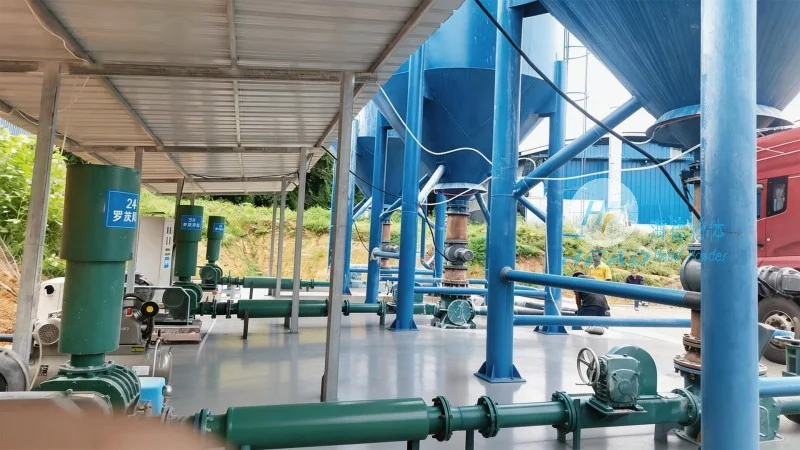
The design of dust-free material feeding and conveying equipment revolves around several key principles aimed at minimizing dust generation and ensuring material integrity. One of the most critical design aspects is the use of sealed and airtight components. This includes enclosed hoppers, sealed conveyor belts, and integrated dust collection systems. The materials used in the construction of these components are often chosen for their resistance to corrosion and their ability to withstand the mechanical stresses of material handling. Additionally, the design incorporates advanced filtration mechanisms, such as HEPA filters or cyclone separators, to capture any residual dust particles before they can escape into the environment. Precision control systems, including variable speed drives and pressure sensors, are also integral to maintaining consistent material flow and preventing blockages or overloading.
Dust-free material feeding and conveying equipment typically consists of several key components that work in concert to achieve optimal performance. The primary components include a hopper or feeder for material storage and discharge, a conveyor system (such as a screw, belt, or pneumatic conveyor) for material transport, and a dust collection system to capture and filter airborne particles. The hopper is often equipped with a discharge valve or gate to control the flow of material, while the conveyor system ensures smooth and continuous movement. The dust collection system, which may include filters, fans, and collection tanks, is designed to remove dust from the air and return it to the system or dispose of it safely. Other features may include sensors for level monitoring, alarms for system faults, and integration with automation systems for enhanced control and efficiency.
The applications of dust-free material feeding and conveying equipment span a wide range of industries, each with unique requirements for material handling and cleanliness. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients while preventing contamination. In the electronics industry, they are employed to handle sensitive components and prevent dust from damaging circuit boards. The food and beverage industry also relies on dust-free systems to maintain the purity of ingredients and prevent cross-contamination between different products. Additionally, in the chemical and plastics industries, these systems help manage powders and granules safely, reducing the risk of dust explosions and ensuring worker safety. The versatility of dust-free material handling systems makes them indispensable in any environment where product quality and operational safety are top priorities.
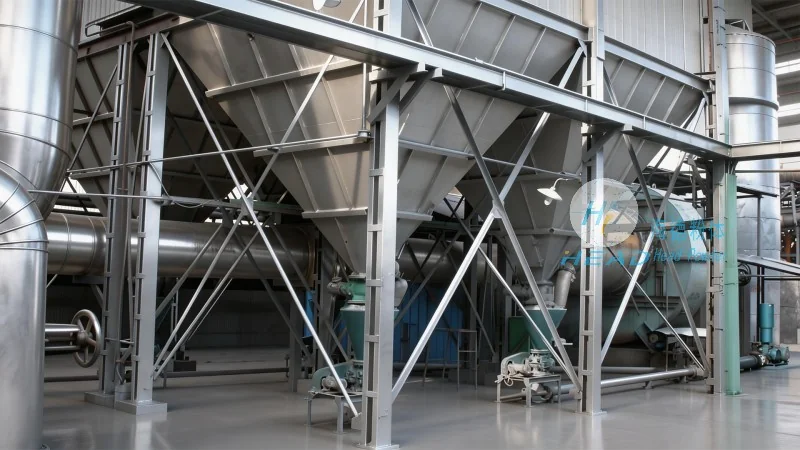
Maintaining a clean environment in material handling operations is not merely a regulatory requirement but a strategic advantage. Dust-free systems contribute to improved product quality, reduced downtime due to equipment maintenance, and enhanced worker safety. By preventing dust accumulation, these systems reduce the risk of equipment failure, which can lead to costly production interruptions. Furthermore, a clean workspace promotes better health and well-being for employees, reducing the incidence of respiratory issues and other health problems associated with exposure to airborne particles. In today's competitive market, companies that invest in advanced dust-free material handling systems are better positioned to meet customer demands for high-quality products and maintain a reputation for operational excellence.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of dust-free material feeding and conveying equipment. With a focus on innovation and quality, HeadPowder specializes in designing and producing systems tailored to the unique needs of various industries. The company's headquarters is located in Shandong, China, where it leverages advanced technology and engineering expertise to develop cutting-edge solutions for material handling challenges. HeadPowder's commitment to customer satisfaction and product excellence has made it a trusted partner for businesses seeking reliable and efficient dust-free material handling systems. Through continuous research and development, the company strives to deliver equipment that not only meets but exceeds industry standards, ensuring that clients can operate with confidence and achieve their operational goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top