Calcium carbonate, a widely used industrial material, often requires efficient and reliable transportation methods for processing and distribution. The calcium carbonate pneumatic conveying system is a specialized solution designed to handle this material with precision and efficiency. This article explores the fundamental aspects of such systems, focusing on their design principles and operational benefits.
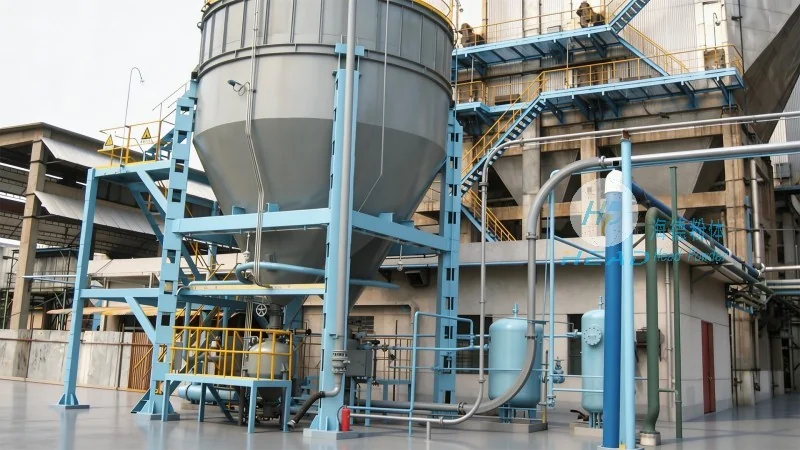
The calcium carbonate pneumatic conveying system is a technology that uses air or other gases to transport calcium carbonate particles from one location to another. This method is particularly advantageous for handling fine powders, as it minimizes material degradation and ensures a consistent flow. Unlike traditional mechanical conveyors, pneumatic systems can operate in a closed environment, reducing dust emissions and improving workplace safety. The system typically consists of a hopper for material storage, a conveyor line with a series of pipes, and a control unit to regulate air pressure and flow rates.
Several critical components work together to ensure the effective operation of a calcium carbonate pneumatic conveying system. The primary components include a material hopper, which holds the calcium carbonate powder and feeds it into the system. A rotary valve or feeder is used to control the flow of material into the conveyor line, ensuring a steady and controlled discharge. The conveyor line itself is made of durable materials, such as stainless steel or plastic, to withstand the abrasive nature of calcium carbonate particles. Air or gas is supplied by a blower or compressor, creating the necessary pressure to move the material through the pipes. The system may also include filters and cyclones to separate the material from the air, preventing dust buildup and maintaining air quality. Additionally, a control panel allows operators to adjust the system's parameters, such as air pressure and flow rate, to optimize performance and prevent system overload.
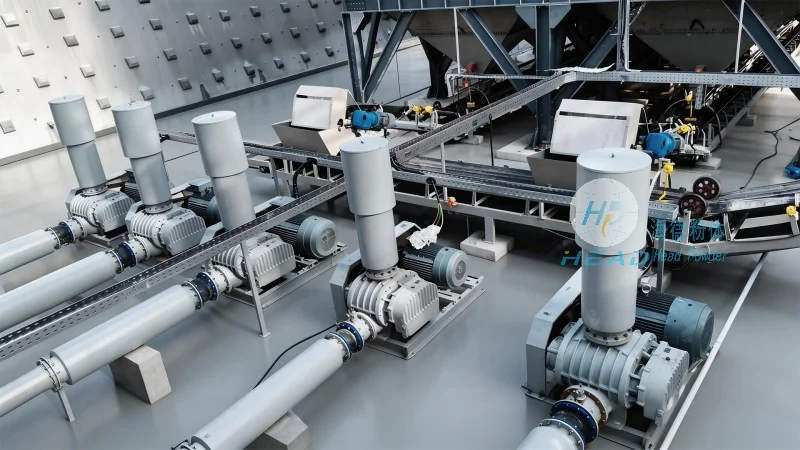
The design of a calcium carbonate pneumatic conveying system is based on several key principles to ensure optimal performance and reliability. One of the most important principles is maintaining a consistent air-to-material ratio. This ratio determines the velocity of the material through the pipes and is crucial for preventing blockages and ensuring smooth transport. The system's design must also consider the particle size and density of the calcium carbonate, as these factors affect the required air pressure and flow rates. For example, finer particles may require higher air velocities to maintain a stable flow, while larger particles may need lower velocities to avoid abrasion and wear on the system components. Another critical design principle is the layout of the conveyor line, which should be as straight and horizontal as possible to minimize pressure losses and reduce the risk of material deposition. The system may include bends or vertical sections, but these should be designed with appropriate angles and diameters to maintain the material's flow and prevent clogging. Furthermore, the system's components must be selected based on the material's properties, such as its abrasiveness and moisture content, to ensure long-term durability and minimal maintenance.
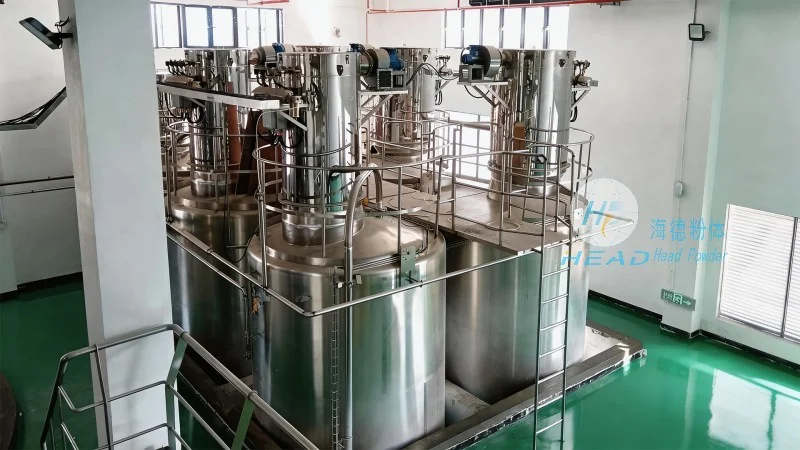
The calcium carbonate pneumatic conveying system offers several operational benefits that make it an attractive choice for industrial applications. One of the main advantages is its ability to handle fine powders without causing material degradation, which is essential for maintaining the quality of calcium carbonate products. The closed system design also reduces dust emissions, improving workplace safety and compliance with environmental regulations. Additionally, the system can operate in a continuous or batch mode, providing flexibility for different production needs. The system's efficiency in material transport reduces labor costs and increases production throughput, making it a cost-effective solution for many industries. The applications of this system are widespread, including the chemical, food, and pharmaceutical industries, where calcium carbonate is used as a filler, extender, or functional ingredient. For example, in the chemical industry, the system is used to transport calcium carbonate for use in the production of plastics, paints, and coatings. In the food industry, it is used to handle calcium carbonate as a food additive or nutritional supplement. The versatility of the system makes it suitable for a wide range of applications, from small-scale laboratory use to large-scale industrial production.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions, specializes in designing and manufacturing calcium carbonate pneumatic conveying systems. With years of experience in the industry, the company has developed a reputation for quality, reliability, and customer satisfaction. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. HeadPowder Engineering focuses on providing customized solutions tailored to the specific needs of its clients, ensuring that each system is optimized for performance and efficiency. The company's team of engineers and technicians work closely with clients to understand their requirements and develop solutions that meet their operational goals. HeadPowder Engineering also provides comprehensive after-sales support, including maintenance, repair, and technical assistance, to ensure the long-term performance of its systems. The company's commitment to quality and innovation has made it a trusted partner for many businesses in the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top