Efficient coal particle conveying is a critical aspect of industrial operations, particularly in sectors like power generation, mining, and material handling. The process of transporting coal from storage to processing or combustion sites requires reliable and efficient systems to ensure smooth workflow and minimal downtime. Various methods have been developed to address the unique challenges of coal handling, each offering distinct advantages based on operational needs, material characteristics, and environmental considerations.
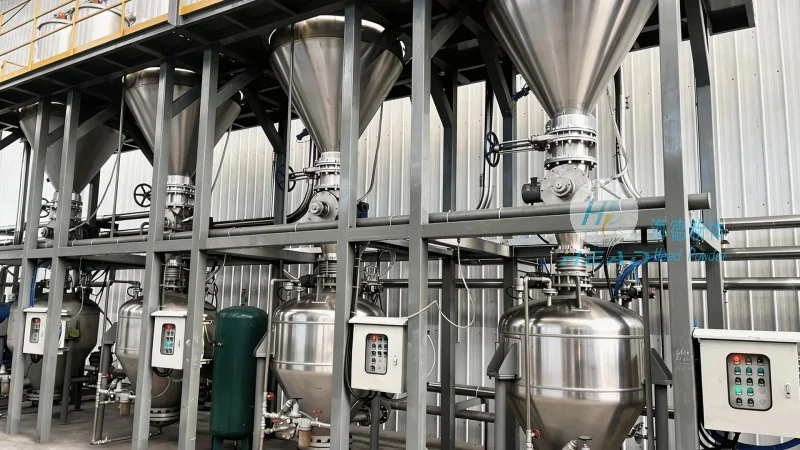
There are several established methods for coal particle conveying, each tailored to specific applications and operational requirements. The primary methods include belt conveyors, screw conveyors, pneumatic conveyors, and bucket elevators. Each system has its own set of advantages and limitations, making the selection process crucial for optimizing performance and cost-effectiveness.
Belt conveyors are among the most common and versatile systems used for coal particle conveying. These systems utilize a continuous belt that moves coal from one point to another, typically through a series of rollers and pulleys. The design allows for long-distance transport with minimal maintenance, making them suitable for both indoor and outdoor applications. Belt conveyors can handle a wide range of coal sizes and moisture levels, ensuring consistent performance even under heavy loads. The efficiency of belt conveyors lies in their ability to transport large volumes of material at relatively low operating costs, which is why they are widely adopted in industrial settings.
Screw conveyors, also known as auger conveyors, offer a compact and enclosed solution for coal particle transport. These systems consist of a rotating screw within a tube, which pushes coal forward as it rotates. Screw conveyors are ideal for applications where space is limited or where dust control is a priority. They are particularly effective for handling fine coal particles and can be used in both horizontal and vertical orientations. The enclosed design of screw conveyors helps minimize dust emissions and prevents material spillage, making them a preferred choice in environments where air quality is a concern. However, screw conveyors may have limitations in terms of the maximum particle size and the amount of material they can transport compared to other systems.
Pneumatic conveyors use air pressure to transport coal particles through a pipeline system. This method is particularly useful for applications requiring dust-free transport or when the coal needs to be moved over long distances without the need for multiple transfer points. Pneumatic systems can handle both dry and wet coal, and they are capable of transporting materials at high speeds, reducing overall transit time. The flexibility of pneumatic conveying allows for the integration of multiple transfer points and the ability to route the material to different destinations from a single source. However, pneumatic systems may require higher energy input and can be more complex to maintain compared to other conveyor types.
Bucket elevators are specialized systems designed for vertical coal transport, often used in combination with horizontal conveyors to form a complete material handling system. These elevators consist of a series of buckets attached to a chain or belt, which moves vertically to lift coal from a lower level to a higher one. Bucket elevators are highly efficient for vertical transport and can handle large volumes of material with minimal space requirements. They are commonly used in power plants and mining operations where vertical movement is necessary to elevate coal to processing or combustion areas. The enclosed design of bucket elevators helps prevent dust and spillage, ensuring a clean and safe operation. However, bucket elevators may have higher initial costs and require more maintenance than other conveyor types, especially when dealing with abrasive coal particles.
The selection of the most appropriate coal particle conveying method depends on several factors, including the type and size of coal, the distance to be covered, the required capacity, and the environmental regulations in place. For example, belt conveyors are often preferred for long-distance horizontal transport due to their high capacity and low cost. Screw conveyors are ideal for applications requiring dust control and compact design, such as in processing plants. Pneumatic conveyors excel in environments where dust-free transport is essential, like in food processing or pharmaceutical industries. Bucket elevators are best suited for vertical transport needs, particularly in power generation facilities where coal must be elevated to boilers.
In conclusion, the choice of coal particle conveying method is a critical decision that impacts the efficiency, cost, and safety of industrial operations. Each method, including belt conveyors, screw conveyors, pneumatic conveyors, and bucket elevators, offers unique advantages and is suitable for specific applications. By carefully evaluating the operational requirements and material characteristics, industrial facilities can select the most effective conveying system to ensure smooth and reliable coal transport. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd. can be invaluable in designing and implementing these systems, ensuring optimal performance and compliance with industry standards. With a focus on providing tailored solutions for coal handling, Shandong HeadPowder Engineering Co., Ltd. leverages advanced technology and engineering expertise to deliver reliable and efficient conveying systems that meet the diverse needs of industrial clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top