For industrial operations dealing with bulk materials like bentonite, efficient and reliable material handling is crucial. This article explores the concept of a bentonite pneumatic conveying system, its design principles, and the engineering considerations that ensure optimal performance. The information is presented by Shandong HeadPowder Engineering Co., Ltd., a company based in Shandong, China, specializing in advanced material handling solutions.
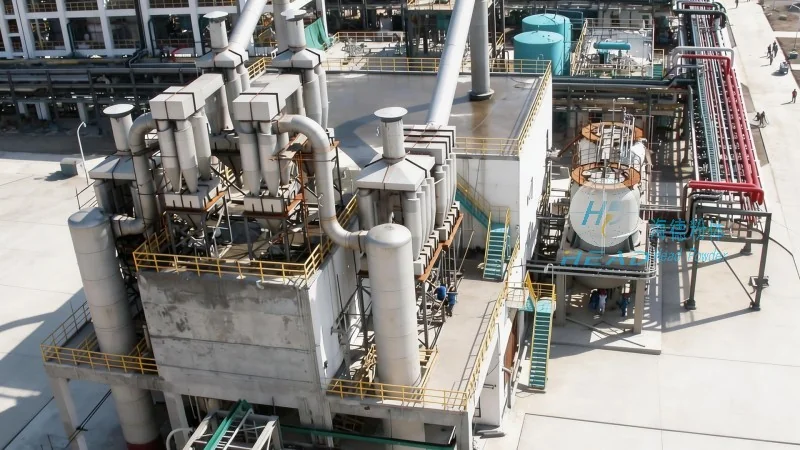
A bentonite pneumatic conveying system is a type of material handling equipment that uses compressed air or other gases to transport bulk materials, such as bentonite, through a network of pipes. Unlike traditional mechanical conveyors, this system relies on the kinetic energy of the air to move the material, making it particularly suitable for handling fine powders and granules. The system typically consists of a hopper for material storage, a blower or compressor to generate the air flow, a pipeline system to transport the material, and a collection or discharge unit. The primary goal is to move bentonite from its source to a processing or storage location with minimal loss and maximum efficiency.
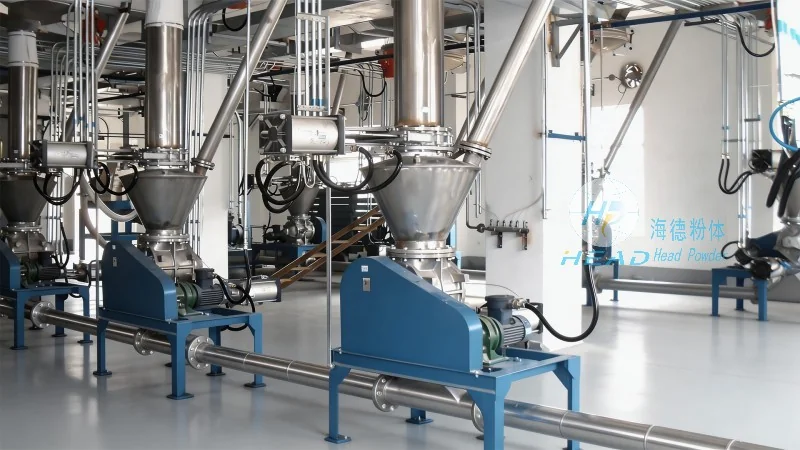
The effectiveness of a bentonite pneumatic conveying system depends on several critical components, each playing a specific role in the material transport process. The first component is the material hopper, which stores the bentonite and provides a consistent feed to the system. The hopper is designed with a discharge valve to control the flow rate, preventing overloading or underfeeding. Next, the air source, usually a high-pressure blower or compressor, generates the necessary airflow to move the material. The blower's capacity and pressure are critical, as they determine the system's conveying capacity and distance. The pipeline system, made of materials like stainless steel or plastic, is the conduit for both the material and air. It is designed to handle the pressure and flow requirements while minimizing friction losses. The conveying line may include bends, elbows, and expansion joints to accommodate changes in direction and elevation. At the receiving end, a separator or cyclone is used to separate the bentonite from the air stream. This component uses centrifugal force to separate the particles from the gas, allowing the clean air to be recirculated or vented. Finally, the control system manages the entire operation, monitoring pressure, flow rate, and material level to ensure smooth and safe operation.
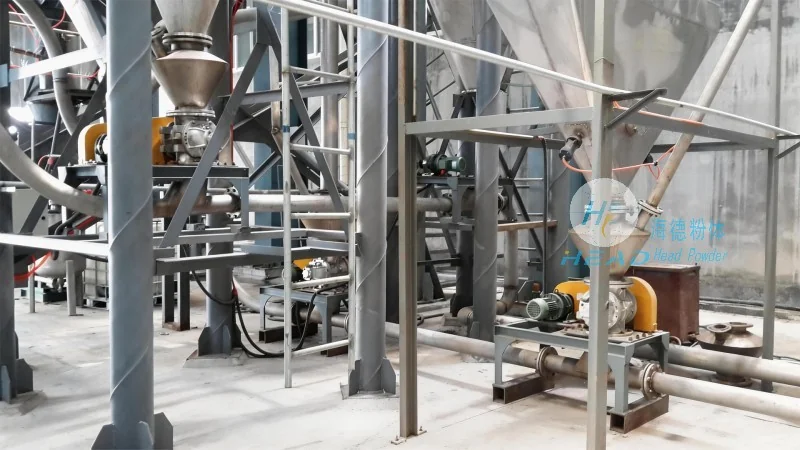
The design of a bentonite pneumatic conveying system follows several fundamental principles to ensure optimal performance and reliability. The first principle is the selection of the appropriate conveying method, which depends on the material's properties, such as particle size, density, and moisture content. For fine bentonite powders, a dilute-phase system is often preferred, where the material is suspended in the air stream at a low concentration. This method is efficient for long-distance transport but requires higher air volumes. For larger particles or bulkier materials, a dense-phase system may be used, where the material is conveyed in a more concentrated form, reducing the risk of blockages and increasing system efficiency. Another key principle is the calculation of the required air velocity and pressure. Engineers use fluid dynamics equations to determine the necessary air flow rate and pressure to maintain the material in suspension and prevent settling or clogging. The system's design also considers the material's flow properties, including its angle of repose and compressibility, to ensure smooth feeding and prevent arching or bridging in the hopper. Additionally, safety and environmental considerations are integral to the design. The system must comply with local regulations regarding air emissions and noise levels. Proper filtration and dust collection systems are installed to minimize air pollution and protect the environment. The control system includes safety features like pressure relief valves and emergency shut-off switches to prevent accidents and protect personnel.
Bentonite pneumatic conveying systems are widely used in various industrial applications due to their versatility and efficiency. In the chemical industry, they are used to transport bentonite for the production of drilling mud, paper, and other products. The system's ability to handle fine powders ensures consistent quality in the final product. In the mining and mineral processing sector, bentonite is used as a flocculant and binder, and the pneumatic conveying system efficiently transports it to processing plants. The system's benefits extend beyond just material transport. It offers advantages such as reduced labor costs, minimized material loss, and improved safety compared to traditional methods like truck or conveyor belt transport. The system is also more flexible, as it can be easily reconfigured to accommodate changes in production needs or facility layout. Furthermore, the use of compressed air as the conveying medium eliminates the need for mechanical parts that are prone to wear and tear, reducing maintenance costs and increasing the system's lifespan. The environmental benefits are also significant, as the system reduces dust emissions and the need for water in some applications, making it a more sustainable option for bulk material handling.
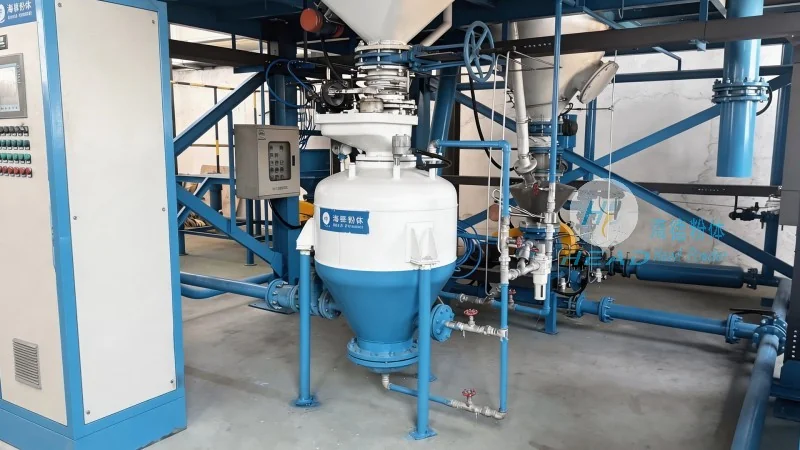
In conclusion, a bentonite pneumatic conveying system is a sophisticated and efficient solution for handling bulk materials like bentonite. Its design, based on fluid dynamics and engineering principles, ensures reliable and safe material transport. The system's components work in harmony to move the material from its source to the desired location, minimizing losses and maximizing productivity. As a leading provider of material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing these systems tailored to the specific needs of industrial clients. With a focus on quality, innovation, and customer satisfaction, the company ensures that its systems meet the highest standards of performance and reliability. Whether for chemical processing, mining, or other industrial applications, a bentonite pneumatic conveying system offers a cost-effective and sustainable solution for bulk material handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top