Ammonium nitrate, a widely used chemical in agricultural and industrial sectors, requires specialized handling systems for safe and efficient transport. Pneumatic conveying systems are a common method for moving this material, and understanding the key components that constitute such a system is essential for optimizing performance and maintaining safety standards. This article explores the primary elements of an ammonium nitrate pneumatic conveying setup, detailing each component's role and significance in the overall operation.
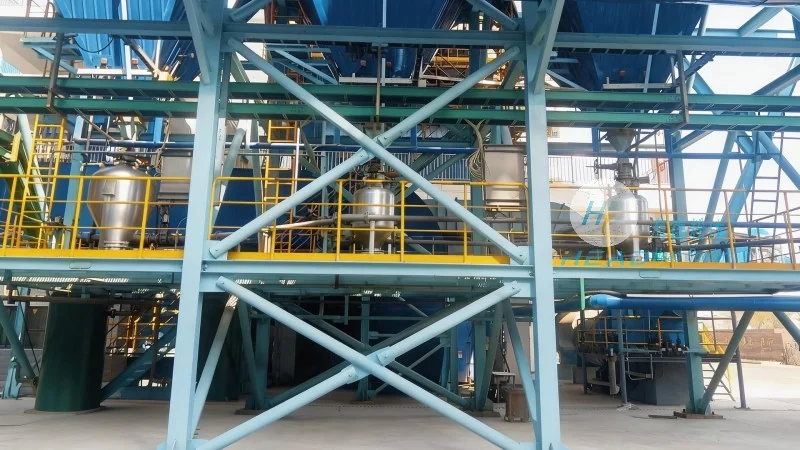
An ammonium nitrate pneumatic conveying system is a complex assembly of equipment designed to handle the material's granular nature and potential sensitivity to moisture or pressure changes. The primary components include the material storage and feeding unit, the conveying pipe network, the air supply system, the material separation equipment, and the control and monitoring systems. Each of these components plays a vital role in ensuring the system operates effectively and safely.
The material hopper serves as the initial storage vessel for ammonium nitrate, typically constructed from corrosion-resistant materials like stainless steel to withstand the chemical's properties and prevent degradation over time. The hopper design features a conical bottom and a discharge outlet that allows for controlled material flow. The feeder, often a rotary valve or a screw feeder, regulates the amount of ammonium nitrate released into the conveying line. This component is critical for maintaining a consistent flow rate, preventing material buildup in the hopper, and ensuring smooth operation of the entire system. Properly designed feeders help minimize the risk of blockages and ensure that the material is introduced into the pipe at an optimal velocity.
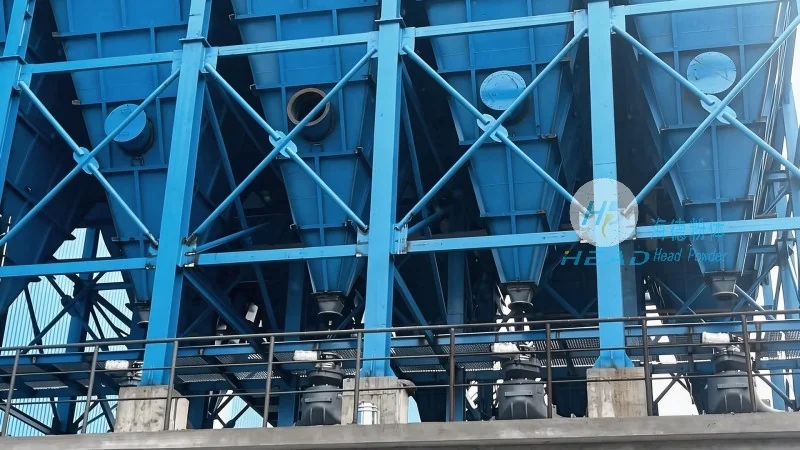
The conveying pipe network is the main pathway for transporting ammonium nitrate from the source to the destination. This network consists of a series of pipes, including vertical risers, horizontal runs, and bends, all made from materials like stainless steel or polyethylene to resist corrosion and maintain durability. The pipe diameter and length are carefully selected based on the system's capacity, the material's density, and the required conveying distance. The design of the pipe network aims to minimize pressure drop, which is essential for efficient material movement and reducing energy consumption. Properly sized and laid-out pipes ensure that the ammonium nitrate flows smoothly without excessive turbulence or segregation, which could lead to system inefficiencies or material loss.
The air supply system provides the necessary airflow to create the pneumatic conveying effect. The blower unit, which can be a positive displacement blower or a centrifugal fan, generates the pressure and volume of air required to move the material through the pipes. The choice of blower depends on factors such as the system's throughput, the material's specific gravity, and the distance the material needs to travel. The air supply system also includes air filtration and moisture control components to ensure that the air used is clean and dry. Moisture in the air can affect the material's flow characteristics and potentially cause blockages or corrosion in the system. By maintaining dry and clean air, the system operates more reliably and reduces maintenance needs.
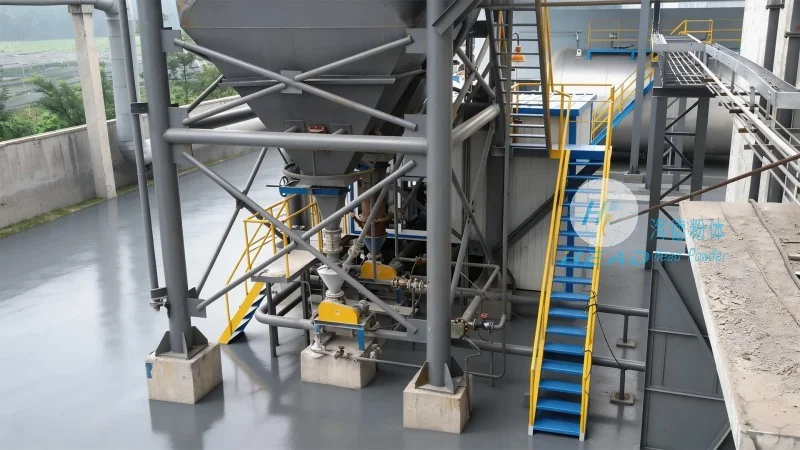
At the receiving end of the conveying system, the material separation and collection equipment are responsible for discharging the ammonium nitrate and separating it from the air. This typically involves a cyclone separator or a baghouse filter, which captures the material and returns it to a collection bin or storage silo. The separation process is critical for maintaining system efficiency and preventing material loss or contamination. The cyclone separator uses centrifugal force to separate the material from the air, while the baghouse filter employs fabric bags to trap fine particles. Both systems are designed to handle the specific characteristics of ammonium nitrate, ensuring that the material is collected in a controlled manner and that dust emissions are minimized. Properly maintained separation equipment is essential for compliance with environmental regulations and for maintaining the quality of the conveyed material.
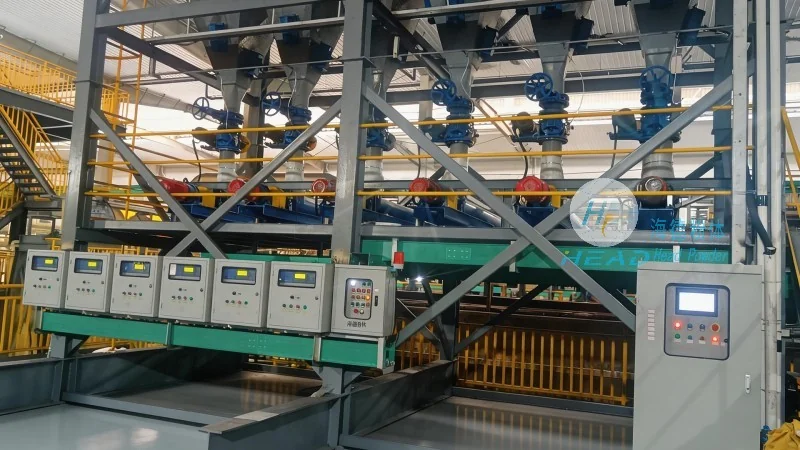
Modern ammonium nitrate pneumatic conveying systems incorporate advanced control and monitoring technologies to optimize performance and enhance safety. These systems include sensors and indicators for pressure, flow rate, and material level, providing real-time data on system operation. Control panels allow operators to adjust parameters such as air pressure, feeder speed, and conveying speed, ensuring the system operates within safe and efficient parameters. Additionally, safety interlocks and alarms are integrated to detect and respond to potential issues, such as overpressure, material blockages, or abnormal flow rates. These features help prevent accidents and downtime, ensuring the system operates reliably and consistently. The control systems also enable remote monitoring and diagnostics, allowing for proactive maintenance and reducing the need for on-site inspections.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a prominent manufacturer and supplier of pneumatic conveying systems, including those tailored for ammonium nitrate applications. HeadPowder has built a strong reputation in the chemical processing industry by providing high-quality, reliable equipment that meets the stringent requirements of its clients. The company is headquartered in Shandong, China, and serves a global clientele with customized solutions designed to address specific operational needs. HeadPowder's expertise in material handling and pneumatic conveying technology ensures that their systems are engineered to handle the unique challenges associated with ammonium nitrate, such as its granular structure and potential sensitivity to environmental factors. The company's commitment to innovation, quality, and safety has made it a trusted partner for businesses seeking efficient and safe ammonium nitrate conveying solutions. With a focus on customer satisfaction and long-term partnerships, HeadPowder continues to be a key player in the industry, delivering systems that enhance operational efficiency and ensure compliance with industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top