Calcined sand, a crucial material in various industrial processes, requires efficient and reliable transportation methods to ensure smooth operation. Pneumatic conveying systems have emerged as a preferred solution for handling calcined sand due to their ability to transport materials in a dust-free environment, enhancing safety and product quality. This article provides a comprehensive classification and application analysis of calcined sand pneumatic conveying systems, highlighting the key factors that influence system selection and performance.
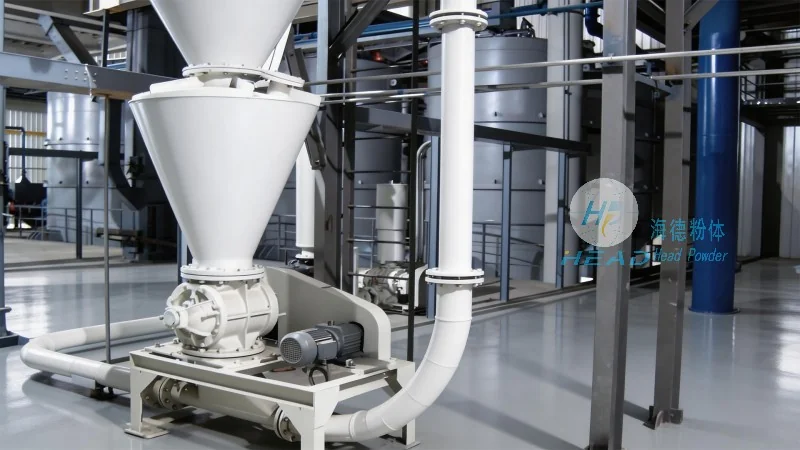
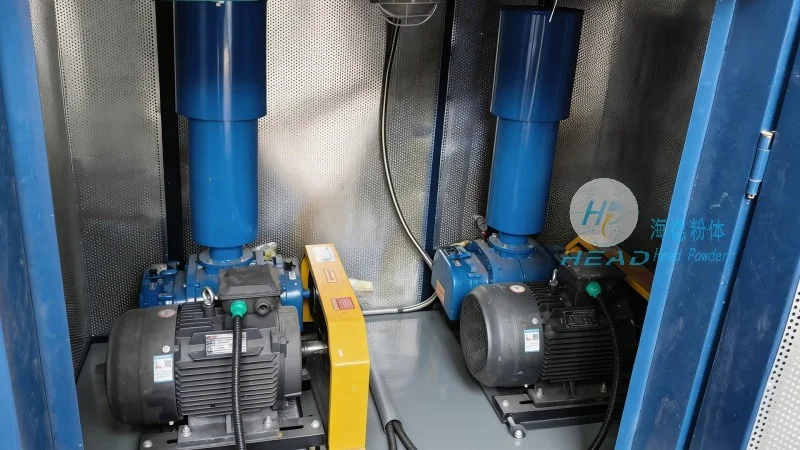
Shandong HeadPowder Engineering Co., Ltd., a reputable company based in China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. With years of experience in the industry, HeadPowder has established itself as a trusted partner for businesses seeking efficient material handling solutions. The company's expertise lies in understanding the unique requirements of calcined sand applications and tailoring systems that meet specific operational needs. HeadPowder's commitment to quality and innovation ensures that their systems deliver optimal performance and durability.
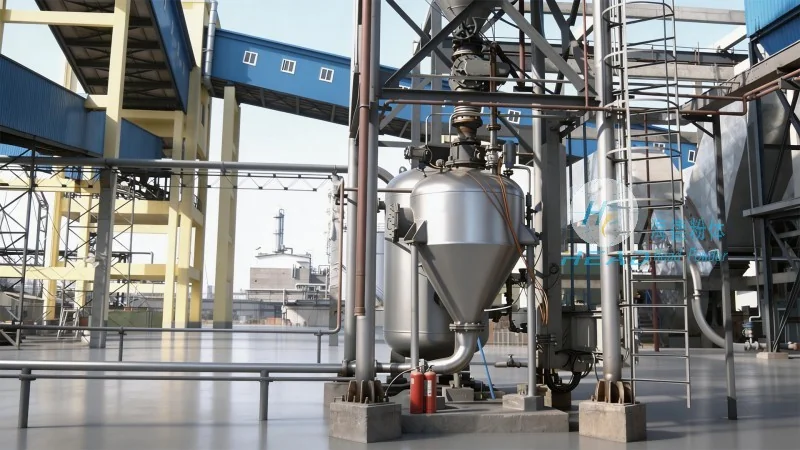
Calcined sand pneumatic conveying systems can be classified based on several key parameters, including the conveying principle, material flow rate, and system configuration. The primary classification includes positive pressure systems, negative pressure systems, and hybrid systems. Positive pressure systems, such as pressure vessels and blower-driven systems, are commonly used for high-volume conveying of calcined sand. These systems operate by pressurizing the conveying line with air, ensuring continuous material transport. Negative pressure systems, on the other hand, use vacuum to draw material from the source, making them suitable for applications where dust control is critical. Hybrid systems combine elements of both positive and negative pressure, offering flexibility in handling varying material characteristics and flow rates. The choice of system type depends on factors like the distance of material transport, the required flow rate, and the environmental regulations in the operating area.
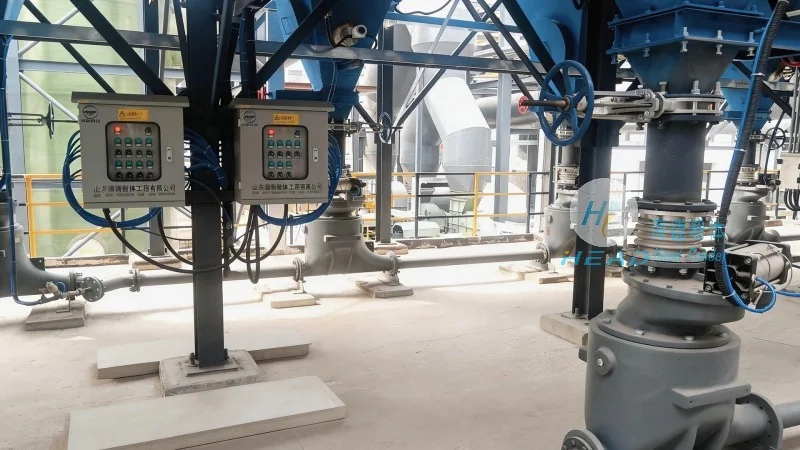
Effective calcined sand pneumatic conveying systems consist of several critical components that work in tandem to ensure efficient material transport. The main components include the material feed hopper, which stores and feeds the calcined sand into the system; the air compressor or vacuum pump, which provides the necessary pressure or vacuum; the conveying line, which transports the material; and the receiver or discharge hopper, where the material is collected. Additionally, systems may include filters and cyclones to separate air from the material, ensuring that the discharged product is clean and free from contaminants. The material feed hopper is designed to handle the bulk density and flow characteristics of calcined sand, preventing blockages and ensuring consistent material feed. The air compressor or vacuum pump is selected based on the required pressure or vacuum level and the flow rate of the system. The conveying line is typically made of materials like stainless steel or plastic, chosen for their resistance to corrosion and wear from calcined sand particles. The receiver or discharge hopper is equipped with a discharge valve or outlet to allow the material to be collected in a controlled manner. Filters and cyclones are essential for maintaining air quality and preventing dust emissions, which is crucial for compliance with environmental regulations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top