Phosphate fertilizer powder is a critical raw material in the agricultural industry, and its efficient transportation is essential for the smooth operation of production lines. Pneumatic conveying systems have become a popular choice for handling such powders due to their ability to transport materials over long distances without the need for complex mechanical equipment. This article provides a technical analysis of pneumatic conveying systems for phosphate fertilizer powders, focusing on the comparison between positive pressure and negative pressure conveying modes. The comparison will cover key aspects such as system design, operational efficiency, material handling characteristics, and application scenarios, helping users make informed decisions based on their specific requirements.
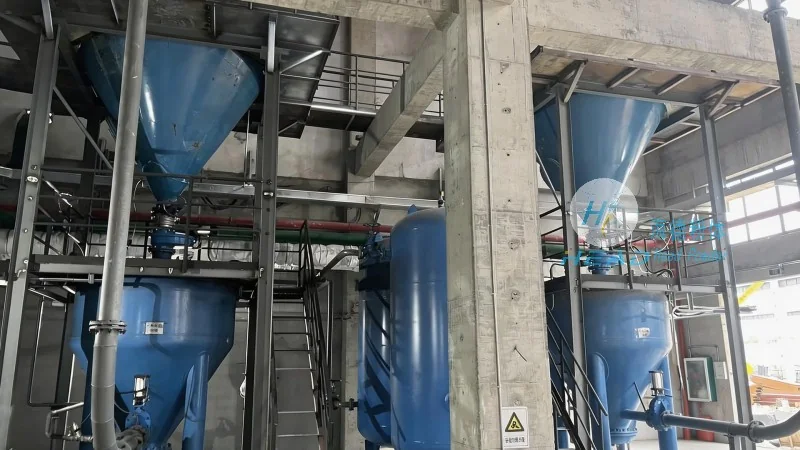
Pneumatic conveying systems are widely used in the fertilizer industry to transport phosphate powders from storage silos to processing units or packaging facilities. These systems utilize air or gas to move the material through a pipeline network, eliminating the need for traditional belt conveyors or bucket elevators. The choice between positive pressure and negative pressure systems depends on factors like the material's properties, distance to be conveyed, and the desired level of control over the conveying process. Both modes have their unique advantages and limitations, which will be explored in detail in this analysis.
Positive pressure conveying systems operate by blowing air or gas into the conveying line, creating a pressure higher than the ambient air pressure. This method is particularly effective for transporting powders with high moisture content or those that are prone to caking. The high pressure ensures that the material is fully suspended and moves smoothly through the pipeline, reducing the risk of blockages and material degradation. In the context of phosphate fertilizer powders, positive pressure systems are commonly used for short to medium-distance conveying, typically up to several hundred meters. They are also suitable for applications where the material needs to be delivered to multiple points along the line, as the system can be easily divided into branches.
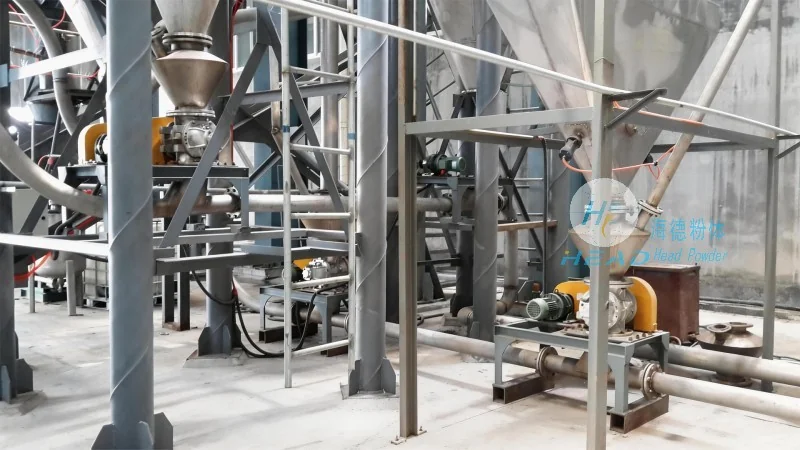
Negative pressure conveying systems, also known as vacuum systems, work by creating a vacuum in the conveying line, drawing the material from the source into the pipeline. This method is ideal for applications where the material is to be collected from multiple points or where the source is at a higher elevation than the destination. Negative pressure systems are particularly effective for handling powders that are light and dusty, as the vacuum helps to maintain a consistent flow rate and prevent dust emissions. For phosphate fertilizer powders, negative pressure systems are often used for longer distances, up to several kilometers, and are commonly employed in large-scale production facilities where the material needs to be transported from a central storage area to multiple processing units.
The design of a pneumatic conveying system for phosphate fertilizer powders involves several critical technical considerations that impact its performance and efficiency. One of the most important factors is the selection of the appropriate air velocity, which must be high enough to fully suspend the material but not so high as to cause excessive wear on the pipeline or increase energy consumption. The air velocity is typically determined based on the material's bulk density, particle size distribution, and flowability. Another key consideration is the choice of pipeline material, which must be resistant to corrosion and abrasion caused by the phosphate powder. Stainless steel or special alloy pipes are commonly used in these systems to ensure durability and longevity.
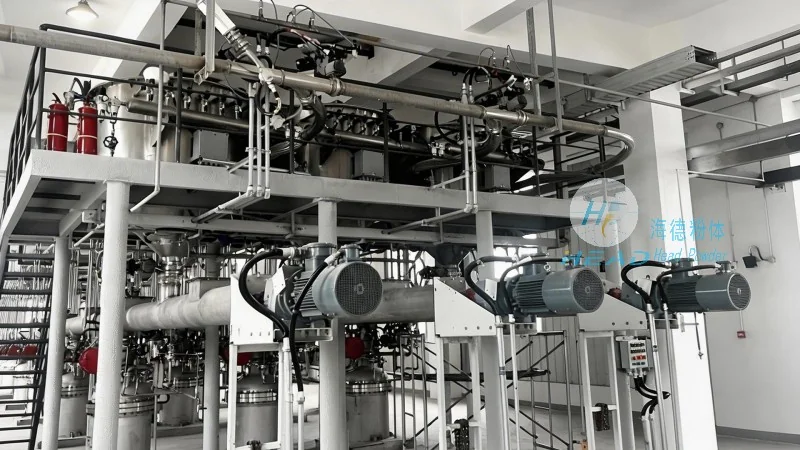
Operational efficiency and energy consumption are critical factors in the selection of a pneumatic conveying system. Positive pressure systems generally consume more energy than negative pressure systems due to the higher air pressure required to move the material. However, they offer better control over the conveying process and are more suitable for applications where the material needs to be delivered to multiple points. Negative pressure systems, on the other hand, are more energy-efficient for long-distance conveying but may require more maintenance due to the higher risk of dust accumulation and blockages. The choice between the two modes should be based on a careful analysis of the specific application requirements, including the distance to be conveyed, the material's properties, and the desired level of control.
The material handling characteristics of phosphate fertilizer powders, such as their bulk density, particle size, and flowability, play a significant role in the performance of the pneumatic conveying system. Positive pressure systems are better suited for materials with higher bulk density and larger particle sizes, as the high pressure ensures that the material is fully suspended and moves smoothly through the pipeline. Negative pressure systems are more effective for lighter, more dusty powders, as the vacuum helps to maintain a consistent flow rate and prevent dust emissions. Flow control is another important aspect, as it allows operators to adjust the conveying rate according to the production needs. This can be achieved through the use of control valves, pressure regulators, and flow meters, which are integrated into the system design.
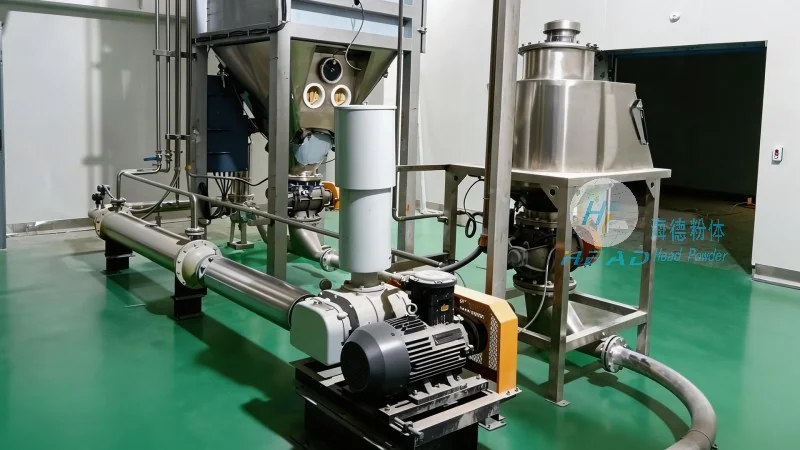
The choice between positive pressure and negative pressure conveying modes for phosphate fertilizer powders depends on the specific application scenario. For example, a small-scale fertilizer plant with a short conveying distance and a single destination point may find a positive pressure system more suitable due to its simplicity and lower cost. In contrast, a large-scale industrial facility with multiple processing units and long-distance conveying requirements may benefit from a negative pressure system due to its energy efficiency and ability to handle multiple points. Case studies from real-world applications have shown that positive pressure systems are more effective for handling powders with high moisture content or those that are prone to caking, while negative pressure systems are better suited for longer distances and lighter powders. These case studies provide valuable insights into the practical performance of each system and can help users make informed decisions based on their specific needs.
In conclusion, the choice between positive pressure and negative pressure pneumatic conveying systems for phosphate fertilizer powders depends on a careful analysis of the application requirements, including the distance to be conveyed, the material's properties, and the desired level of control. Positive pressure systems offer better control and are more suitable for short to medium-distance conveying, while negative pressure systems are more energy-efficient for long-distance conveying and are better suited for handling lighter, more dusty powders. The design of the system should also consider factors such as pipeline material, air velocity, and flow control to ensure optimal performance and efficiency. By understanding the technical aspects of each mode and their applications, users can select the most appropriate pneumatic conveying system for their phosphate fertilizer powder handling needs, ensuring smooth and efficient operation of their production lines.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top