Ammonium nitrate is a critical industrial chemical widely used in fertilizers, explosives, and other applications. Efficient and safe handling of this material is paramount for manufacturers to maintain productivity and ensure operational safety. Traditional methods of transporting ammonium nitrate, such as belt conveyors or bucket elevators, often face challenges like material degradation, dust generation, and high maintenance costs. To address these issues, many industries are turning to pneumatic conveying technology as a more efficient and clean alternative.
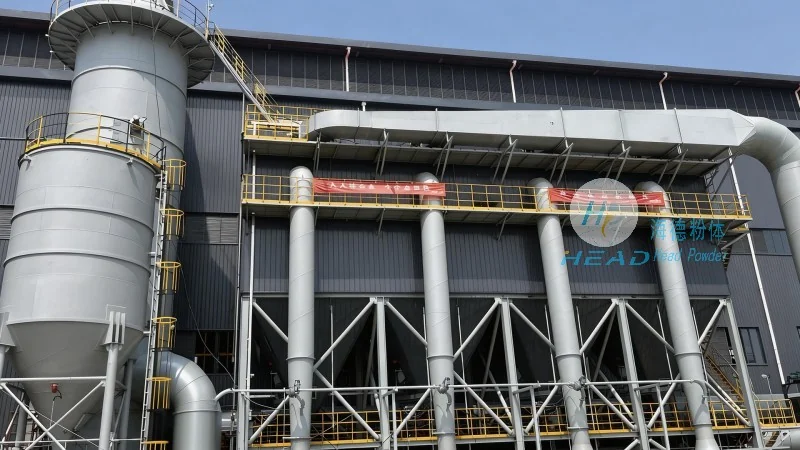
Shandong HeadPowder Engineering Co., Ltd., a prominent company based in China, specializes in designing and manufacturing advanced pneumatic conveying systems tailored for handling ammonium nitrate and other bulk materials. With years of experience in the field, HeadPowder has established itself as a trusted partner for businesses seeking to optimize their material handling processes. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-quality solutions that meet the unique needs of its clients.
Pneumatic conveying systems use air or other gases to transport bulk materials like ammonium nitrate through a pipeline network. This technology offers several advantages over conventional methods. First, it minimizes dust exposure, reducing health risks for workers and preventing contamination of the material. Second, it enables faster and more precise material transfer, improving overall production efficiency. Third, pneumatic conveying systems are less prone to material degradation, as the material is not subjected to mechanical stress or abrasion during transport. These benefits make pneumatic conveying an ideal choice for industries that require clean, reliable, and efficient handling of ammonium nitrate.
HeadPowder’s pneumatic conveying systems are engineered with a focus on performance, reliability, and safety. The systems typically consist of several components, including a material feed hopper, a conveying line, a receiver, and a control system. The feed hopper ensures a consistent flow of ammonium nitrate into the system, while the conveying line transports the material to the desired destination. The receiver collects the material and can be integrated with downstream processes. The control system monitors and regulates the operation of the system, ensuring optimal performance and preventing issues like blockages or overfilling.
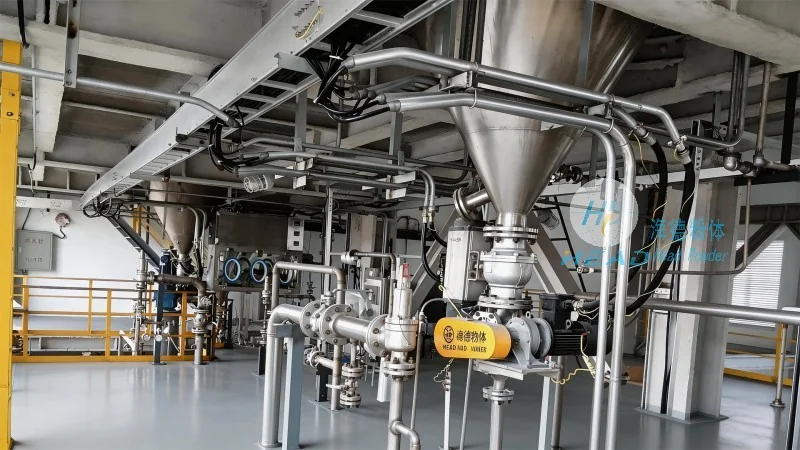
One of the key advantages of HeadPowder’s systems is their adaptability. The company offers both positive and negative pressure conveying options, allowing customers to choose the most suitable configuration based on their specific application requirements. Positive pressure systems are ideal for long-distance or high-rise applications, as they can maintain consistent material flow over greater distances. Negative pressure systems, on the other hand, are better suited for applications where dust control is a top priority, as they draw material into the system rather than expelling it.
Adopting pneumatic conveying technology for ammonium nitrate handling brings numerous benefits to industrial operations. For one, it significantly reduces labor costs associated with manual handling and cleaning. The automated nature of the system minimizes the need for human intervention, freeing up workers for other tasks and improving overall productivity. Additionally, the reduced dust generation leads to lower maintenance costs for equipment and a safer working environment. Over time, these operational efficiencies translate into substantial cost savings for businesses.
Another key benefit is the improved product quality. By minimizing material degradation and contamination, pneumatic conveying systems help maintain the purity and effectiveness of ammonium nitrate. This is particularly important for applications where the material is used in sensitive processes, such as fertilizer production or pharmaceutical manufacturing. The consistent flow and precise control of the system also reduce the risk of spills or overfilling, further enhancing product quality and safety.
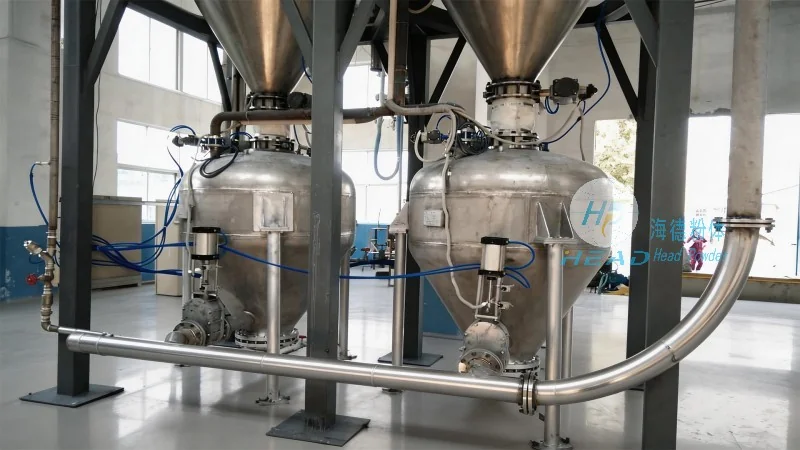
Consider a fertilizer manufacturing plant that was struggling with inefficient and dusty material handling processes. The plant was using traditional belt conveyors to transport ammonium nitrate from storage silos to production lines, resulting in frequent breakdowns, high maintenance costs, and poor air quality in the facility. After evaluating various options, the plant decided to implement a pneumatic conveying system from HeadPowder. The new system was installed and commissioned within a few weeks, and the results were immediate.
The plant experienced a 30% reduction in material handling time, as the pneumatic system transported ammonium nitrate faster and more reliably than the old belt conveyor. Dust levels in the facility dropped by 90%, improving air quality and reducing the risk of respiratory issues for workers. The plant also saw a 20% decrease in maintenance costs, as the pneumatic system required less frequent repairs and replacements. The overall productivity of the plant increased by 25%, and the quality of the ammonium nitrate produced improved, leading to higher customer satisfaction.
For industries dealing with ammonium nitrate, selecting the right material handling technology is crucial for maintaining efficiency, safety, and product quality. Pneumatic conveying technology offers a clean, efficient, and reliable solution that addresses the challenges of traditional methods. HeadPowder Engineering Co., Ltd. provides advanced pneumatic conveying systems that are tailored to the specific needs of its clients, ensuring optimal performance and long-term benefits. By investing in a pneumatic conveying system from HeadPowder, businesses can enhance their operational efficiency, reduce costs, and improve the overall safety of their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top