HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced pneumatic conveying solutions for industrial applications. The powder bin pneumatic conveying system is a critical component in material handling, designed to efficiently transport bulk powders and granules from storage bins to processing units. This system operates by utilizing compressed air or gas to create a flow of material through a pipeline network, ensuring smooth and reliable material transfer without the need for mechanical components like belts or buckets.
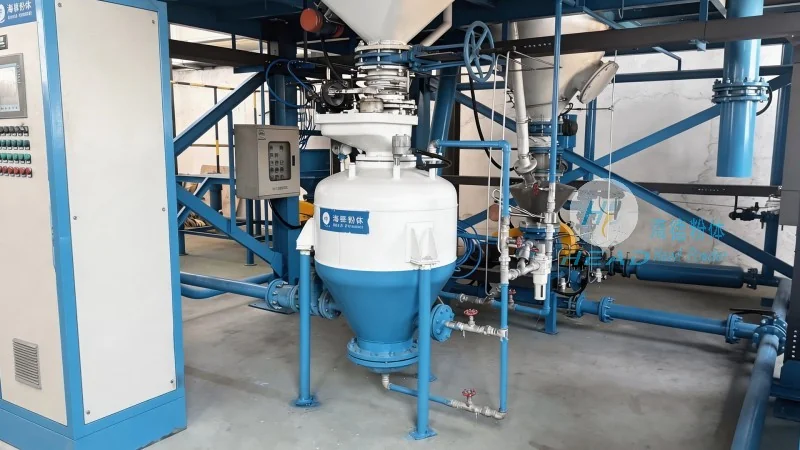
The core mechanism of the powder bin pneumatic conveying system involves several key steps. First, the material is stored in a large powder bin, which serves as the initial storage container. When the conveying process is initiated, a vacuum or pressure is applied to the system, depending on the specific design. Compressed air is then introduced into the bin, creating a flow of air that entrains the powder particles. The air-powder mixture travels through the pipeline to the destination point, where the material is discharged. The system typically includes a hopper or receiver at the end to collect the conveyed material, and a filter or separator to remove any excess air before it is released back into the environment. This process ensures that the material is transported efficiently and with minimal loss, maintaining product integrity throughout the transfer.
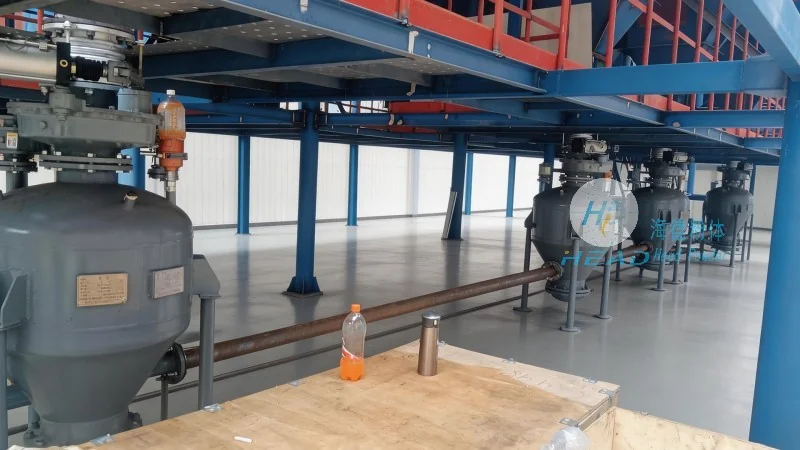
HeadPowder's powder bin pneumatic conveying system offers several distinct features that enhance its performance and usability. One of the primary advantages is its ability to handle a wide range of materials, from fine powders to coarse granules, without causing degradation or contamination. The system is also highly flexible, allowing for multiple transfer points and complex pipeline configurations to meet the specific needs of different industrial applications. Additionally, the design minimizes maintenance requirements, as there are no moving parts in direct contact with the material, reducing wear and tear and extending the system's operational lifespan. Another notable feature is the system's energy efficiency, as it uses compressed air to transfer material, which can be integrated with existing air systems in many facilities, reducing additional energy costs. The system also provides excellent dust control, as the material is contained within the pipeline and is not exposed to the environment during transport, improving safety and compliance with environmental regulations.
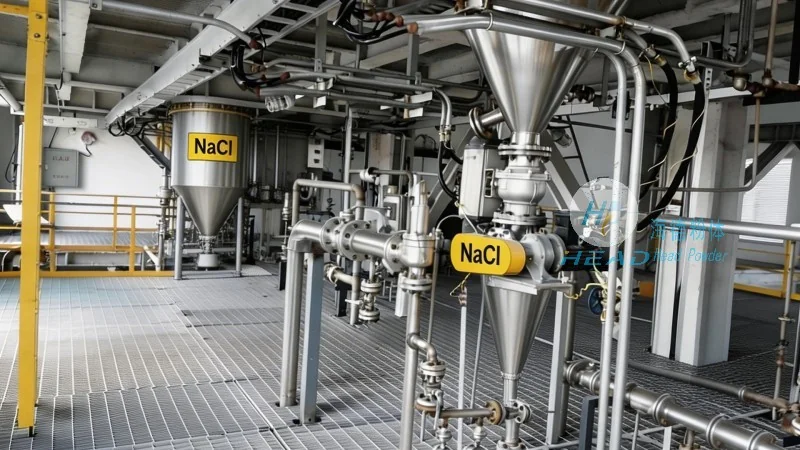
The powder bin pneumatic conveying system is widely used across various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, for example, the system is used to transport active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring that the product remains sterile and free from contamination. In food processing, the system handles ingredients like flour, sugar, and spices, maintaining the quality and safety of the final product. In chemical manufacturing, the system is used to transport raw materials and intermediates, improving process efficiency and reducing downtime. The system's ability to handle a variety of materials and its flexibility make it a versatile solution for many industrial applications.
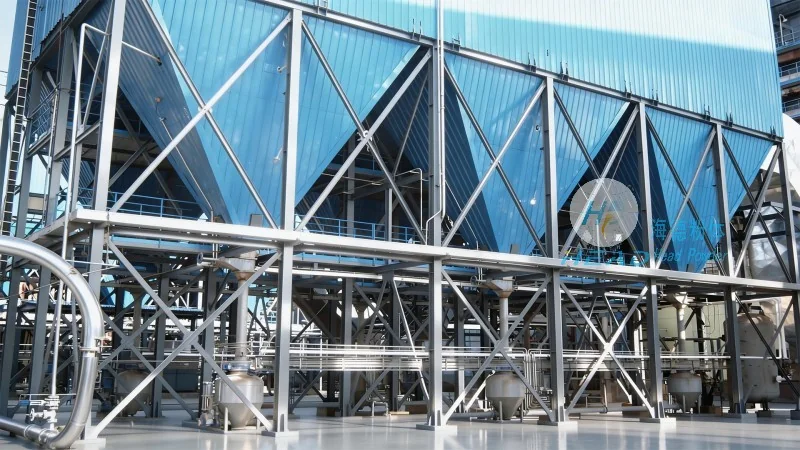
HeadPowder's powder bin pneumatic conveying system is a reliable and efficient solution for material handling in various industrial sectors. With its advanced design and features, the system ensures smooth and safe transport of bulk powders, while minimizing maintenance and operational costs. Based in Shandong, China, HeadPowder continues to innovate and provide high-quality pneumatic conveying solutions to meet the evolving needs of its clients. The company's commitment to quality and customer satisfaction makes it a trusted partner for businesses seeking effective material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top