Efficient and clean transportation of coke is a critical concern for industries relying on this essential raw material. Traditional methods often involve manual handling or mechanical conveyors, which can lead to dust pollution, operational inefficiencies, and increased maintenance costs. In response to these challenges, pneumatic conveying technology has emerged as a superior solution for coke handling, offering enhanced efficiency, environmental friendliness, and operational reliability.
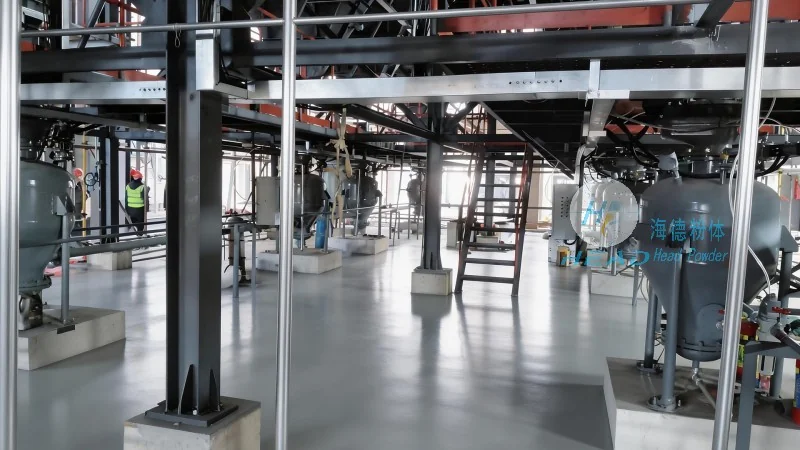
Pneumatic conveying systems utilize air pressure to move bulk materials like coke through a network of pipes. This technology eliminates the need for physical contact between the material and machinery, significantly reducing the risk of contamination and dust generation. The system typically consists of a hopper for material storage, a conveyor line with airlocks or rotary valves, and a receiver for the delivered coke. By controlling the air flow and pressure, operators can precisely regulate the speed and volume of coke transport, ensuring consistent performance and minimizing downtime.
One of the primary benefits of pneumatic conveying for coke is its ability to maintain a clean and dust-free environment. Unlike mechanical conveyors that generate significant dust, pneumatic systems contain the material within sealed pipes, preventing airborne particles from contaminating the workplace and affecting product quality. This not only improves safety but also reduces the need for extensive cleaning and maintenance, leading to lower operational costs over time.
Additionally, pneumatic conveying offers superior efficiency in terms of speed and throughput. By eliminating the need for manual loading and unloading, the system can process large volumes of coke quickly and continuously. The ability to adjust the air pressure and flow rate allows for flexible operation, accommodating varying production demands without compromising performance. This adaptability makes pneumatic conveying ideal for both small-scale and large-scale coke handling applications.
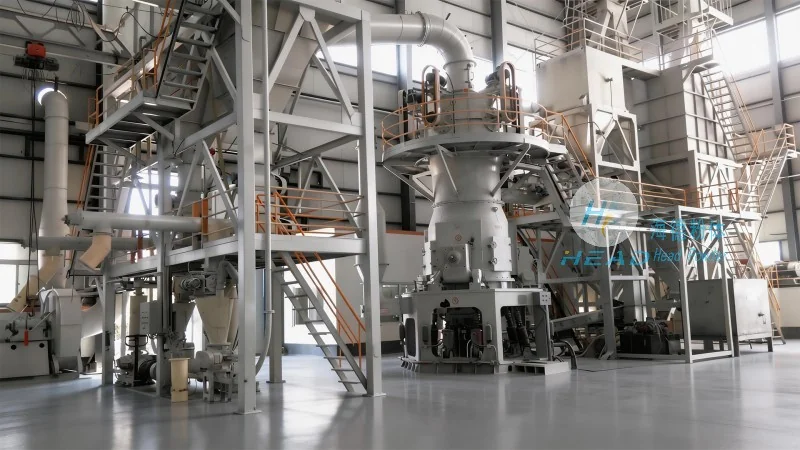
At the core of effective pneumatic conveying for coke are several key components that ensure optimal performance. The hopper, where coke is stored before transport, is designed with a sloped bottom to facilitate smooth material flow. Airlocks or rotary valves are used to control the release of coke into the conveyor line, preventing backflow and maintaining consistent material feed. The conveyor pipes are typically made of durable materials such as stainless steel or high-density polyethylene, which resist corrosion and wear from coke particles. The receiver, where the coke is deposited, is equipped with a dust collection system to capture any residual particles, further enhancing the clean operation of the system.
Pneumatic conveying technology is widely adopted across various industries that rely on coke as a key ingredient. In the steel industry, for example, coke is used in blast furnaces to reduce iron ore to molten iron. The ability to efficiently transport coke to these furnaces without contamination is crucial for maintaining consistent production and quality. Similarly, in the foundry industry, coke is used as a fuel source and a reducing agent in the casting process. Pneumatic conveying ensures that coke is delivered to the foundry in a clean and controlled manner, supporting efficient production and reducing waste.
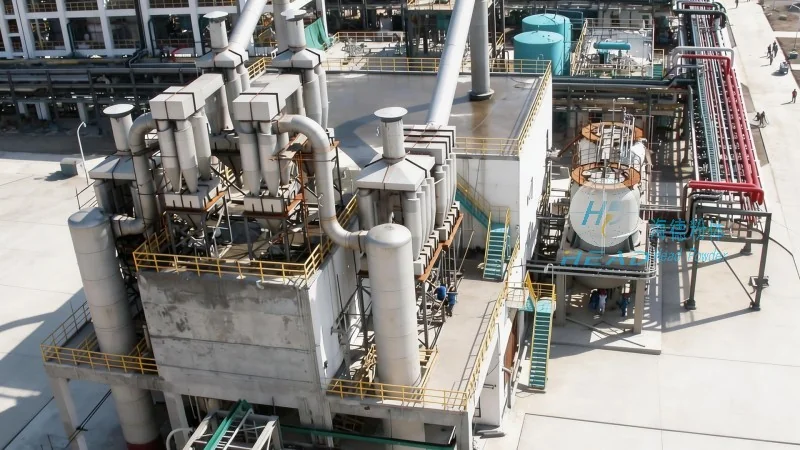
Other industries that benefit from pneumatic conveying include cement production, where coke is used as a fuel in kilns, and chemical manufacturing, where coke is a raw material for various processes. The versatility of pneumatic systems allows them to adapt to different material characteristics and operational requirements, making them a reliable choice for diverse applications.
When selecting a pneumatic conveying system for coke handling, several factors should be considered to ensure optimal performance and cost-effectiveness. The first consideration is the material characteristics of the coke, including its size, density, and moisture content. These factors influence the choice of system type, such as pressure or vacuum conveying, and the design of components like the hopper and airlocks. The required throughput and distance of transport are also critical, as they determine the necessary air pressure and pipe diameter. Additionally, the space available for installation and the environmental regulations in the operating area should be taken into account to ensure compliance and efficient operation.
Working with a reputable engineering company, such as Shandong HeadPowder Engineering Co., Ltd., can provide valuable guidance in selecting and implementing the right pneumatic conveying solution. With expertise in bulk material handling and a commitment to clean, efficient technology, HeadPowder offers customized solutions tailored to the specific needs of each client. Their team of engineers can assess operational requirements, recommend appropriate system configurations, and provide support throughout the installation and commissioning process, ensuring that the chosen solution delivers maximum efficiency and reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top