When it comes to transporting kaolin—a fine, white clay mineral—through pneumatic conveying systems, preventing pipeline blockages is a critical challenge. Kaolin's unique physical properties, such as its high fineness and tendency to agglomerate, can easily lead to clogging if the system is not properly designed and operated. This article explores effective strategies to prevent blockages and highlights the key design parameters that engineers must consider to ensure smooth, reliable operation of pneumatic conveying systems for kaolin transport.
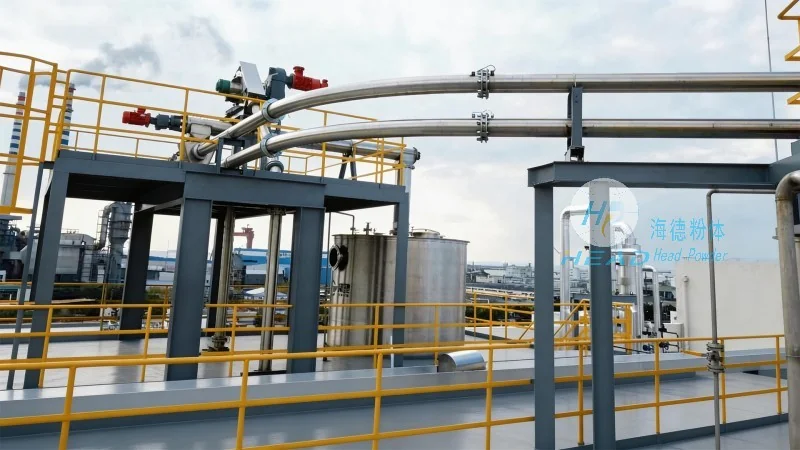
Kaolin, also known as china clay, is widely used in various industries including ceramics, paper, and coatings due to its excellent whiteness and plasticity. Its fine particle size (typically ranging from 1 to 10 microns) and high surface area make it prone to sticking together, which can cause blockages in the conveying lines. Additionally, kaolin's low bulk density and high moisture content can affect the flow characteristics, further complicating the design of the pneumatic system. To address these challenges, a thorough understanding of kaolin's behavior under different operating conditions is essential.
Several critical design parameters play a pivotal role in preventing pipeline blockages in pneumatic conveying systems for kaolin. These parameters are tailored to the specific properties of kaolin and the operational requirements of the system. The following sections outline the most important considerations:
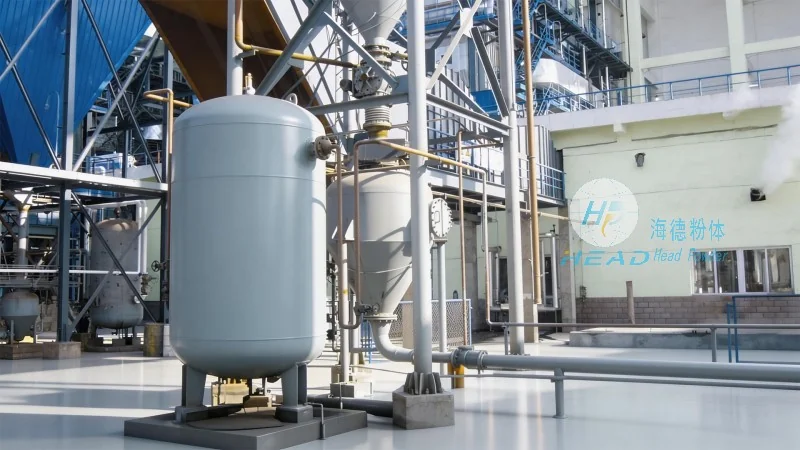
One of the most fundamental parameters in pneumatic conveying is the air velocity. For kaolin, maintaining an appropriate air velocity is crucial to prevent particle agglomeration and ensure proper suspension. The air velocity must be high enough to keep the particles in suspension but not so high as to cause excessive wear on the system components. Typically, a velocity range of 20 to 30 meters per second is recommended for fine kaolin particles. The flow rate, which is directly related to the air velocity, must also be optimized to match the material feed rate and the system's capacity. A mismatch between the air flow and the material feed can lead to surging or blockages, especially when handling high moisture content kaolin.
The configuration of the pneumatic conveying system, including the type of pipeline (e.g., positive pressure, negative pressure, or mixed pressure), significantly impacts the risk of blockages. Positive pressure systems, where air is forced through the pipeline, are generally more suitable for kaolin transport as they provide better control over the material flow and reduce the risk of particle deposition. The pipeline diameter is another critical parameter; larger diameters reduce the friction losses and the likelihood of particle accumulation, while smaller diameters may increase the risk of blockages if the air velocity is not properly maintained. Properly sized and configured pipelines are essential to maintain consistent flow and prevent the buildup of kaolin particles.
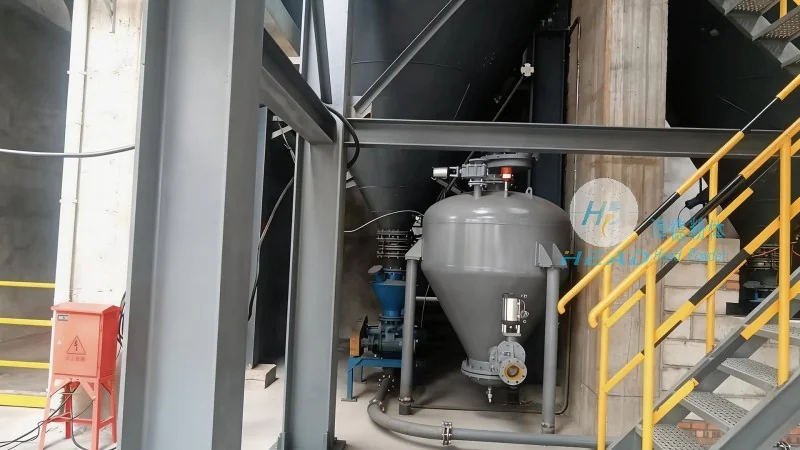
The way kaolin is fed into the system and any conditioning steps taken before conveying can greatly influence the risk of blockages. A consistent and controlled feed rate is vital to avoid surging or overloading the system. Conditioning kaolin, such as drying or adding anti-agglomerating agents, can improve its flowability and reduce the tendency to stick together. For example, drying kaolin to a moisture content below 2% can significantly enhance its flow characteristics and minimize the risk of clogging. Additionally, using feeders with adjustable speed controls allows for precise material input, ensuring that the air flow and material flow remain balanced.
Even with optimal design, regular cleaning and maintenance are necessary to prevent long-term blockages. Kaolin particles can accumulate on pipeline walls and system components over time, especially if the system is not operated continuously. Implementing a cleaning schedule, such as using air blasts or mechanical scrapers, can help remove accumulated material and maintain the system's efficiency. Regular inspection of the pipeline and components for signs of wear or buildup is also recommended to identify and address potential issues before they lead to blockages.
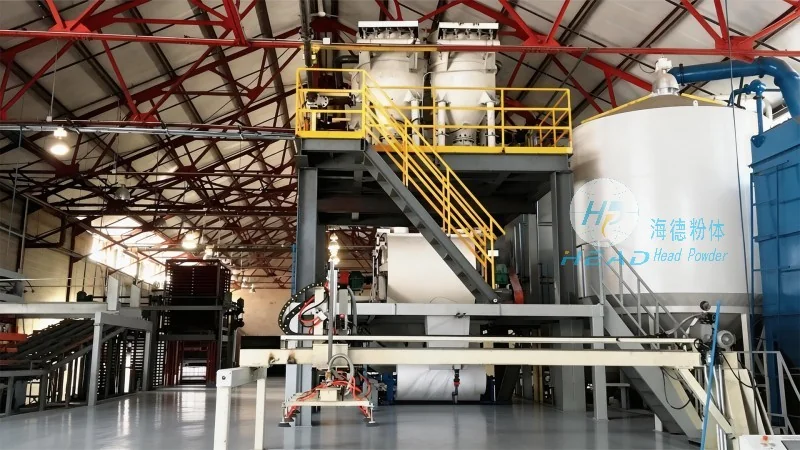
Advanced control systems and real-time monitoring are essential for preventing blockages in pneumatic conveying systems for kaolin. Sensors can be installed to monitor air pressure, flow rate, and material level, providing early warnings of any deviations from the optimal operating conditions. Automated control systems can adjust the air velocity or flow rate in response to changes in material feed or system pressure, ensuring that the system remains stable and free from blockages. Real-time data analysis can also help identify patterns or trends that may indicate potential issues, allowing for proactive maintenance and adjustments.
Preventing pipeline blockages in pneumatic conveying systems for kaolin requires a comprehensive approach that considers the unique properties of kaolin and the specific design parameters of the system. By optimizing air velocity and flow rate, selecting appropriate pipeline configurations, managing material feed and conditioning, implementing regular maintenance, and utilizing advanced control systems, engineers can significantly reduce the risk of blockages and ensure the smooth operation of kaolin transport systems. These strategies not only improve the efficiency and reliability of the system but also extend its lifespan and reduce maintenance costs. As a leading provider of engineering solutions for material handling, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing pneumatic conveying systems tailored to the needs of industries handling kaolin. With years of experience in the field, the company offers expert guidance and customized solutions to help clients achieve optimal performance and minimize the risk of blockages in their kaolin transport operations. The address of the company is in Shandong, China, where it serves clients globally with its advanced technology and commitment to quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top