For businesses in the brown sugar industry, optimizing the transportation process is crucial for maintaining product quality and operational efficiency. The brown sugar pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., represents a significant advancement in this field. This system is designed to handle the unique challenges associated with brown sugar, such as its granular structure and moisture content, ensuring a smooth and efficient transfer from storage to processing or packaging areas.
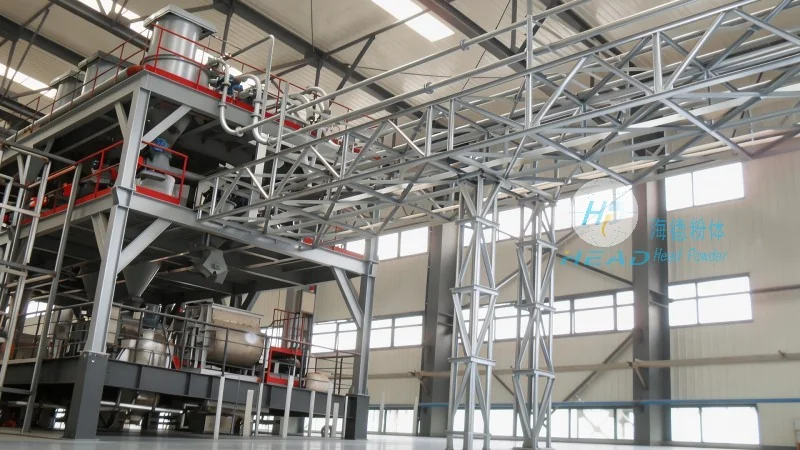
The system incorporates several key features that enhance its performance and reliability. One of the primary advantages is its ability to maintain consistent air pressure and flow rates, which is essential for preventing product degradation and ensuring uniform handling. The equipment is constructed with high-quality materials, including corrosion-resistant components, to withstand the chemical properties of brown sugar and the environmental conditions in processing facilities. Additionally, the system is equipped with advanced control mechanisms that allow for real-time monitoring and adjustment, enabling operators to optimize performance based on production demands.
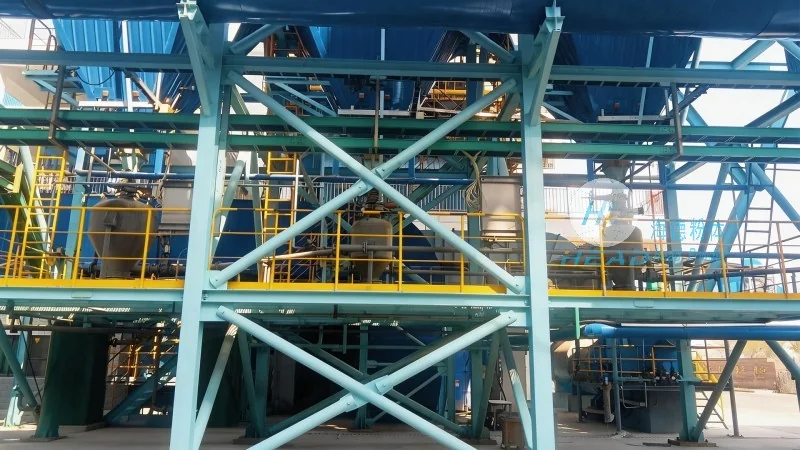
The brown sugar pneumatic conveying system operates on the principle of air-based transport. It uses a combination of positive and negative pressure to move brown sugar through a network of pipes. The process begins with the sugar being fed into a hopper, where it is then conveyed by an air stream. The system includes components such as rotary valves, filters, and dust collectors to ensure that the material is transported efficiently while minimizing dust and maintaining product integrity. The design allows for flexible configurations, accommodating various production scales and layouts, from small-scale operations to large industrial facilities.
Implementing the brown sugar pneumatic conveying system offers numerous benefits for producers. Firstly, it significantly reduces labor costs by automating the transportation process, minimizing the need for manual handling and reducing the risk of product contamination. Secondly, the system enhances product quality by preventing exposure to air and moisture, which can cause clumping or spoilage. This leads to higher yields and better marketability of the final product. Thirdly, the system improves operational efficiency by streamlining the workflow, allowing for faster production cycles and increased output. The advanced control features also enable better management of inventory and production planning, contributing to overall business optimization.
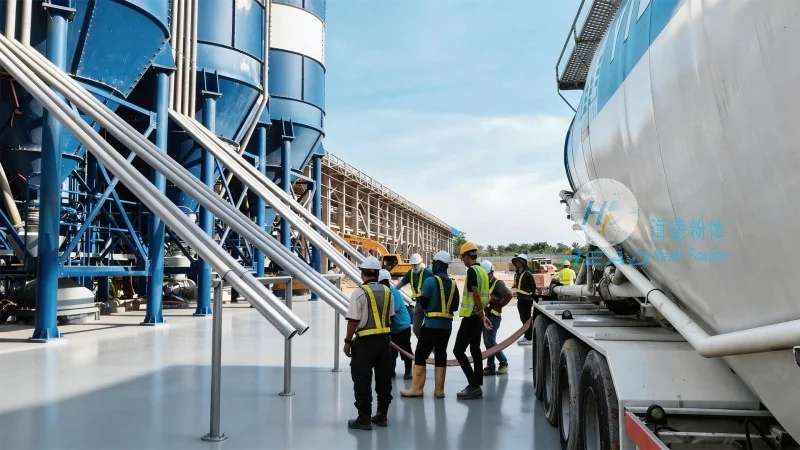
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial conveying systems. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the food processing industry. HeadPowder specializes in designing and manufacturing customized solutions tailored to the specific needs of its clients, ensuring that each system is optimized for performance, durability, and cost-effectiveness. The company's headquarters is located in Shandong, China, where it leverages its expertise and resources to develop cutting-edge technologies for the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top