Long - distance pneumatic conveying systems for coal ash have become increasingly vital in modern industrial operations, offering efficient and reliable solutions for transporting bulk materials over extended distances. This technology has revolutionized the handling of coal ash, a by - product of coal combustion, by providing a dust - free, low - maintenance, and environmentally friendly method of material transport. The system's design and implementation are crucial for optimizing industrial processes, ensuring safety, and enhancing operational efficiency.
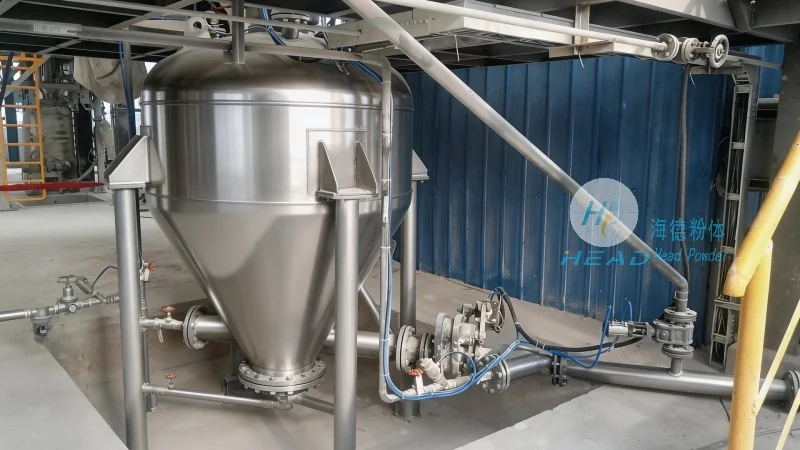
At Shandong HeadPowder Engineering Co., Ltd., we specialize in developing and manufacturing advanced pneumatic conveying systems tailored to the unique needs of coal ash handling. With our headquarters located in Shandong, China, our team of experienced engineers and technicians leverages cutting - edge technology and industry best practices to deliver high - performance, durable, and cost - effective solutions. Our company, commonly known as HeadPowder, has built a strong reputation for excellence in the field of bulk material handling, serving a wide range of industrial clients across various sectors.
The long - distance pneumatic conveying system for coal ash is engineered with several key features that set it apart from traditional transport methods. Firstly, it utilizes a combination of positive and negative pressure air flow to move coal ash particles through a network of pipes. This method eliminates the need for mechanical components like conveyors or elevators, reducing wear and tear and maintenance costs. Secondly, the system is designed to handle a wide range of ash particle sizes and moisture content, ensuring consistent and reliable operation. Advanced control systems are integrated to monitor and adjust air pressure, flow rate, and particle velocity in real - time, optimizing performance and preventing system failures. Additionally, the system incorporates dust suppression and filtration mechanisms to meet environmental regulations and maintain a clean working environment.
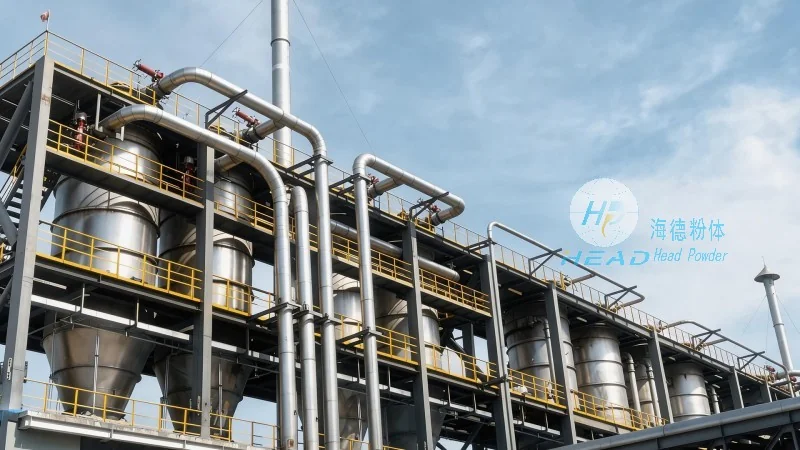
Implementing a long - distance pneumatic conveying system for coal ash offers numerous benefits for industrial operations. One of the primary advantages is the significant reduction in labor costs and operational downtime. By automating the material transport process, companies can minimize manual handling, which not only saves time but also enhances worker safety. The system's ability to transport materials over long distances without the need for intermediate storage or transfer points streamlines the overall production flow, improving productivity and throughput. Furthermore, the dust - free operation of the system contributes to a cleaner workplace, reducing health hazards and improving air quality. This is particularly important in environments where air quality is a concern, as it helps comply with environmental regulations and maintain a safe working atmosphere. The low maintenance requirements of the system also lead to long - term cost savings, as there are fewer mechanical parts to replace or repair, resulting in lower operational expenses over the system's lifespan.
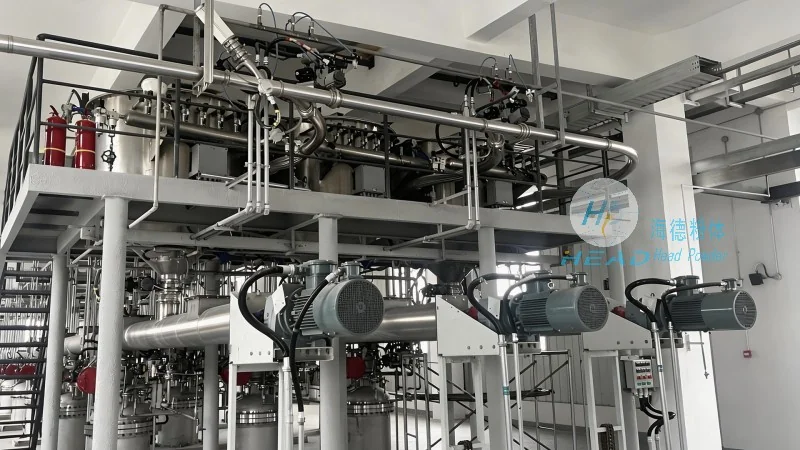
The long - distance pneumatic conveying system for coal ash is widely used in various industrial applications, particularly in power plants, cement factories, and waste management facilities. In power plants, the system is employed to transport coal ash from the boiler to storage silos or disposal sites, ensuring efficient and safe handling of the by - product. In cement factories, the system is used to convey coal ash as a raw material for cement production, improving the quality and consistency of the final product. Waste management facilities also benefit from this technology by transporting coal ash for recycling or disposal, contributing to sustainable waste management practices. The system's adaptability allows it to be customized to fit the specific requirements of each application, whether it's for short - distance or long - distance transport, high or low flow rates, or different particle sizes.
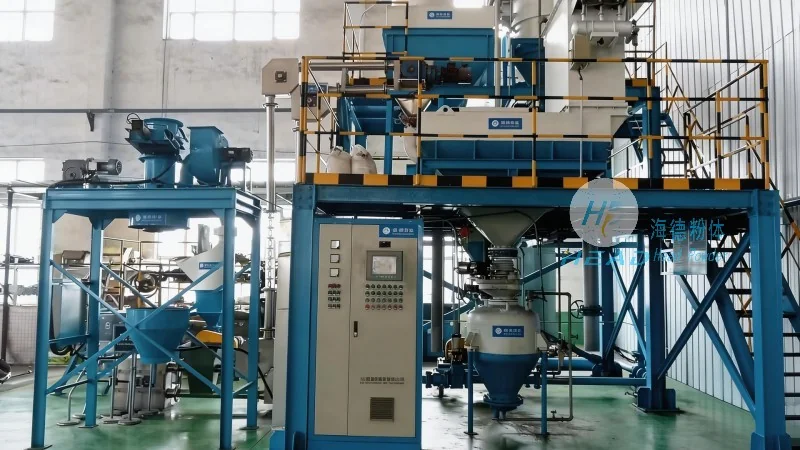
HeadPowder understands that each industrial facility has unique operational requirements, and our long - distance coal ash pneumatic conveying systems are designed to be highly customizable. We work closely with clients to assess their specific needs, including the distance of transport, the volume of material to be handled, and the existing infrastructure. Our engineers can design a system that integrates seamlessly with existing equipment, such as storage silos, processing units, or disposal facilities. This integration ensures that the new system complements the existing operations without disrupting the workflow. Additionally, we offer a range of accessories and components, such as air filters, silencers, and control panels, to enhance the system's performance and meet specific environmental or safety standards. Our commitment to customization ensures that each system is tailored to provide the best possible solution for the client's particular application.
At Shandong HeadPowder Engineering Co., Ltd., we prioritize quality and reliability in all our products. Our long - distance pneumatic conveying systems for coal ash are manufactured using high - quality materials and components, ensuring durability and long - term performance. Each system undergoes rigorous testing and quality control checks before delivery to ensure it meets or exceeds industry standards. We also provide comprehensive after - sales support, including installation, commissioning, and maintenance services, to ensure that our clients can rely on the system's consistent performance. Our team of experienced technicians is available to provide technical support and troubleshooting assistance, helping to minimize downtime and maximize the system's operational efficiency. By choosing HeadPowder, clients can be confident that they are investing in a reliable and high - performance solution that will meet their needs for years to come.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top