Chocolate pneumatic conveying systems are essential in the chocolate manufacturing industry, enabling efficient and hygienic transportation of chocolate powders and related materials. This article provides an overview of the working principles, classification, and practical applications of chocolate pneumatic conveying technology, presented by Shandong HeadPowder Engineering Co., Ltd. (headpowder), a leading engineering company based in Shandong, China.
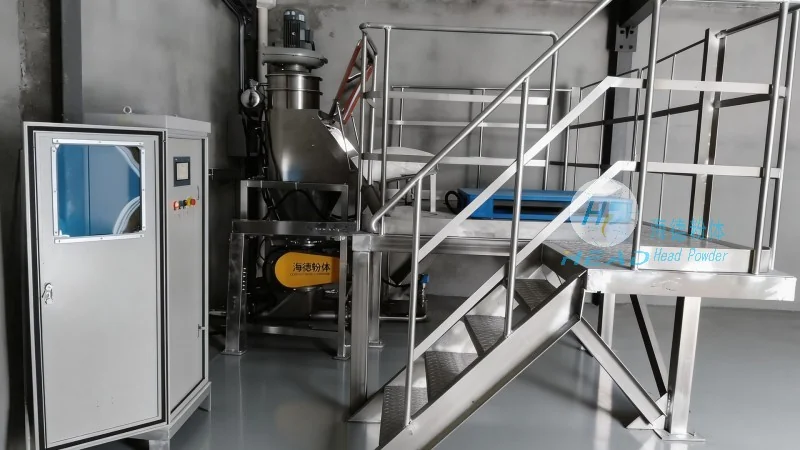
Chocolate pneumatic conveying operates on the principle of using air to transport solid materials, such as cocoa powder, sugar, and other ingredients, through a pipeline system. The process typically involves a vacuum or pressure system that draws or pushes the material along the conveyor line. The system consists of several key components, including a hopper for material storage, a conveyor line, a separator to remove excess air, and a receiver for the conveyed material. The air flow is controlled to ensure optimal material transport, minimizing product degradation and maintaining product quality. The working principle is based on the balance between the air velocity and the material's properties, such as particle size, density, and moisture content. By adjusting the air pressure and flow rate, manufacturers can achieve efficient and consistent conveying of chocolate products.
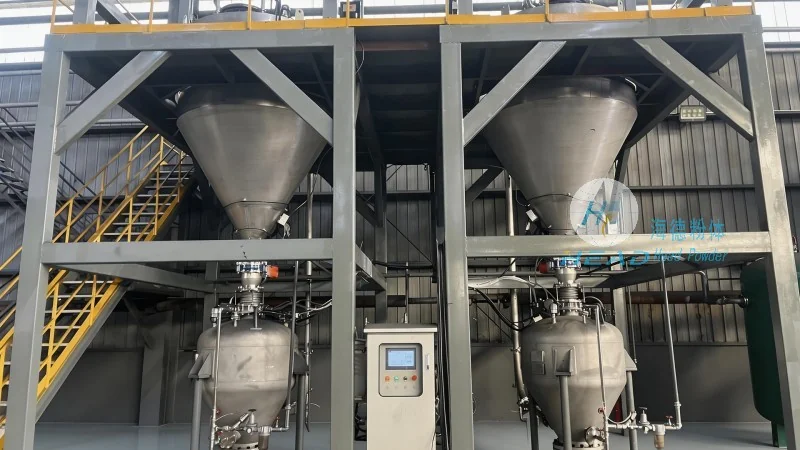
Chocolate pneumatic conveying systems are classified based on the operating pressure and the method of material transport. The two main categories are vacuum conveying and pressure conveying. Vacuum conveying systems use a vacuum pump to create a negative pressure that draws material from the source to the receiver. This method is suitable for transporting materials from lower to higher elevations and is commonly used for handling fine powders like cocoa. Pressure conveying systems, on the other hand, use a positive pressure to push material through the pipeline. This approach is ideal for transporting materials over longer distances and at higher speeds. Additionally, systems can be further classified by the type of air flow, such as dilute phase and dense phase conveying. Dilute phase systems use high air velocities to transport materials in a suspended state, while dense phase systems use lower air velocities to move material in a slurry-like state, reducing the risk of product degradation and clogging.
Chocolate pneumatic conveying is widely used in various stages of chocolate production. In the ingredient handling phase, it efficiently transports cocoa powder, sugar, and milk powder from storage silos to processing lines. This ensures a continuous and hygienic supply of raw materials, reducing downtime and improving production efficiency. During the mixing and blending process, the system helps to evenly distribute ingredients, contributing to consistent chocolate flavor and texture. In the packaging stage, pneumatic conveying can transport finished chocolate products or packaging materials to the packaging line, streamlining the overall production workflow. The technology is also applied in quality control and inspection processes, where it assists in transporting samples for testing and analysis. By integrating pneumatic conveying systems, chocolate manufacturers can enhance operational efficiency, maintain product quality, and reduce labor costs.
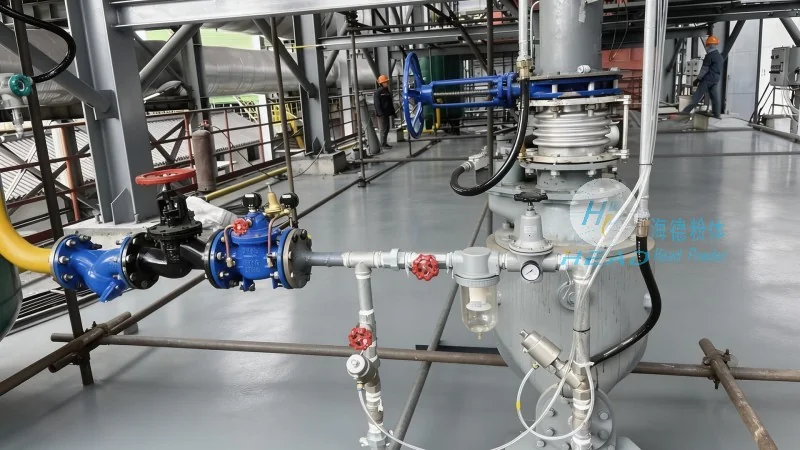
Implementing chocolate pneumatic conveying offers several advantages. Firstly, it provides a hygienic and closed system, preventing contamination from external sources and maintaining product purity. This is crucial in the food industry, where product safety and quality are paramount. Secondly, the system reduces labor requirements by automating material transport, allowing workers to focus on other critical tasks. Thirdly, it minimizes product degradation by controlling air flow and temperature, preserving the flavor and texture of chocolate ingredients. However, there are considerations to keep in mind when selecting a system. The choice between vacuum and pressure conveying depends on the specific application and material characteristics. Additionally, the system's design must consider the material's particle size and moisture content to avoid clogging or blockages. Regular maintenance and cleaning are essential to ensure the system operates efficiently and prolong its lifespan. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized chocolate pneumatic conveying solutions tailored to the unique needs of each client, ensuring optimal performance and reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top