For agricultural and industrial operations, efficient and reliable material handling is crucial, especially when dealing with bulk commodities like corn. Pneumatic conveying systems offer a versatile solution for transporting corn from storage to processing facilities, or between different stages of production. The fundamental principle of corn pneumatic conveying involves using air pressure to move corn particles through a pipeline network. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and increasing operational safety. The process typically starts with a hopper or storage silo where corn is loaded. An air compressor then generates the necessary pressure to draw corn into the pipeline. As the corn travels through the system, it is propelled by the moving air, which can be either positive pressure (where air pushes the material) or negative pressure (where air pulls the material). The choice between these two methods depends on the specific application and the distance the corn needs to be transported.
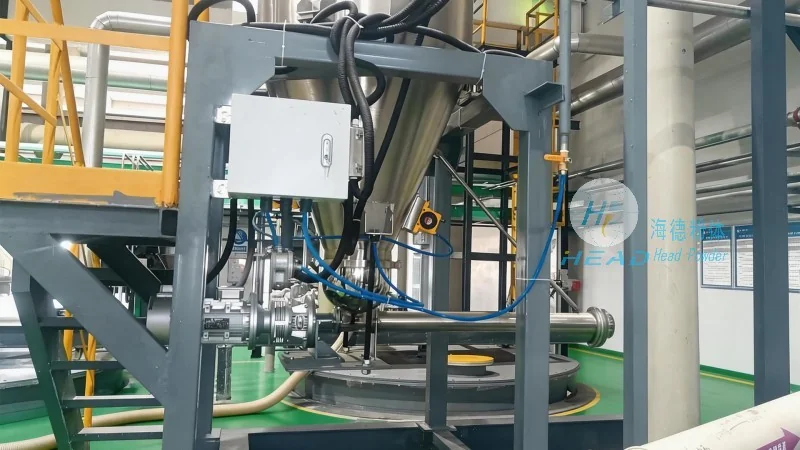
The core mechanism of corn pneumatic conveying relies on the interaction between air flow and corn particles. In a positive pressure system, a blower or compressor supplies compressed air into the conveying line, creating a pressure differential that forces corn to move from the source to the destination. The air velocity must be sufficient to overcome the gravitational force and frictional resistance of the corn particles. Conversely, in a negative pressure system, a vacuum pump creates a low-pressure environment at the receiving end, drawing corn from the source through the pipeline. Both systems require careful design to ensure that the air velocity is within the appropriate range to prevent particle degradation or blockages. The design of the system, including the size of the pipeline, the type of air nozzle, and the placement of inlets and outlets, directly impacts the efficiency and effectiveness of corn transportation.
Based on the pressure and flow characteristics, corn pneumatic conveying systems can be classified into several types. The most common categories include dilute phase and dense phase systems. Dilute phase systems operate at higher air velocities, typically moving corn particles in a dispersed state, similar to a cloud of dust. This method is suitable for short to medium distances and when the corn is relatively dry. Dense phase systems, on the other hand, operate at lower air velocities, where corn particles are conveyed in a more concentrated stream, often with a higher solids-to-air ratio. This approach is ideal for longer distances and when the corn is wet or contains more impurities, as it reduces the risk of particle degradation and blockages. Another classification is based on the direction of air flow, with horizontal and vertical conveying systems being the most prevalent. Horizontal systems are used for transporting corn over relatively short distances, while vertical systems are employed for moving corn vertically, such as from a lower storage level to an upper processing unit. The selection of the appropriate system type depends on factors like the distance to be covered, the height of the vertical lift, and the characteristics of the corn being conveyed.
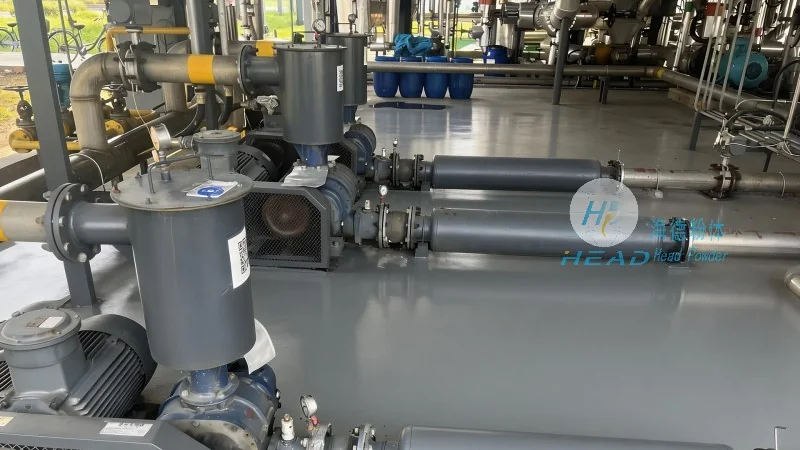
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of corn processing industries. These systems are widely used in corn milling, ethanol production, and animal feed manufacturing. In corn milling, pneumatic conveyors efficiently transport corn from storage silos to grinding and processing equipment, ensuring a continuous flow of raw material. In ethanol production, the system helps move corn from the storage area to the fermentation tanks, maintaining the necessary supply for the production process. For animal feed manufacturers, the technology is used to transport corn from storage to mixing and packaging units, enhancing operational efficiency and reducing labor costs. The versatility of corn pneumatic conveying systems allows them to handle various corn qualities, from fresh to dried, and different moisture contents, making them suitable for a wide range of industrial applications.
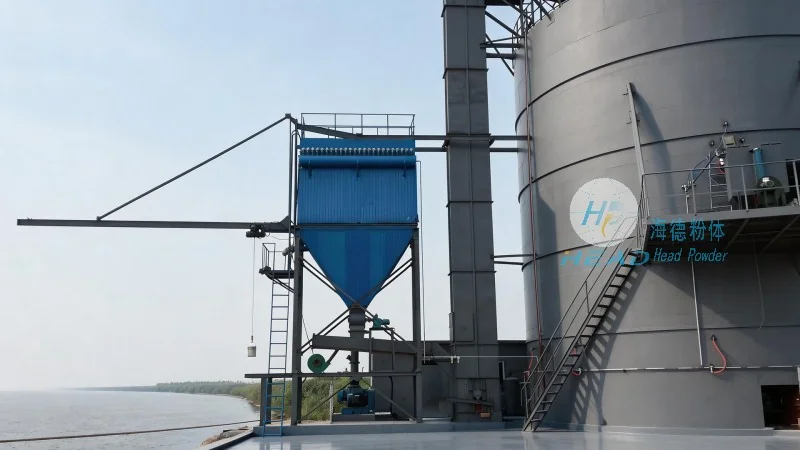
Implementing corn pneumatic conveying systems offers several advantages over traditional mechanical methods. One of the key benefits is the reduction in maintenance costs, as there are fewer moving parts and mechanical components. This leads to lower operational expenses and increased system reliability. Additionally, pneumatic conveying systems are more hygienic and easier to clean, which is particularly important in food processing industries where sanitation is critical. The systems also provide better control over the flow rate and direction of corn, allowing for precise management of the material handling process. However, there are also considerations to keep in mind when using pneumatic conveying for corn. For instance, the system requires a consistent air supply, and any fluctuations in pressure can affect the conveying efficiency. Moreover, the design must account for the potential for corn to degrade or become contaminated during transport, especially if the system is not properly maintained. Proper filtration and cleaning of the air system are essential to prevent the buildup of dust and impurities that could affect the quality of the corn being conveyed.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of pneumatic conveying systems specializing in corn and other bulk material handling solutions. With headquarters in Shandong, China, the company has established itself as a trusted provider of efficient and reliable material transport technologies for agricultural and industrial sectors. HeadPowder's expertise lies in designing customized pneumatic conveying systems that meet the specific requirements of clients, ensuring optimal performance and durability. The company's products are engineered to handle various conditions, from dry to wet corn, and different processing needs, making them suitable for a wide range of applications in the corn industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top