Ammonium nitrate is a widely used chemical compound in various industrial sectors, including agriculture, explosives, and chemical manufacturing. The efficient and safe handling of this material is crucial for industrial operations. Pneumatic conveying is a key technology used to transport ammonium nitrate and other bulk materials. This article explores the concept of ammonium nitrate pneumatic conveying, its classification, and practical applications in industrial settings.
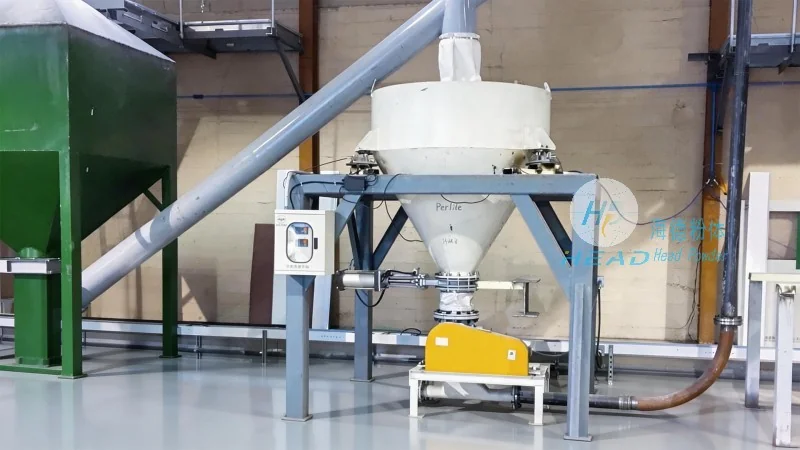
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using a stream of air. In the case of ammonium nitrate, this technology is employed to move the material from storage to processing units or from production lines to packaging areas. The process involves creating a pressure differential or using vacuum to move the material, ensuring minimal dust generation and enhanced safety compared to traditional methods like belt conveyors or trucks.
Ammonium nitrate is a granular or powdered chemical, and its handling requires specialized equipment to prevent caking, segregation, and dust explosion risks. Pneumatic conveying systems are designed to address these challenges by maintaining consistent material flow and controlling air pressure and velocity. The system typically consists of a hopper, a conveyor line, and a receiver, with optional components like filters, cyclones, and rotary valves to manage the material and air flow effectively.
Pneumatic conveying systems are generally classified into two main categories: pressure and vacuum systems. Each type has distinct characteristics and is suitable for different operational requirements.
Pressure pneumatic conveying systems operate by forcing air and material through the pipeline using a positive pressure source, such as a blower or compressor. This method is ideal for short to medium-distance transport and is commonly used in applications where the material needs to be conveyed from a central storage to multiple processing points. The pressure system ensures a continuous flow of material and can handle a wide range of particle sizes and densities.
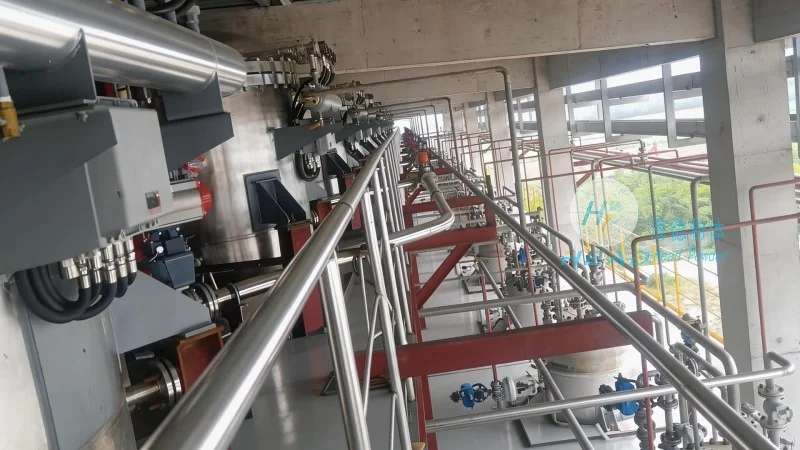
Vacuum pneumatic conveying systems, on the other hand, use a vacuum pump to create a negative pressure in the pipeline, drawing the material from the source into the system. This type of system is suitable for long-distance transport and is often used when the material is located at a higher elevation or needs to be transported from multiple sources to a central location. Vacuum systems are particularly effective for handling fine powders and can maintain a stable flow even with varying material characteristics.
Within these main categories, there are further subtypes based on the air flow direction and the method of material transport. For example, dense phase conveying is a variation of pressure systems that operates at lower air velocities, reducing material degradation and increasing system efficiency. This method is commonly used for sensitive materials like ammonium nitrate, where maintaining particle integrity is critical.
The application of pneumatic conveying in ammonium nitrate handling spans across various industries, ensuring efficient material movement and process optimization.
In the agricultural sector, ammonium nitrate is used as a nitrogen fertilizer. Pneumatic conveying systems are employed to transport the fertilizer from production facilities to storage silos or directly to agricultural fields. This method allows for precise dosing and reduces the risk of contamination or loss during transport. The systems are designed to handle large volumes of granular fertilizer, ensuring consistent delivery to farmers and agricultural cooperatives.
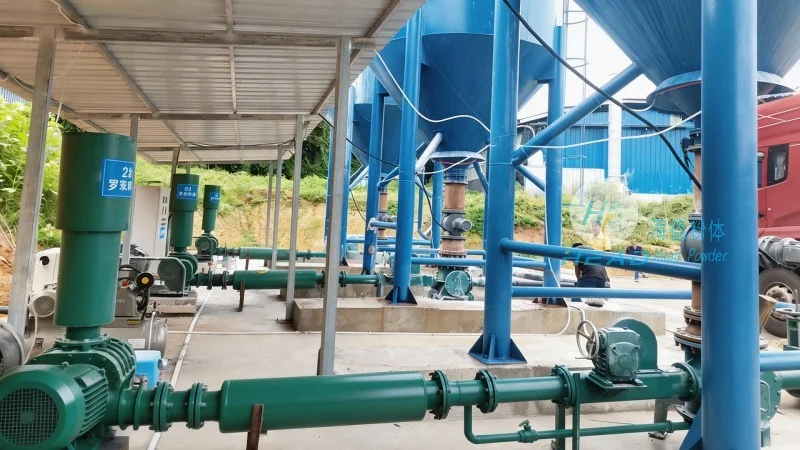
In the explosives industry, ammonium nitrate is a key component in the production of blasting agents. Pneumatic conveying is used to transport the material from storage to mixing and packaging units. The technology ensures that the material is handled safely and efficiently, minimizing the risk of accidental detonation or exposure to moisture. The systems are equipped with safety features such as explosion-proof designs and material flow monitoring to maintain operational safety.
In chemical manufacturing, ammonium nitrate is used in various processes, including the production of other nitrogen-based compounds. Pneumatic conveying systems are integrated into production lines to transport the material between reactors, filters, and storage tanks. This integration improves process efficiency by reducing downtime and ensuring a steady supply of raw material. The systems are designed to handle the specific requirements of chemical processes, such as temperature control and material purity.
Additionally, pneumatic conveying is used in the handling of ammonium nitrate for industrial applications like snow removal and de-icing. In these cases, the material is transported from storage to application equipment, ensuring that the right amount of ammonium nitrate is delivered to the treatment sites. The systems are often mobile and can be adapted to different operational needs, providing flexibility in industrial applications.
Implementing pneumatic conveying systems for ammonium nitrate handling offers several advantages over traditional methods. These benefits include improved safety, increased efficiency, and reduced operational costs.
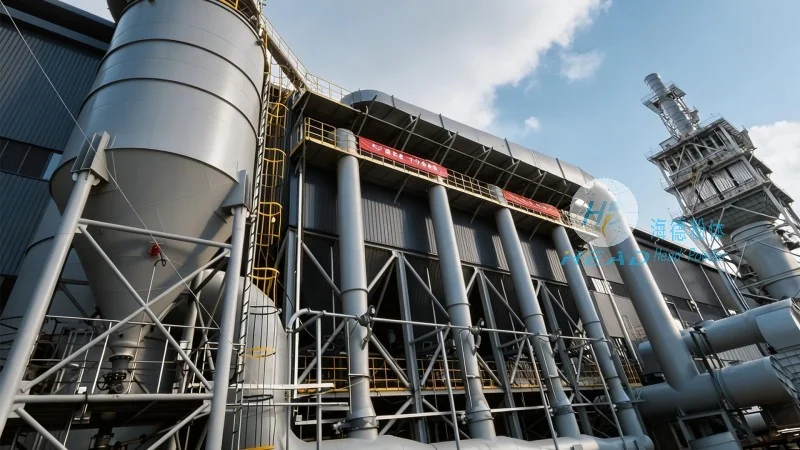
Firstly, pneumatic conveying systems significantly reduce the risk of dust explosions and material contamination. By containing the material within a closed pipeline system, the risk of dust dispersion is minimized. This is particularly important for ammonium nitrate, which is a hazardous material when exposed to ignition sources. The closed system also prevents contamination from external sources, ensuring the material remains pure and meets quality standards.
Secondly, pneumatic conveying enhances operational efficiency by allowing for continuous and automated material transport. Unlike traditional methods that may require manual handling or frequent stops, pneumatic systems can operate continuously, reducing downtime and increasing production throughput. The automation of the process also reduces the need for manual labor, lowering labor costs and improving workplace safety.
Thirdly, the technology offers cost savings in terms of energy consumption and maintenance. While initial setup costs may be higher, the long-term operational costs are lower due to reduced material loss and lower maintenance requirements. The systems are designed to be durable and reliable, with components that require minimal maintenance, such as filters and pumps. This reduces the overall cost of ownership and improves the return on investment for industrial operations.
Pneumatic conveying is a critical technology for the efficient and safe handling of ammonium nitrate in various industrial applications. By understanding the different classifications of pneumatic systems and their applications, industries can optimize their material transport processes. The use of specialized equipment and systems, such as those provided by Shandong HeadPowder Engineering Co., Ltd., ensures that ammonium nitrate is handled safely and effectively, meeting the demands of modern industrial operations. As the demand for ammonium nitrate continues to grow, the importance of reliable pneumatic conveying systems will only increase, making it a vital component in industrial material handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top