Calcium carbonate powder pneumatic conveying systems are widely used in industrial applications for the efficient and safe transportation of fine powders. These systems are essential for processes involving calcium carbonate, a key raw material in various industries such as paper, plastics, and coatings. The design and functionality of these systems vary based on specific operational requirements, material properties, and environmental considerations. This article provides an overview of the classification and key components of calcium carbonate powder pneumatic conveying systems, with a focus on the expertise and solutions offered by Shandong HeadPowder Engineering Co., Ltd., a leading provider based in China.
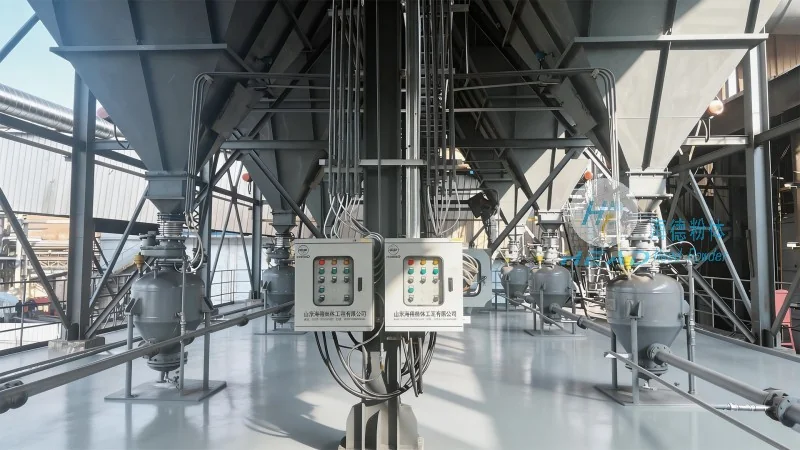
Calcium carbonate (CaCO₃) is a common mineral used as a filler or pigment in many industrial products. When processed as a fine powder, its handling requires specialized equipment to prevent dust accumulation, material degradation, and operational inefficiencies. Pneumatic conveying systems offer a solution by using air or gas to transport the powder through a sealed system, minimizing environmental impact and ensuring product integrity. The effectiveness of these systems depends on proper classification of the application and the selection of appropriate components.
Pneumatic conveying systems for calcium carbonate powder are typically classified into two main categories: suction (or vacuum) systems and pressure systems. Each type has distinct characteristics and is suited to different operational scenarios.
Suction systems operate by creating a negative pressure at the inlet, drawing the powder from the source into the conveying line. This method is ideal for applications where the material is located at a higher elevation than the discharge point or where the process requires a gentle handling approach. The system typically includes a vacuum pump, a hopper for material storage, and a filter to capture any fines before releasing the air back to the environment. Suction systems are particularly effective for transporting calcium carbonate powder from storage silos or processing equipment to a central collection point.
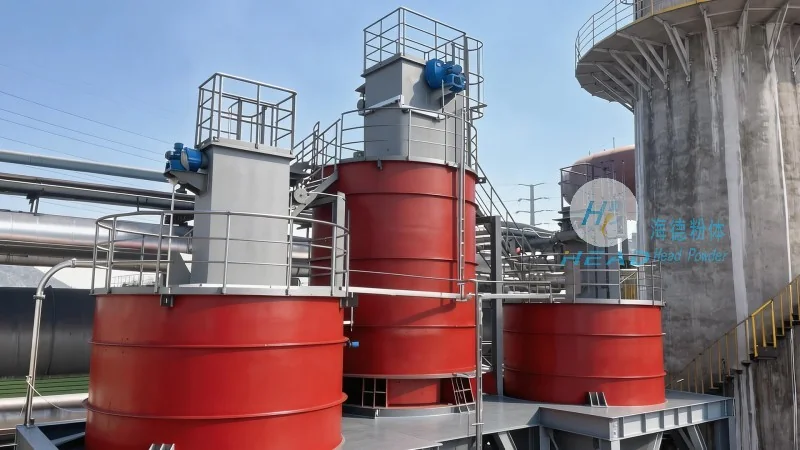
Pressure systems, on the other hand, use positive pressure to push the powder through the conveying line. These systems are commonly used when the material needs to be transported to a higher elevation or over longer distances. They are often preferred for applications involving high-volume material transport, as they can handle larger quantities with less energy consumption compared to suction systems. Pressure systems typically consist of a blower or compressor, a material feeder, and a pressure vessel to maintain the required pressure. The design of pressure systems must consider factors such as material flow rate, pipeline length, and the need for pressure relief valves to prevent over-pressurization.
Regardless of the system type, calcium carbonate powder pneumatic conveying systems share several critical components that ensure reliable operation. These components work in concert to control the flow of material, maintain system pressure, and protect the equipment from damage.
The material hopper is the primary storage unit for calcium carbonate powder. It is designed to hold the bulk material and feed it into the conveying system at a controlled rate. The hopper typically includes a discharge valve or a rotary valve to regulate the flow of powder. For calcium carbonate, which can be prone to caking or bridging, the hopper may be equipped with agitators or vibrators to prevent material buildup. The feeder is responsible for delivering the powder from the hopper to the conveying line, ensuring a consistent and uniform flow. Shandong HeadPowder Engineering Co., Ltd. specializes in designing hoppers and feeders that are tailored to the specific characteristics of calcium carbonate, such as particle size distribution and moisture content.
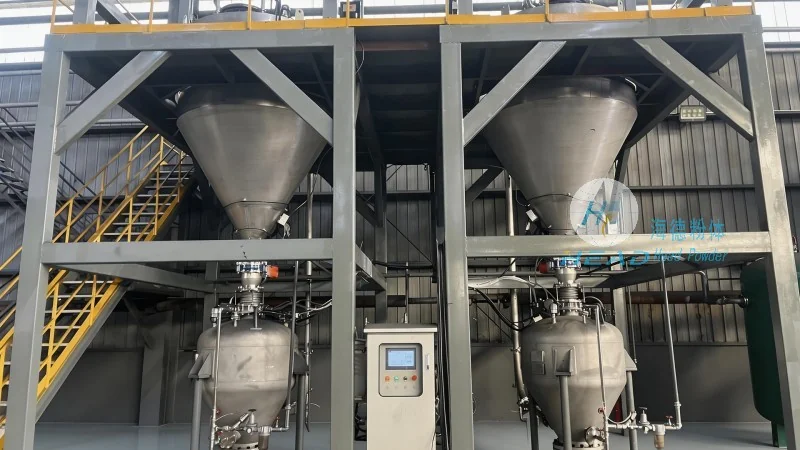
The pneumatic conveying unit is the heart of the system, providing the necessary air or gas to move the powder. The choice between a blower and a compressor depends on the system pressure requirements. Blowers are used for suction systems and operate at lower pressures, while compressors are used for pressure systems and can generate higher pressures. The unit must be capable of delivering sufficient airflow to overcome the resistance in the pipeline and lift the powder to the desired height. For calcium carbonate powder, which has a relatively low bulk density, a high airflow rate is often required to maintain a stable flow. Shandong HeadPowder Engineering Co., Ltd. offers a range of blower and compressor options, including centrifugal and positive displacement types, to meet the specific needs of each application.
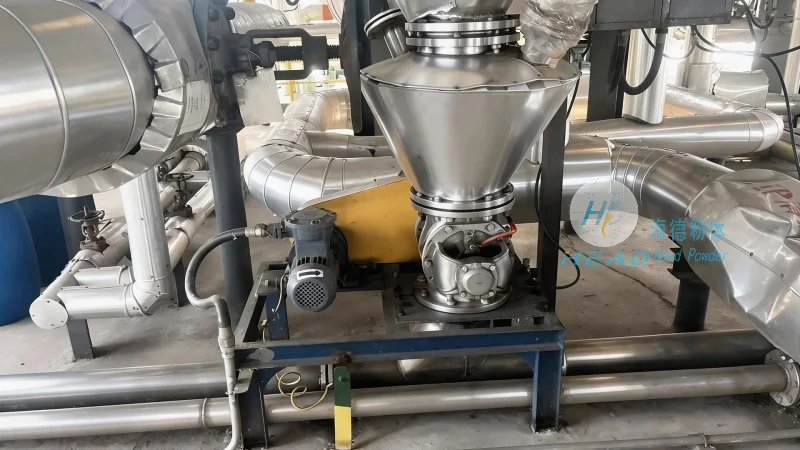
The pipeline is the conduit through which the calcium carbonate powder and air travel. It is typically made of stainless steel or other corrosion-resistant materials to prevent contamination and ensure durability. The pipeline design must consider factors such as the length of the conveying distance, the elevation changes, and the required flow rate. Fittings such as elbows, tees, and reducers are used to direct the flow and maintain the system's integrity. For long-distance or high-elevation conveying, the pipeline may include expansion joints or flexible connectors to accommodate thermal expansion and movement. The selection of pipeline diameter and material is critical to minimize pressure drop and energy consumption. Shandong HeadPowder Engineering Co., Ltd. provides customized pipeline solutions, including the use of flexible hoses for suction systems and rigid pipes for pressure systems, to optimize performance and reduce maintenance costs.
At the discharge end of the pneumatic conveying system, a separation and filtration unit is necessary to separate the powder from the air and collect the material for further processing. The separation system typically includes a cyclone separator, which uses centrifugal force to separate the powder from the air, and a bag filter or cartridge filter to capture any remaining fines. The collected powder is then discharged into a receiving container, while the clean air is vented to the atmosphere. For calcium carbonate powder, which may contain moisture or other contaminants, the filtration system must be designed to prevent clogging and ensure efficient collection. Shandong HeadPowder Engineering Co., Ltd. integrates advanced separation technologies, such as multi-cyclone separators and high-efficiency particulate air (HEPA) filters, to achieve high collection efficiency and maintain product quality.
Modern calcium carbonate powder pneumatic conveying systems are equipped with control and monitoring systems to ensure safe and efficient operation. These systems include sensors for pressure, flow rate, and level, as well as control panels to regulate the operation of the feeder, blower, and other components. The control system may also include alarms and safety interlocks to prevent over-pressurization, material blockages, or other hazards. For applications involving calcium carbonate, which can be sensitive to temperature and moisture, the monitoring system may include temperature sensors and humidity controls to maintain optimal conditions. Shandong HeadPowder Engineering Co., Ltd. offers comprehensive control solutions, including programmable logic controllers (PLCs) and human-machine interfaces (HMIs), to provide real-time monitoring and automated operation of the system.
The successful implementation of a calcium carbonate powder pneumatic conveying system depends on several factors, including the material properties, operational requirements, and environmental regulations. Shandong HeadPowder Engineering Co., Ltd. takes a customized approach to system design, ensuring that each solution is tailored to the specific needs of the client.
Calcium carbonate powder has distinct properties that affect the design of the pneumatic conveying system. The particle size distribution, bulk density, and moisture content of the powder influence the flow characteristics and the required airflow rate. For example, finer particles may require higher airflow to maintain a stable suspension, while higher moisture content can lead to caking and blockages. Shandong HeadPowder Engineering Co., Ltd. conducts thorough material testing to determine the optimal system parameters and select the appropriate components.
The operational requirements of the system, such as the conveying distance, elevation change, and material flow rate, also play a crucial role in system design. Longer conveying distances or higher elevations may require higher pressure or larger pipeline diameters. The system must also be able to handle variations in material feed rate, such as during start-up or shutdown. Shandong HeadPowder Engineering Co., Ltd. works closely with clients to understand their operational needs and design systems that meet or exceed their performance expectations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top