Cement production heavily relies on the efficient and reliable transport of raw materials in powder form. This process is critical for maintaining consistent quality and optimizing production efficiency. The systems used for conveying these materials, such as cement raw materials, are designed to handle the unique challenges of powder handling, including dust control, material flow management, and system durability. In this overview, we will explore the key components, structural design, and operational principles of cement raw material powder conveying systems, highlighting the importance of each element in ensuring smooth and effective material transport.
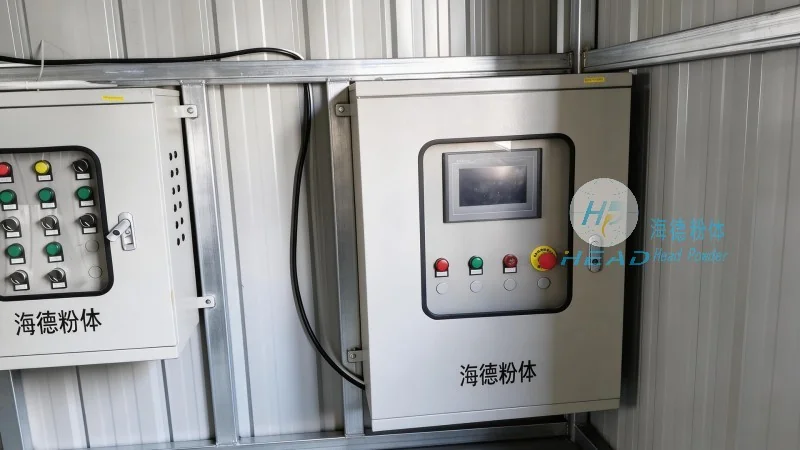
At the core of any cement raw material powder conveying system are several essential components that work in tandem to achieve efficient material transport. These components include feeders, conveyors, and control systems, each playing a vital role in the overall operation. Feeders are responsible for regulating the flow of raw materials from storage silos or hoppers into the conveying system, ensuring a consistent and controlled feed rate. This is crucial for preventing material buildup or uneven flow, which can lead to system inefficiencies or equipment damage. Conveyors, such as pneumatic or mechanical systems, then transport the powder through the pipeline network. Pneumatic conveyors use air pressure to move materials, while mechanical conveyors rely on belts, screws, or other mechanisms. The choice of conveyor type depends on factors like material properties, distance, and system capacity. Control systems, including sensors and automation equipment, monitor and adjust the flow rate, pressure, and other parameters to maintain optimal performance. These components are typically integrated into a comprehensive system that ensures seamless material handling from source to destination.
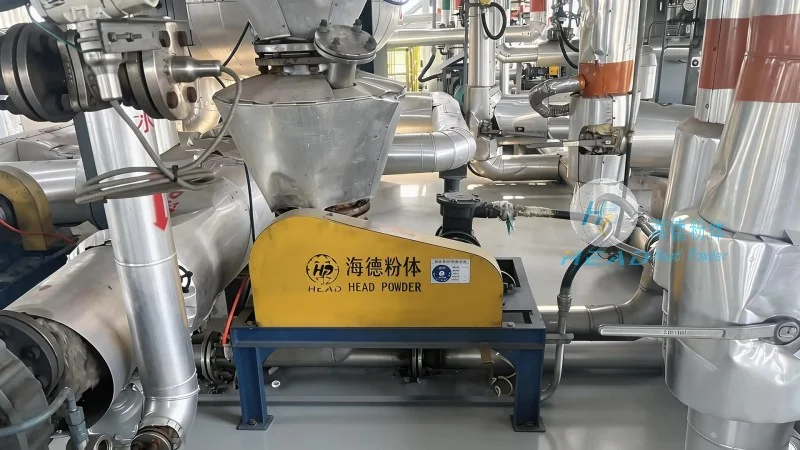
The operational principle of cement raw material powder conveying systems is based on the physics of powder flow and the mechanics of material transport. The system operates by creating a flow of material through the pipeline, often using air or mechanical force. In pneumatic conveying, for example, a fan or blower generates air pressure that propels the powder particles forward. The velocity of the air and the size of the particles determine the efficiency of the conveying process. Proper design of the pipeline, including the use of appropriate pipe diameters and bends, is essential to minimize pressure losses and ensure smooth flow. Mechanical conveyors, such as screw conveyors, use rotating screws to push the material along the tube. This method is particularly effective for handling cohesive or sticky materials, as the screw provides continuous movement and prevents material stagnation. The control system plays a critical role in maintaining the desired flow rate and pressure, adjusting parameters in real-time based on sensor feedback. This ensures that the system operates within optimal conditions, preventing overloading or under-conveying, which can impact production output and material quality.
The design and maintenance of cement raw material powder conveying systems are critical factors that directly impact their performance and longevity. Proper system design involves considering the characteristics of the raw materials, such as particle size, moisture content, and flowability, to select the most suitable conveying method and equipment. For example, materials with high moisture content may require additional drying or conditioning steps to prevent clogging or corrosion in the system. The structural design of the pipeline, including the use of corrosion-resistant materials and proper sealing, is also essential to ensure long-term reliability. Regular maintenance, including cleaning, lubrication, and inspection of components, is necessary to prevent wear and tear and maintain system efficiency. HeadPowder, a leading provider of engineering solutions for cement and other industries, specializes in designing and manufacturing high-quality powder conveying systems tailored to the specific needs of clients. With a focus on durability, efficiency, and reliability, HeadPowder's systems are built to withstand the demanding conditions of cement production and ensure consistent performance over extended periods.
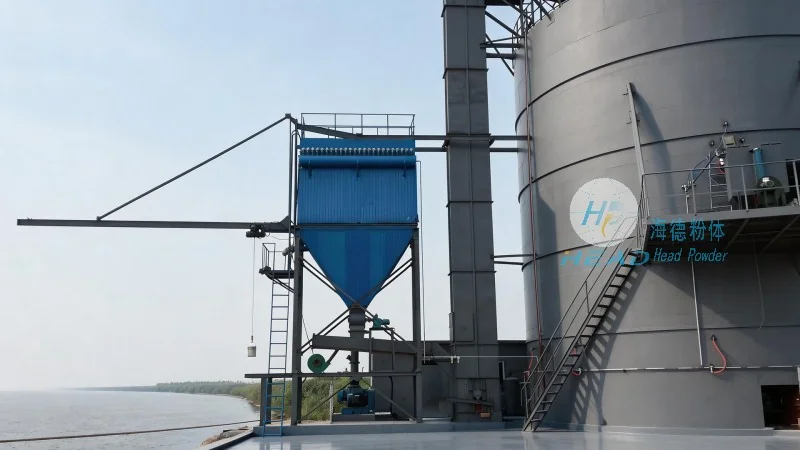
Cement raw material powder conveying systems are widely used in various stages of cement production, from raw material handling to clinker processing. The efficient transport of raw materials like limestone, clay, and iron ore is essential for maintaining the quality of the final cement product. By ensuring a consistent and controlled supply of raw materials, these systems help to optimize the grinding process and reduce energy consumption. The benefits of using advanced powder conveying systems include improved production efficiency, reduced downtime, and enhanced material quality. Additionally, these systems contribute to better safety and environmental performance by minimizing dust emissions and controlling material handling processes. HeadPowder's expertise in powder handling technology allows them to provide customized solutions that address the unique challenges of each client's operation, ensuring that the conveying system is optimized for their specific production requirements.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top