Understanding the efficient and reliable transport of corn kernels as a powder is crucial in various industrial applications, from food processing to agricultural storage. This article provides a comprehensive overview of the mechanisms, structural components, and operational principles that underpin modern corn kernels powder conveying systems, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in designing and manufacturing advanced solutions tailored to meet industry demands.
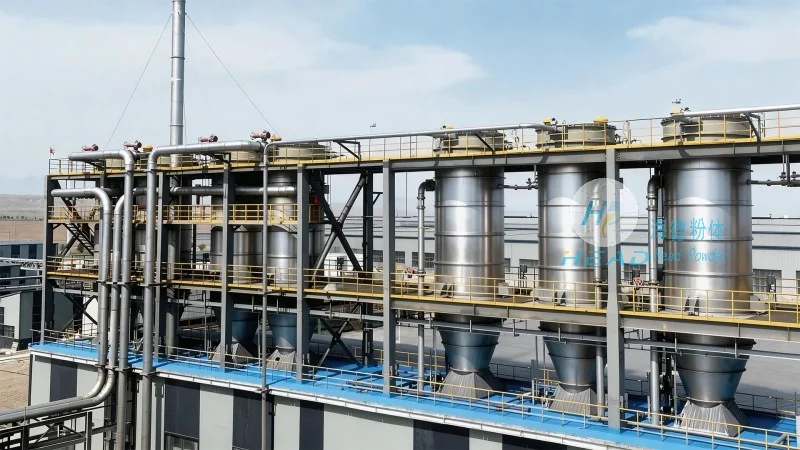
The core of any corn kernels powder conveying system lies in its integrated structural design, which ensures optimal performance, durability, and safety. Key components typically include: the hopper or feed inlet, which serves as the entry point for corn kernels; the conveyor mechanism, such as screw conveyors or pneumatic systems, responsible for transporting the material; and the discharge outlet, facilitating the smooth release of the conveyed powder. Each component is engineered to withstand the mechanical stresses and environmental conditions associated with handling corn kernels, ensuring consistent and efficient operation.
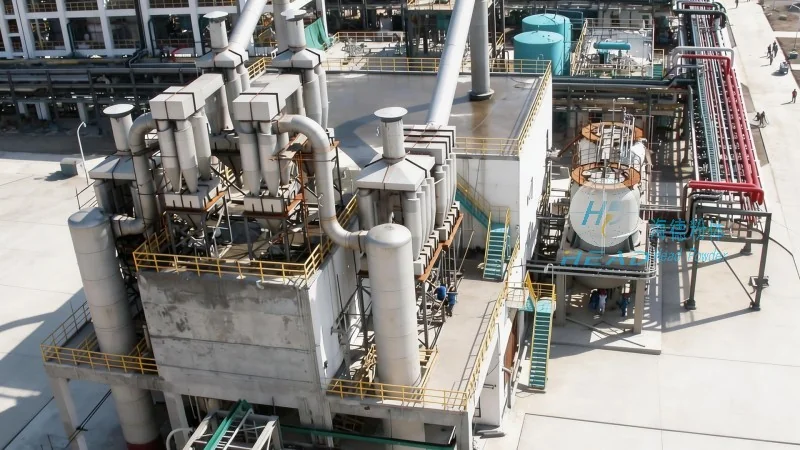
The operational principle of corn kernels powder conveying systems revolves around the movement of material through a controlled environment. For mechanical conveyors like screw conveyors, the rotating screw (or auger) creates a continuous flow by pushing the corn kernels forward, leveraging the friction between the material and the screw surface. In pneumatic conveying systems, air pressure is used to create a flow, where the corn kernels are suspended in a stream of air and transported through pipelines. Both methods are designed to maintain the integrity of the corn kernels, preventing breakage or degradation, while ensuring high throughput rates. The system’s design also incorporates features like variable speed controls and material flow monitoring to adapt to different processing requirements, enhancing overall efficiency.
Corn kernels powder conveying systems are widely used in industries such as food processing, where they facilitate the transport of raw materials for milling, grinding, or packaging. In agricultural storage, these systems help in moving corn kernels from storage facilities to processing plants, ensuring smooth supply chains. The adaptability of the systems to handle varying particle sizes and moisture content makes them suitable for diverse applications, from small-scale operations to large industrial facilities. Shandong HeadPowder Engineering Co., Ltd. specializes in customizing these systems to meet specific client needs, providing solutions that enhance productivity and reduce operational costs.
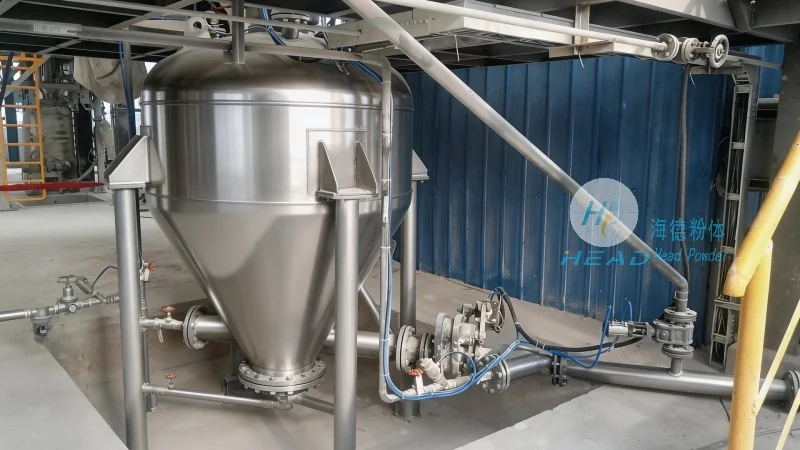
Modern corn kernels powder conveying systems offer several advantages over traditional methods. These include improved energy efficiency, reduced labor costs, and enhanced safety features. The use of advanced materials and manufacturing techniques ensures longer service life and lower maintenance requirements. Additionally, the systems are designed to minimize dust generation and environmental impact, aligning with industry standards for sustainability. By integrating automation and control systems, these solutions enable real-time monitoring and adjustment, optimizing performance and reducing downtime. The expertise of Shandong HeadPowder Engineering Co., Ltd. in this field allows them to deliver high-quality, reliable systems that meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top