HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and application of equipment for transporting and processing bentonite powder. This article provides an overview of bentonite powder conveying systems, focusing on their structural design and operational principles. The company, based in Shandong, China, leverages decades of industry experience to deliver efficient and reliable solutions tailored to the unique challenges of bentonite powder handling.
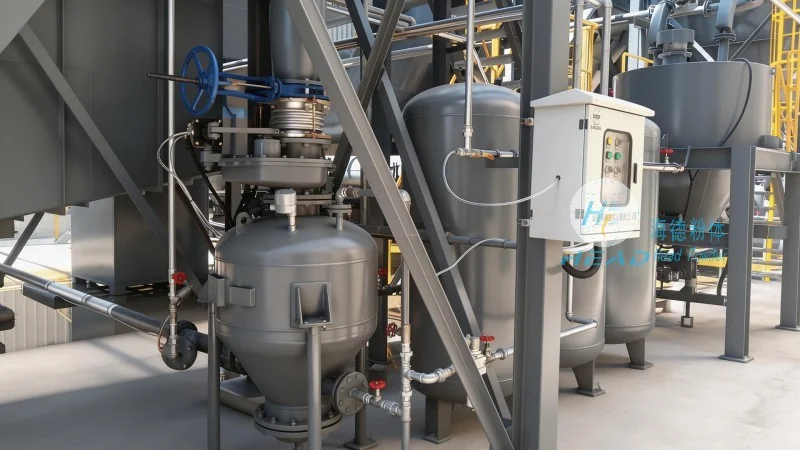
Bentonite is a natural clay mineral composed primarily of montmorillonite, known for its high swelling capacity and excellent thixotropic properties. These characteristics make bentonite a critical material in various industries, including drilling fluids, foundry casting, and environmental remediation. However, the unique physical properties of bentonite—such as its fine particle size, cohesive nature, and tendency to agglomerate—pose significant challenges during powder handling. Traditional conveying methods often struggle with issues like blockages, dust generation, and material degradation. To address these challenges, specialized conveying systems have been developed to ensure safe, efficient, and consistent transport of bentonite powder.
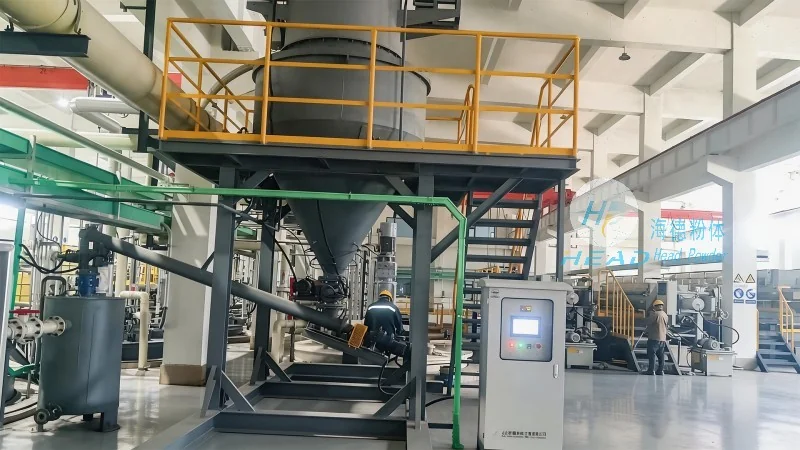
The core of bentonite powder conveying systems lies in their robust structural design, which is engineered to accommodate the material's specific characteristics. Key components typically include a hopper for material storage, a feeder to control the flow rate, a conveyor (often a screw or pneumatic system), and a dust collection system. The hopper is designed with a wide, sloped bottom to prevent material bridging and ensure smooth discharge. The feeder, such as a rotary valve or a variable-speed screw feeder, regulates the flow of bentonite into the conveyor, preventing overloading and maintaining consistent feed rates. The conveyor itself is constructed from materials resistant to corrosion and abrasion, such as stainless steel or high-grade plastics, to withstand the abrasive nature of bentonite particles. Additionally, the system incorporates a dust suppression and collection mechanism to minimize airborne dust, which is essential for maintaining a safe and clean working environment.
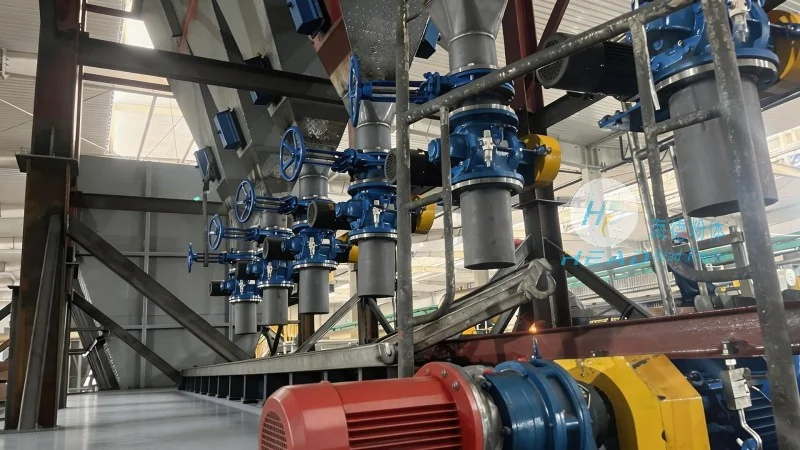
The operational principles of bentonite powder conveying systems are centered on maintaining a consistent flow of material while minimizing the risk of blockages or equipment damage. The system operates by first feeding bentonite from the hopper into the feeder, which then controls the flow rate based on the process requirements. The conveyor transports the material to the discharge point, where it is either stored or transferred to the next processing stage. A critical aspect of the system's operation is the control of moisture content and particle size distribution. Bentonite's thixotropic properties mean that its flow behavior changes with shear rate and time, so the conveying system must be designed to maintain a stable shear environment to prevent agglomeration. The use of variable-speed feeders and adjustable conveyor speeds allows operators to optimize the flow rate, ensuring that the material moves smoothly without causing excessive wear on the equipment. Furthermore, the system includes monitoring and control features, such as pressure sensors and flow meters, to detect any deviations in performance and alert operators to potential issues before they escalate.
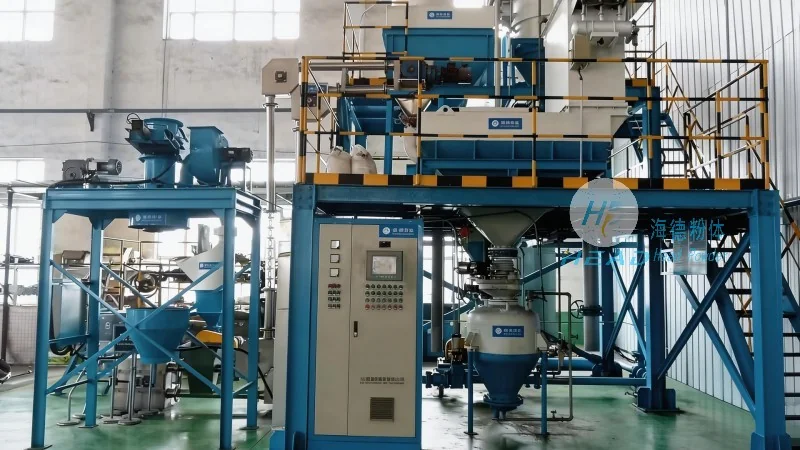
Bentonite powder conveying systems are widely used in industries where the consistent and reliable transport of bentonite is essential. In the oil and gas industry, bentonite is used to formulate drilling fluids, and the conveying system ensures that the correct amount of bentonite is added to the fluid mix without causing contamination or equipment damage. In foundry casting, bentonite is used as a mold material, and the system provides a clean and efficient way to transport the powder to the casting process. In environmental applications, bentonite is used for soil stabilization and remediation, and the conveying system ensures that the material is applied uniformly and safely. The benefits of using specialized bentonite powder conveying systems include improved process efficiency, reduced downtime due to equipment failures, lower maintenance costs, and enhanced safety through dust suppression. By addressing the unique challenges of bentonite handling, these systems enable industries to maximize productivity while minimizing operational risks.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top