Bulk bag packing systems are essential in industries dealing with bulk powders, offering efficient and cost-effective solutions for material handling. These systems are designed to handle large quantities of powders, such as chemicals, food products, and industrial materials, ensuring safe and reliable transport and storage. The core of these systems lies in the integration of bulk bag filling, sealing, and discharge mechanisms, which work together to streamline the entire powder handling process.
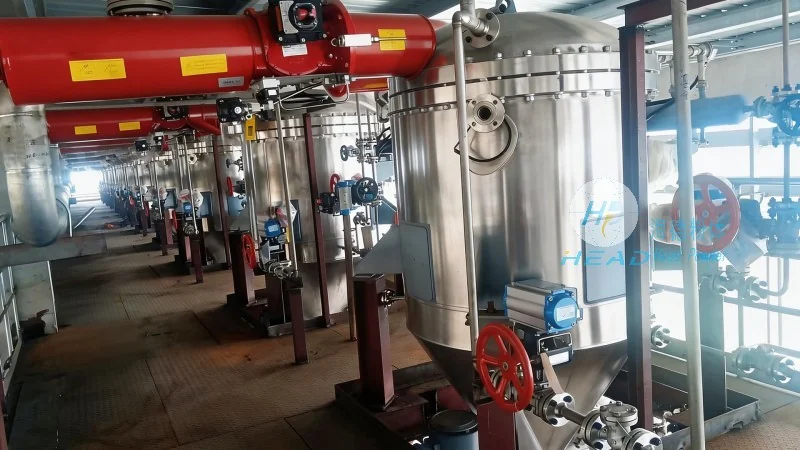
HeadPowder, a leading manufacturer in the field of bulk material handling equipment, specializes in providing high-quality bulk bag packing solutions. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for businesses seeking reliable and efficient powder handling systems. HeadPowder's expertise spans across various industries, including chemical, food, pharmaceutical, and agricultural sectors, catering to diverse material handling needs.
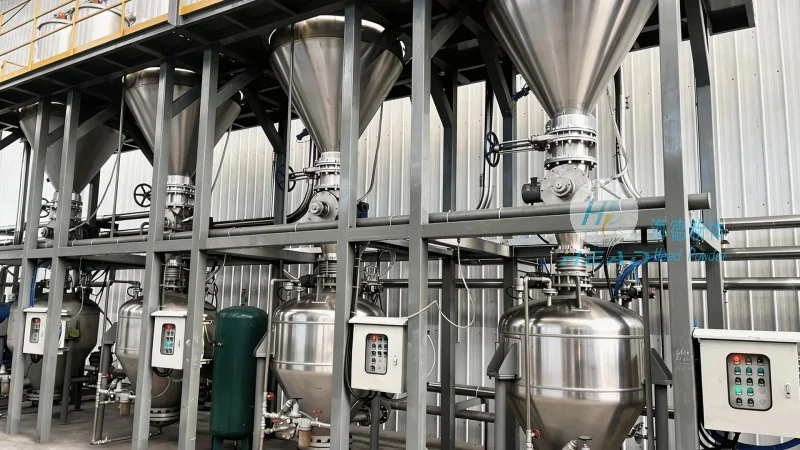
The bulk bag packing system consists of several key components that work in tandem to ensure optimal performance. The primary components include a bulk bag filler, a discharge valve, a frame or support structure, and a control system. The filler is responsible for accurately measuring and dispensing the powder into the bulk bag, while the discharge valve allows for controlled release of the material when needed. The frame provides stability and support to the bulk bag during the filling and handling process. The control system manages the entire operation, ensuring precision and safety throughout.
Bulk bag packing systems significantly improve material handling efficiency by reducing manual labor and minimizing material loss. Traditional methods of handling bulk powders often involve manual scooping or bagging, which are time-consuming and prone to errors. In contrast, automated bulk bag packing systems enable high-speed filling, reducing processing time and increasing throughput. Additionally, these systems help maintain consistent material quality by preventing contamination and ensuring accurate dosing. The use of bulk bags also reduces packaging costs compared to traditional containers, making it a cost-effective solution for bulk material transport.
Bulk bag packing systems are widely used across various industries due to their versatility and efficiency. In the chemical industry, these systems are used for handling raw materials and finished products, ensuring safe and controlled transport. The food and beverage industry relies on bulk bag packing for ingredients like flour, sugar, and spices, maintaining hygiene and quality standards. The pharmaceutical industry uses these systems for handling active pharmaceutical ingredients (APIs) and other sensitive materials, where precision and sterility are critical. Agricultural industries also benefit from bulk bag packing for storing and transporting fertilizers and seeds, ensuring efficient distribution and use.
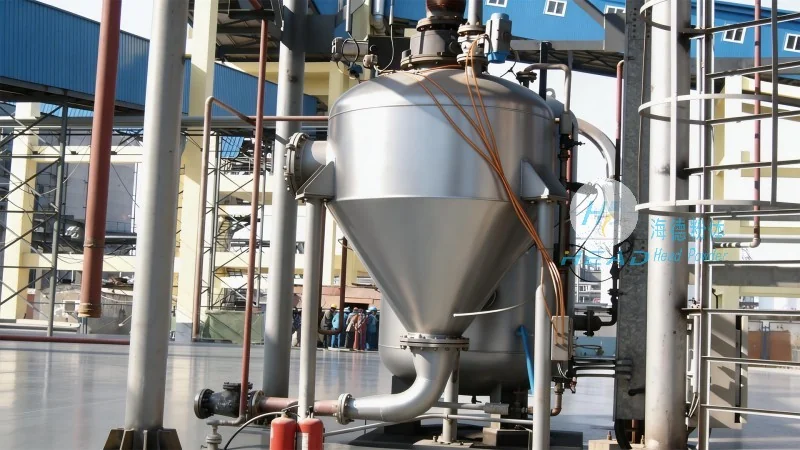
There are several advantages to implementing bulk bag packing systems in material handling operations. Firstly, they offer high capacity, allowing for the handling of large quantities of powders in a single operation. This reduces the number of handling steps and improves overall efficiency. Secondly, bulk bags are lightweight and easy to handle, making them suitable for both indoor and outdoor applications. They also provide excellent protection against moisture and contamination, preserving the quality of the material. Another advantage is the cost-effectiveness of bulk bag packing, as it reduces packaging and transportation costs compared to smaller containers. Furthermore, these systems are flexible and can be customized to meet specific material handling requirements, ensuring optimal performance for different applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top