HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced cement raw material pneumatic conveying systems. This equipment is essential for the efficient transport of raw materials in cement production lines, ensuring smooth and reliable material handling from storage to processing units.
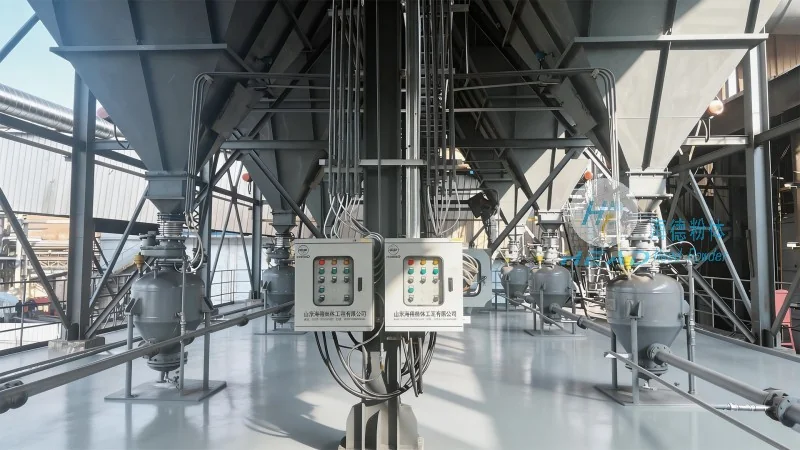
The cement raw material pneumatic conveying equipment, as offered by Shandong HeadPowder Engineering Co., Ltd., is engineered to handle the transportation of bulk materials such as limestone, clay, and iron ore. These raw materials are crucial for the production of cement, and the efficient conveyance directly impacts the overall productivity and quality of the final product. The system operates by using compressed air to create a flow that propels the material through a pipeline network, eliminating the need for mechanical components like belts or buckets in traditional conveying methods. By leveraging pneumatic technology, the equipment provides a dust-free and low-maintenance solution that enhances operational efficiency in cement manufacturing.
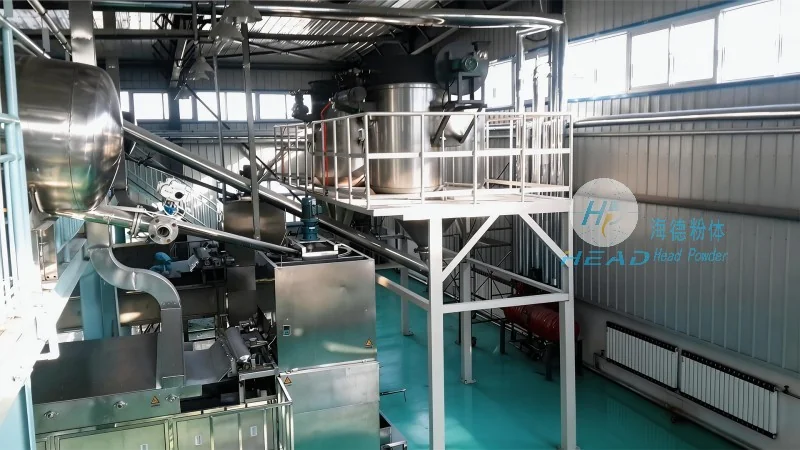
The core structure of the pneumatic conveying system consists of several key components that work in tandem to ensure effective material transport. The primary elements include the material feed hopper, the air compressor, the conveying pipeline, and the material discharge unit. The process begins with the raw material being fed into the hopper, where it is then mixed with the compressed air from the compressor. As the air and material mixture enters the pipeline, the air velocity is sufficient to keep the material suspended and transported to the destination. The system utilizes either positive pressure or negative pressure (or a combination of both) depending on the specific application and material characteristics. For instance, positive pressure systems are commonly used for long-distance or high-capacity conveying, as they can maintain consistent air pressure along the entire pipeline. Negative pressure systems, on the other hand, are suitable for short-distance or dusty applications, as they create a vacuum that draws the material into the pipeline. The choice between these systems depends on factors such as the distance between the feed and discharge points, the material's density and particle size, and the plant's layout.
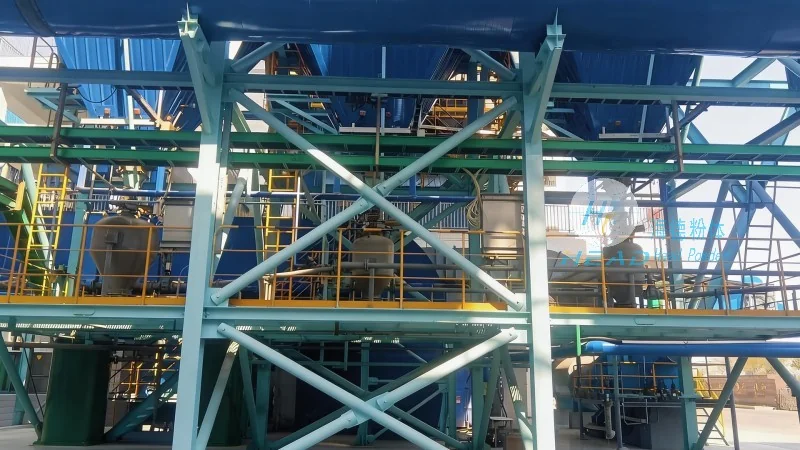
Implementing the cement raw material pneumatic conveying equipment from HeadPowder brings several significant advantages to cement production facilities. Firstly, it enhances operational efficiency by reducing downtime and labor costs associated with manual material handling. The automated system ensures consistent material flow, minimizing variations in feed rates that can affect the quality of the cement clinker. Secondly, the equipment improves safety by eliminating the need for workers to handle heavy or dusty materials manually, thereby reducing the risk of occupational hazards like dust inhalation or material handling injuries. Additionally, the system offers flexibility in terms of layout, as the pipelines can be installed in various configurations to accommodate different plant layouts and production requirements. This adaptability allows for easier integration into existing production lines without major structural modifications, making it a cost-effective solution for both new and retrofit projects.
HeadPowder provides a range of technical specifications and customization options to meet the diverse needs of cement manufacturers. The equipment is available in different pressure ratings, from low to high, to suit various conveying distances and material types. The pipeline diameter and length can be tailored to the specific requirements of the plant, ensuring optimal performance. The company also offers accessories such as filters, cyclones, and material separators to enhance the system's functionality and maintain material quality. These components help in preventing dust accumulation and ensuring that the conveyed material remains clean and free from contaminants. Furthermore, the system can be equipped with monitoring and control systems that allow operators to track the flow rate, pressure, and temperature in real-time, enabling proactive maintenance and troubleshooting. This feature helps in identifying potential issues before they lead to system failures, thereby reducing maintenance costs and increasing the equipment's lifespan.
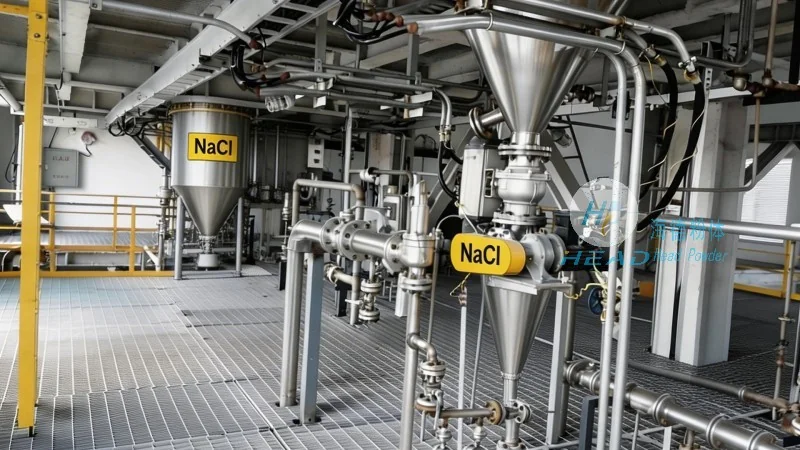
The cement raw material pneumatic conveying equipment plays a critical role in the overall cement production process. It is typically integrated into the raw material preparation stage, where the bulk raw materials are transported from storage silos to the raw mill for grinding. The efficient conveyance of these materials ensures that the raw mill operates at optimal capacity, reducing the time required for material processing and minimizing energy consumption. The system also contributes to the stability of the production line by providing a consistent feed rate, which is essential for maintaining the quality of the cement clinker. In addition, the equipment helps in reducing energy consumption by minimizing the need for mechanical conveying systems that often require more power and maintenance. By leveraging the pneumatic conveying technology, cement plants can achieve higher productivity and lower operational costs, making it a preferred choice for modern cement production facilities. The equipment's ability to handle various raw materials and its adaptability to different plant layouts make it a versatile solution for cement manufacturers looking to optimize their production processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top