The tonne bag quantitative feeding pneumatic conveying system is a specialized industrial equipment designed for efficient and precise material handling. This system is particularly suited for applications involving bulk materials, where accurate and controlled feeding is crucial. The system integrates advanced pneumatic conveying technology with precise dosing mechanisms, ensuring optimal performance in various industrial settings. By leveraging the principles of air-based material transport, it offers a reliable solution for transporting and feeding materials from bulk storage containers, such as tonne bags, into processing equipment.
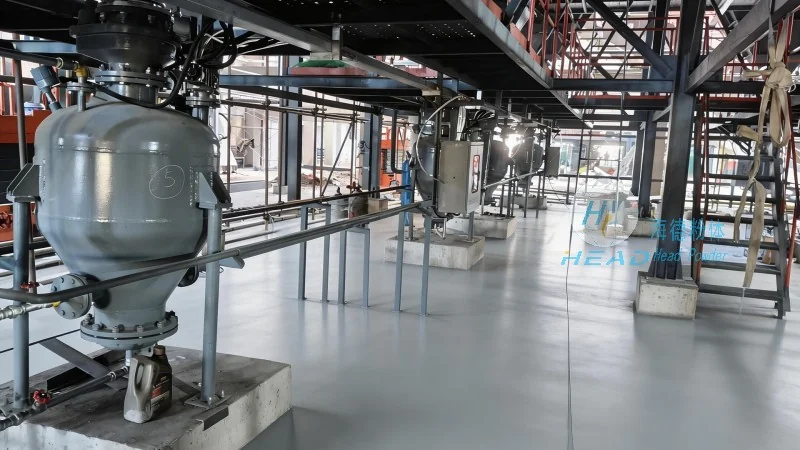
The tonne bag quantitative feeding pneumatic conveying system comprises several critical components that work in tandem to achieve its operational objectives. The primary components include the hopper, the pneumatic conveying pipeline, the rotary valve or feeder, the air compressor, and the control system. The hopper is responsible for receiving and storing the material from the tonne bag, providing a stable feed source. The pneumatic conveying pipeline transports the material from the hopper to the processing unit using compressed air. The rotary valve or feeder regulates the flow rate of the material, ensuring precise dosing. The air compressor generates the necessary air pressure to drive the material through the pipeline. The control system monitors and adjusts the operation of the system, maintaining consistent performance.
The operation of the tonne bag quantitative feeding pneumatic conveying system is based on the principle of pneumatic transport, where materials are conveyed through a pipeline using air as the conveying medium. The process begins with the material being discharged from the tonne bag into the hopper. The air compressor then generates compressed air, which is introduced into the conveying pipeline. As the air flows through the pipeline, it creates a pressure differential that propels the material particles forward. The rotary valve or feeder controls the rate at which material is released from the hopper into the pipeline, ensuring that the material is conveyed at a controlled and consistent rate. The material travels through the pipeline and is discharged into the processing equipment, where it is further processed or utilized. The control system continuously monitors the pressure, flow rate, and material level, adjusting the operation as needed to maintain optimal performance.
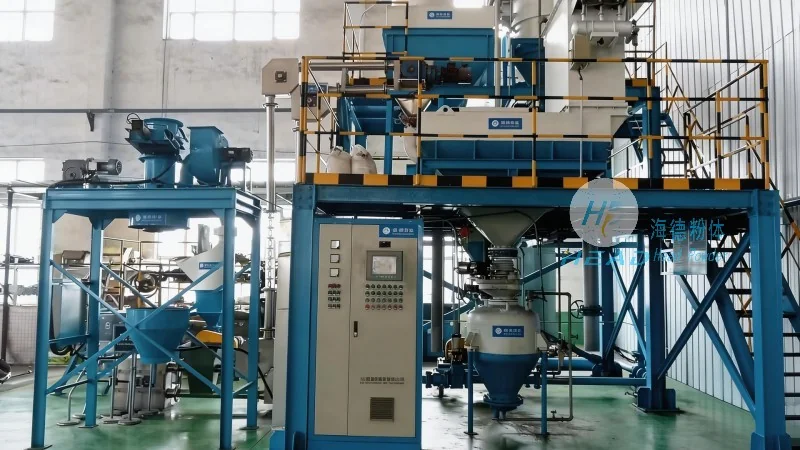
Implementing a tonne bag quantitative feeding pneumatic conveying system offers several advantages over traditional material handling methods. Firstly, it provides high accuracy in material dosing, minimizing waste and ensuring consistent product quality. The precise control of the feeding rate allows for better process control and reduces the risk of overfeeding or underfeeding. Secondly, the system is highly efficient, as it eliminates the need for manual handling of bulk materials, reducing labor costs and improving safety. The pneumatic conveying process is also faster and more reliable compared to mechanical conveyors, which can be prone to blockages and maintenance issues. Additionally, the system is versatile and can handle a wide range of materials, including powders, granules, and fine particles. It is also suitable for applications that require dust-free and hygienic handling, making it ideal for industries such as food, pharmaceuticals, and chemicals.
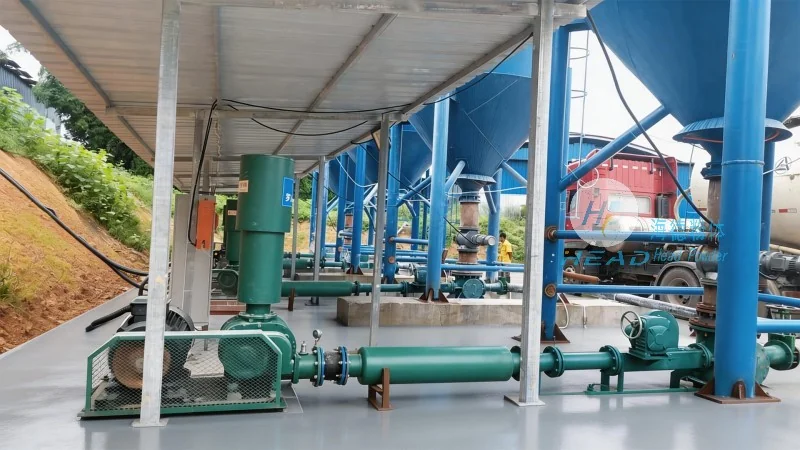
The tonne bag quantitative feeding pneumatic conveying system is widely used in various industries that require bulk material handling and precise feeding. Some common applications include the food and beverage industry, where it is used for handling ingredients like flour, sugar, and spices. In the pharmaceutical industry, it is used for conveying raw materials and active pharmaceutical ingredients (APIs) with high precision and hygiene. The chemical industry also utilizes this system for handling various chemicals, including powders and granules. Additionally, it is used in the agricultural sector for handling fertilizers and other agricultural products. The system is also suitable for industrial applications such as cement, minerals, and construction materials, where accurate dosing is essential for quality control.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of industrial material handling equipment, specializing in pneumatic conveying systems. The company is headquartered in Shandong, China, and has a strong reputation for providing high-quality, reliable, and efficient solutions for material handling needs. With years of experience in the industry, HeadPowder has developed a comprehensive range of products that cater to various industrial applications. The company focuses on innovation and technology, continuously improving its products to meet the evolving needs of its customers. HeadPowder's commitment to quality and customer satisfaction has made it a trusted partner for many industries worldwide. The company's products are designed to be durable, easy to maintain, and cost-effective, providing long-term value to its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top