Unattended feeding pneumatic conveying systems represent a sophisticated solution in material handling, designed to operate autonomously without continuous human intervention. These systems are engineered to efficiently transport bulk materials from storage to processing points, leveraging pneumatic principles to achieve seamless material movement. The technology is particularly valuable in industrial settings where reliability, efficiency, and safety are paramount.
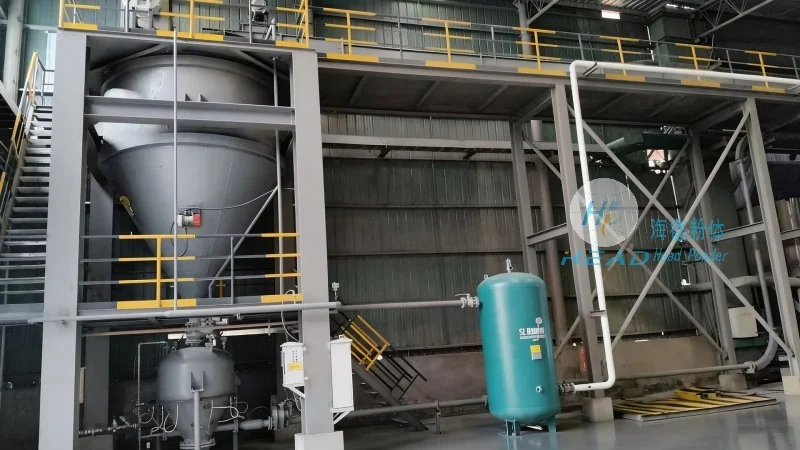
The core structure of an unattended feeding pneumatic conveying system comprises several integral components that work in concert to ensure optimal performance. At the heart of the system is the feeding unit, which typically includes a hopper or silo to store the bulk material. This storage vessel is equipped with a discharge mechanism, such as a rotary valve or a gate valve, that controls the flow of material into the conveying line. The feeding unit is connected to a pneumatic conveying line, which may consist of flexible hoses or rigid pipes, depending on the system design and material characteristics.
Within the conveying line, the material is propelled by a high-pressure air stream generated by a blower or a compressor. The air and material mixture travels through the pipeline, with the velocity and pressure maintained at levels sufficient to prevent material settling or blockage. The system may incorporate additional components like cyclones or filters to separate the material from the air stream, ensuring that the conveyed material reaches its destination in a clean and controlled manner. Additionally, the system includes control mechanisms, such as sensors and valves, that monitor and regulate the flow of material and air, enhancing operational stability and preventing system failures.
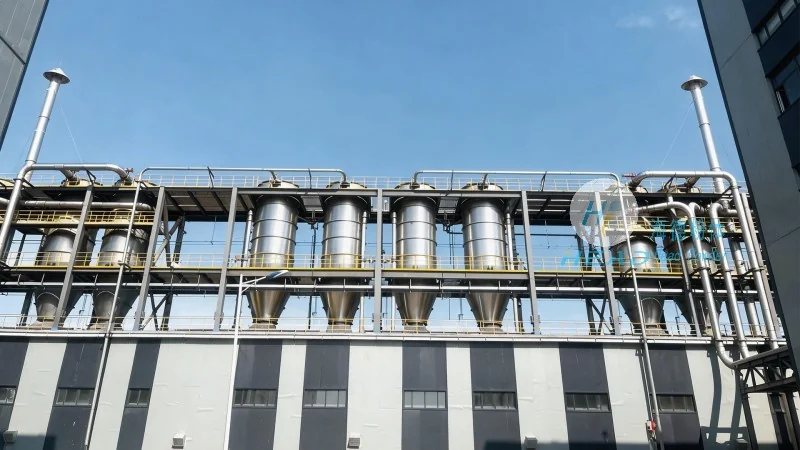
The operational principle of an unattended feeding pneumatic conveying system revolves around the use of compressed air to transport bulk materials. The process begins with the material being discharged from the storage hopper into the conveying line. As the material enters the line, it is entrained by the high-velocity air stream, forming a dense phase or dilute phase flow, depending on the system design and material properties. The air stream provides the necessary kinetic energy to move the material through the pipeline, overcoming gravitational and frictional forces that would otherwise impede movement.
In dilute phase systems, the material is suspended in the air stream as individual particles, allowing for high-velocity transport over longer distances. Conversely, dense phase systems use lower air velocities and higher material concentrations, which can be advantageous for handling materials that are prone to segregation or degradation. The system's control system continuously adjusts the air pressure and flow rate to maintain the desired conveying conditions, ensuring that the material is delivered to the target location without loss or degradation.
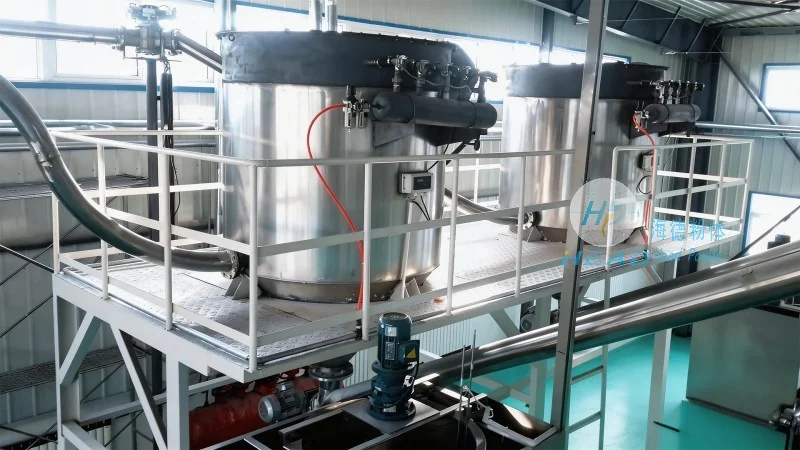
Unattended feeding pneumatic conveying systems offer several advantages that make them suitable for a wide range of industrial applications. One of the primary benefits is the ability to operate without human presence, reducing labor costs and minimizing the risk of workplace accidents. The systems are also highly flexible, as they can be configured to handle various materials, including powders, granules, and even fine particles. Additionally, the enclosed design of the system prevents dust emissions, enhancing workplace safety and compliance with environmental regulations.
These systems are commonly used in industries such as food processing, pharmaceuticals, chemicals, and minerals. For example, in the food industry, unattended feeding systems are employed to transport ingredients like flour, sugar, and spices from storage to production lines, ensuring consistent quality and hygiene. In the pharmaceutical sector, the enclosed and sterile design of the system is critical for maintaining product purity and preventing contamination. The reliability and efficiency of these systems make them an essential component in modern industrial operations.
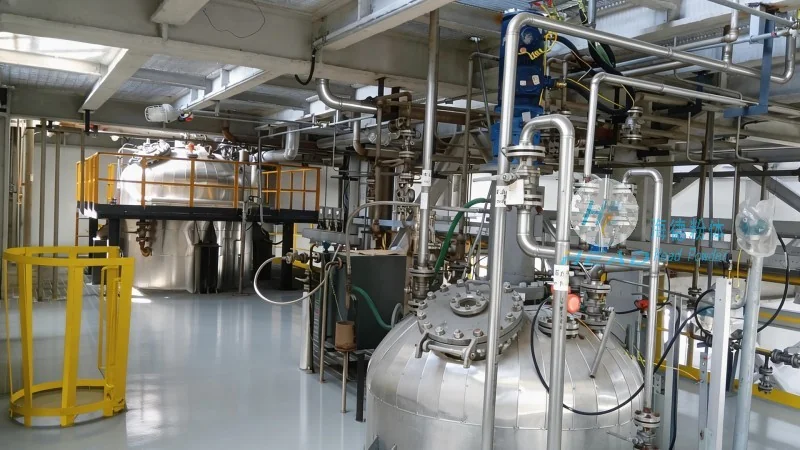
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of pneumatic conveying systems. The company is headquartered in Shandong, China, and specializes in designing, manufacturing, and installing customized unattended feeding solutions tailored to the specific needs of various industries. With a strong focus on innovation and quality, headpowder has established itself as a trusted partner for businesses seeking reliable material handling solutions.
Headpowder's team of engineers and technicians leverages advanced technology and extensive industry experience to develop cutting-edge pneumatic conveying systems. The company adheres to strict quality control standards, ensuring that all products meet or exceed industry specifications. By combining expertise in material science, mechanical engineering, and automation, headpowder delivers systems that are not only efficient but also durable and low-maintenance. The company's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including installation, training, and technical assistance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top