Maltose material handling equipment is essential for the efficient processing and transportation of maltose, a vital sugar component used across various food and beverage sectors. This equipment ensures safe, reliable, and consistent movement of maltose from storage to production lines, enhancing overall operational efficiency in industrial settings.
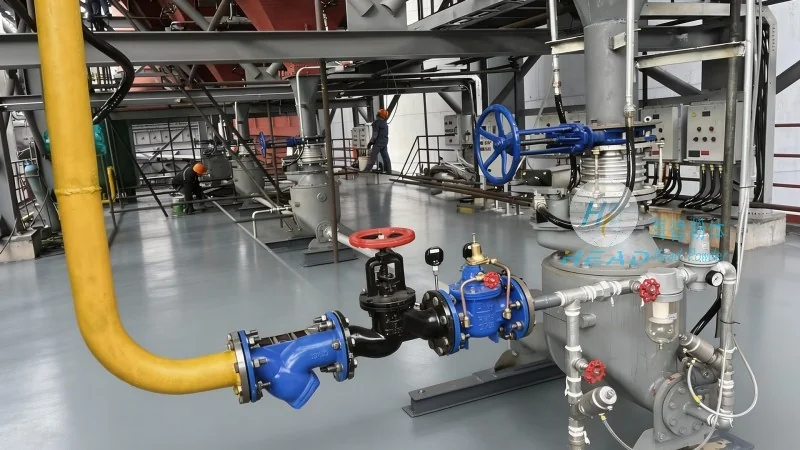
HeadPowder, a leading manufacturer based in Shandong, China, specializes in developing advanced maltose handling solutions. The company’s equipment is engineered to meet the specific demands of maltose processing, offering durability, precision, and compliance with industry standards. With a focus on innovation and customer-centric design, HeadPowder’s products are widely recognized for their performance and reliability in the maltose industry.
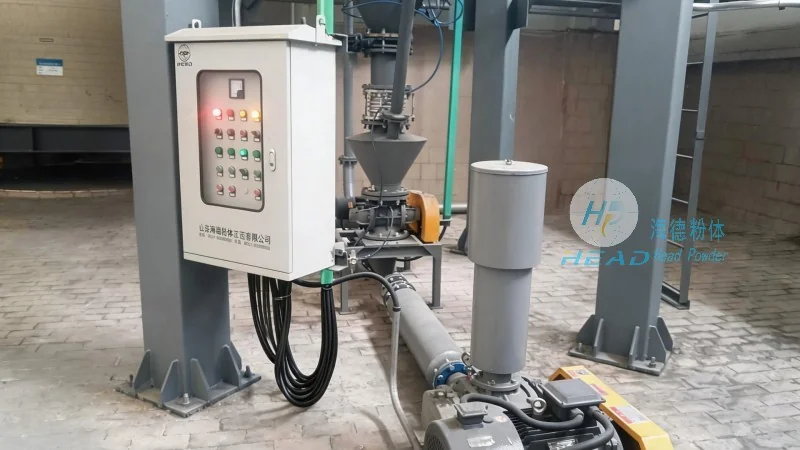
The maltose material handling equipment typically consists of several integrated components, including feed hoppers, conveyor systems, pumps, control panels, and safety mechanisms. The feed hopper receives maltose from storage silos or bulk containers, while the conveyor system—equipped with adjustable speed and direction controls—facilitates smooth material transfer. Pumps (centrifugal or positive displacement types) handle liquid maltose or dissolved solutions, ensuring consistent flow rates. The control panel integrates sensors, valves, and automated controls to monitor and regulate the entire process, enhancing operational safety and efficiency.
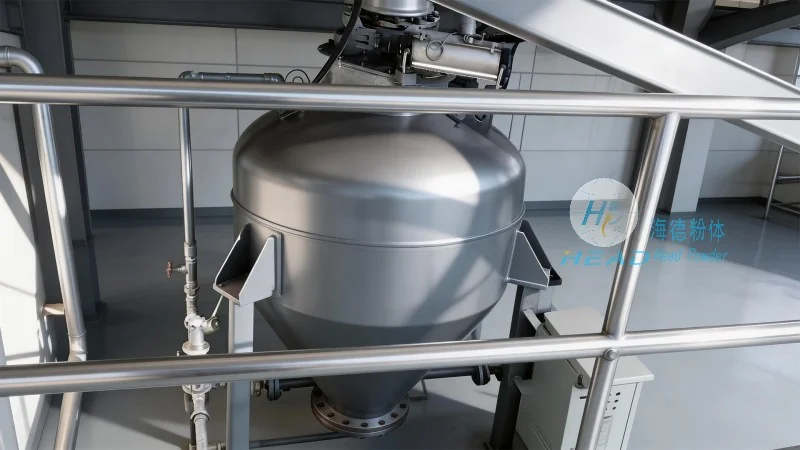
The operation process begins with loading maltose into the feed hopper. Once filled, the conveyor system activates, transporting the material to processing lines or storage tanks. For liquid maltose, pumps are engaged to move the solution through pipelines, with flow rates controlled by automation. The control panel continuously monitors parameters like pressure, temperature, and flow rate, adjusting performance as needed. Safety features—including emergency stop buttons and overload protection—prevent accidents and ensure personnel safety during operation.
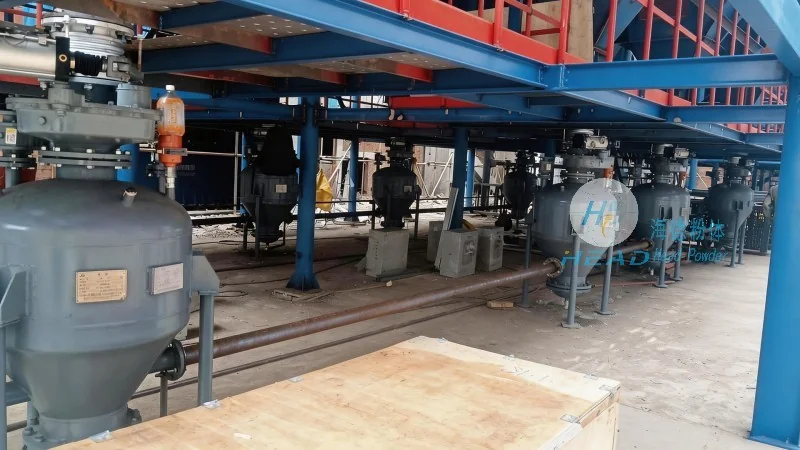
The working principle relies on mechanical and fluid dynamics. The conveyor system uses gravity or motor-driven mechanisms for solid maltose, while pumps employ centrifugal force or positive displacement for liquids. Sensors and feedback loops provide real-time data on material status, enabling precise control. This integrated approach minimizes loss, contamination, or degradation, maintaining product quality throughout transportation and processing.
HeadPowder’s equipment is widely used in the food and beverage industry for maltose-based products like syrups, beverages, and baked goods. It is also applicable in chemical and pharmaceutical sectors where maltose serves as a raw material or additive. Its versatility in handling both solid and liquid forms supports production lines requiring consistent material flow. By optimizing handling, the equipment reduces downtime, improves productivity, and enhances operational efficiency for manufacturers.
HeadPowder, officially known as Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer specializing in material handling equipment design and production. Headquartered in Shandong, China, the company has built a strong reputation for delivering high-quality, customized solutions tailored to maltose industry needs. With a commitment to R&D, HeadPowder continuously improves products to meet evolving industry standards and customer requirements. Advanced manufacturing and quality control systems ensure each equipment meets stringent performance and safety criteria. HeadPowder’s dedication to excellence has made it a trusted partner for businesses seeking reliable maltose handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top