HeadPowder, a leading provider in the field of material handling solutions, specializes in the efficient and reliable transportation of rare earth mineral powders. This article delves into the operational process and underlying principles that govern the handling of these critical materials, highlighting the technical aspects and practical applications essential for industrial operations.
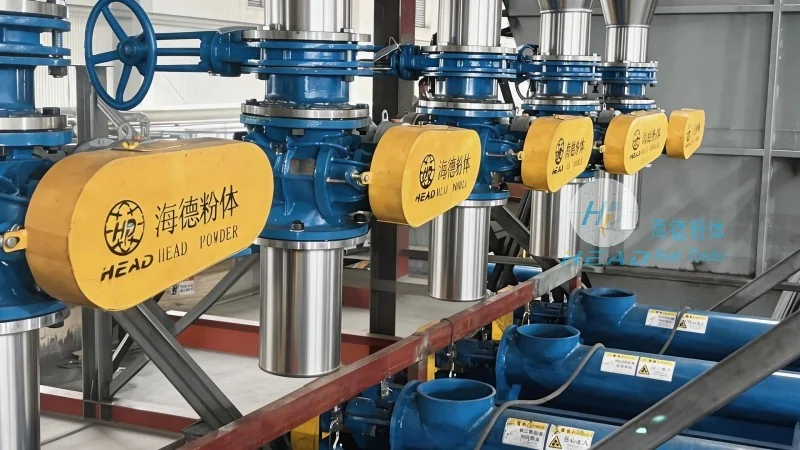
Rare earth minerals are vital components in modern industrial applications, including electronics, renewable energy, and advanced manufacturing. The safe and efficient transportation of these powders is crucial to maintaining production efficiency and ensuring product quality. HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has developed specialized systems tailored to meet the unique challenges of handling rare earth mineral powders, ensuring optimal performance and minimal risk.
The material handling system for rare earth mineral powders typically consists of several integrated components designed to facilitate smooth and controlled movement. These components include feeders, conveyors, storage silos, and control systems, each playing a critical role in the overall operation. The feeders are responsible for accurately measuring and dispensing the powder, while the conveyors transport it from one location to another with precision. Storage silos provide a secure and controlled environment for bulk storage, preventing contamination and maintaining material integrity. Advanced control systems monitor and regulate the entire process, ensuring consistent performance and safety.
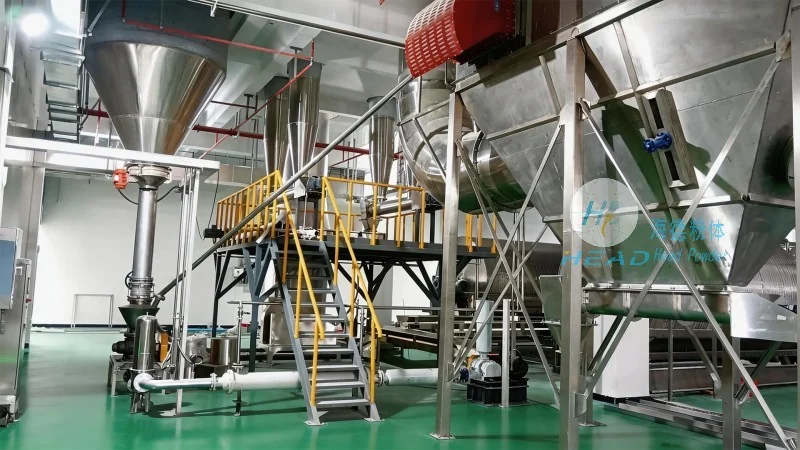
The operation process of the rare earth mineral powder material handling system begins with the loading of raw materials into the storage silo. The control system then initiates the feeding process, where the feeder measures the required amount of powder and releases it into the conveyor system. The conveyor transports the powder to the processing or packaging area, where it is further handled as per the production requirements. Throughout the process, sensors and monitoring devices continuously track key parameters such as flow rate, pressure, and temperature, providing real-time data to the control system. This data is used to adjust the operation parameters dynamically, ensuring optimal performance and preventing any potential issues.
The working principle of the material handling system for rare earth mineral powders is based on the principles of fluidization and controlled flow. The powder is treated as a fluid-like substance under specific conditions, allowing it to be transported efficiently through the system. The feeders use a combination of mechanical and pneumatic mechanisms to control the flow rate, ensuring consistent and uniform dispensing. The conveyors utilize either belt or screw mechanisms, depending on the specific application, to move the powder smoothly. The storage silos are designed with a conical or hopper shape to facilitate gravity-fed flow, reducing the need for additional energy input. The control system integrates all these components, using feedback loops to maintain stability and prevent overloading or underflow conditions.
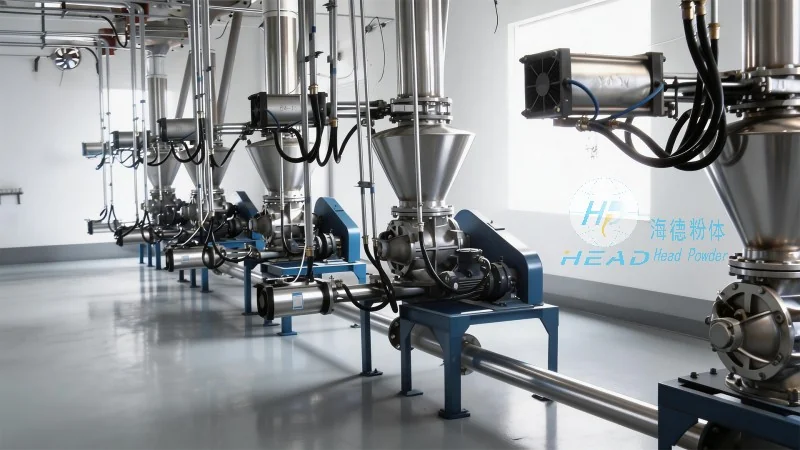
HeadPowder Engineering Co., Ltd. offers several advantages in the design and implementation of rare earth mineral powder material handling systems. The company's expertise in material science and industrial engineering ensures that the systems are tailored to the specific characteristics of rare earth minerals, such as their fine particle size and potential for dust generation. The systems are designed to minimize dust emissions and ensure environmental compliance, while maximizing operational efficiency. Additionally, the use of advanced materials and corrosion-resistant components ensures long-term durability and low maintenance costs. The company's commitment to quality and safety is reflected in the robust design and rigorous testing of all its systems, providing customers with reliable and dependable solutions.
In conclusion, the operation process and working principle of rare earth mineral powder material handling systems are complex and require specialized knowledge and equipment. HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, has established itself as a leading provider of these critical systems, offering efficient, reliable, and safe solutions for the transportation and handling of rare earth minerals. By understanding the technical aspects and practical applications of these systems, industrial operations can enhance their productivity and ensure the quality of their products.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top