Ammonia fertilizer pneumatic conveying lines are critical components in modern agricultural and industrial operations, designed to efficiently transport ammonia-based fertilizers from storage to application points. These systems leverage pneumatic technology to move bulk materials through a network of pipes, ensuring safe, reliable, and high-capacity material handling. The operation of such lines involves several key stages and principles that contribute to their effectiveness in various applications.
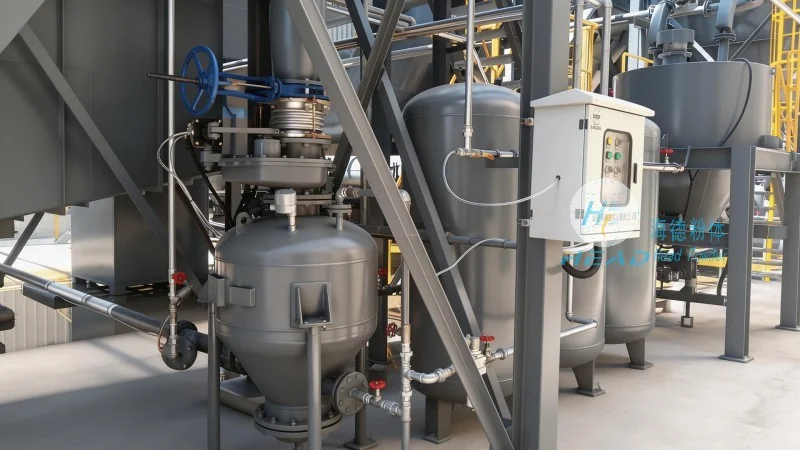
Ammonia fertilizer pneumatic conveying systems are engineered to handle the unique properties of ammonia-based fertilizers, which include high reactivity, corrosive nature, and the need for precise control during transport. These systems are typically composed of a series of components, including a hopper for material storage, a blower or compressor to generate airflow, a pipeline network for material transport, and a discharge unit for material release. The design of these systems is tailored to meet the specific requirements of the fertilizer type, such as granular or liquid ammonia, and the operational conditions of the site, including distance, elevation, and material flow rate. The company, Shandong HeadPowder Engineering Co., Ltd., specializes in the design and manufacturing of such systems, providing customized solutions for various industrial and agricultural applications.
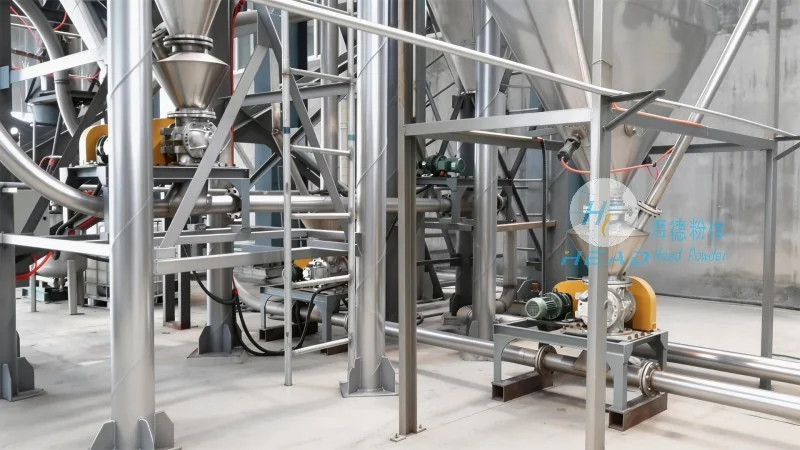
The core components of an ammonia fertilizer pneumatic conveying line include the material hopper, which stores the fertilizer and provides a controlled feed to the system. The hopper is equipped with a feeder mechanism, such as a rotary valve or screw conveyor, to regulate the flow of material into the pipeline. The blower or compressor generates the necessary air pressure to move the material through the system. In some designs, a filter or separator is included to remove any dust or debris from the air before it is discharged, ensuring compliance with environmental regulations and maintaining system efficiency. The pipeline network consists of straight sections, bends, and fittings that are carefully selected to minimize pressure loss and maintain consistent airflow. The discharge unit, often a rotary valve or a controlled outlet, allows the fertilizer to be released at the desired location, such as a field or a storage silo. The company ensures that all components are made from high-quality materials, such as stainless steel, to withstand the corrosive nature of ammonia-based fertilizers and ensure long-term durability.
The working principle of ammonia fertilizer pneumatic conveying lines is based on the use of air as the conveying medium. The system operates by creating a pressure differential between the inlet and outlet of the pipeline. The blower or compressor supplies high-pressure air into the hopper, which lifts the fertilizer particles and propels them through the pipeline. The air and material mixture travels at a velocity sufficient to overcome the gravitational forces and friction within the system. As the mixture moves through the pipeline, the air velocity and pressure are maintained at optimal levels to ensure efficient transport without causing material degradation or system damage. The system may use different conveying modes, such as dilute-phase or dense-phase, depending on the material characteristics and operational requirements. Dilute-phase conveying involves a lower air-to-material ratio, resulting in higher velocities and shorter transport distances, while dense-phase conveying uses a higher air-to-material ratio, allowing for longer distances and more controlled material flow. The company's engineers design systems based on the specific conveying needs, ensuring optimal performance for each application.
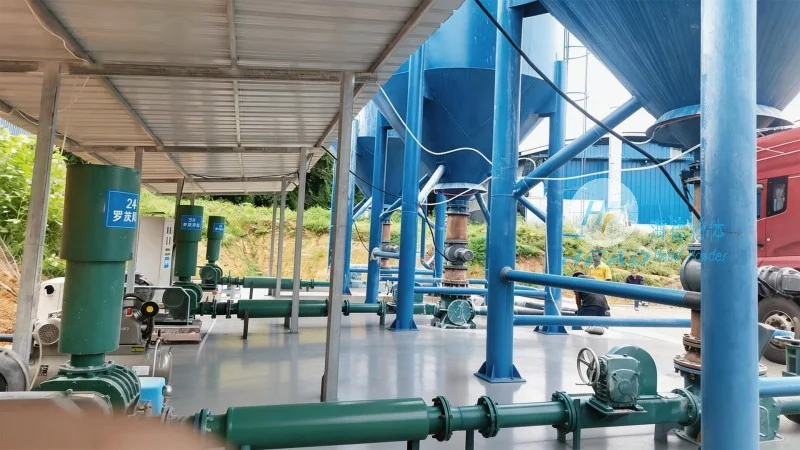
The operation process of an ammonia fertilizer pneumatic conveying line begins with the loading of the fertilizer into the material hopper. The hopper is typically equipped with a level sensor to monitor the material level and trigger the feeder mechanism when the level drops below a certain threshold. The feeder mechanism then starts to feed the fertilizer into the pipeline at a controlled rate, ensuring a steady flow of material. The blower or compressor is activated, and the air is introduced into the hopper, creating a pressure that lifts the fertilizer particles. The mixture of air and material is then transported through the pipeline network to the discharge unit. At the discharge point, the air is separated from the fertilizer, and the fertilizer is released into the intended application area. The system may include a control panel that monitors key parameters, such as pressure, flow rate, and material level, and adjusts the operation of the feeder and blower as needed to maintain optimal performance. The entire process is designed to be automated, reducing the need for manual intervention and improving operational efficiency. The company provides comprehensive training and support to ensure that operators can effectively manage the system and maximize its performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top