For industrial applications requiring efficient and reliable material handling, bulk bag pneumatic conveying lines offer a robust solution. These systems are designed to transport bulk materials from storage containers, such as super sacks or bulk bags, to processing equipment or storage areas. The technology is widely used in industries like food, pharmaceuticals, chemicals, and minerals, where maintaining product integrity and minimizing contamination is critical.
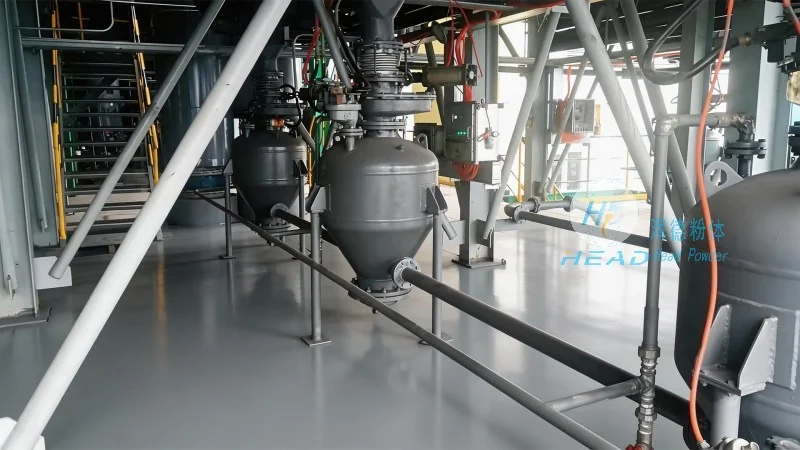
Bulk bag pneumatic conveying lines are specialized systems that utilize air pressure or vacuum to move bulk materials through a network of pipes. The system typically includes a bulk bag discharger, an air compressor or vacuum pump, a filter system, and a receiving hopper or silo. The design ensures that materials are transferred safely and efficiently, with minimal dust generation and product degradation. This technology is particularly advantageous for handling powders, granules, and other dry bulk materials that are prone to caking or segregation.
The operation of a bulk bag pneumatic conveying line involves several key steps. First, the bulk bag is placed on a discharge frame or hopper, ensuring it is properly secured and aligned with the system. The discharge valve of the bulk bag is then opened, allowing the material to flow into the conveying line. Simultaneously, the air compressor or vacuum pump is activated to create the necessary pressure or vacuum in the system. As the air flows through the pipes, it entrains the material particles, forming a dense phase or dilute phase flow depending on the system design. The material is then transported from the discharge point to the receiving container, such as a silo or processing unit. Once the bulk bag is empty, the system can be prepared for the next load, with the discharge valve closed and the air supply turned off.
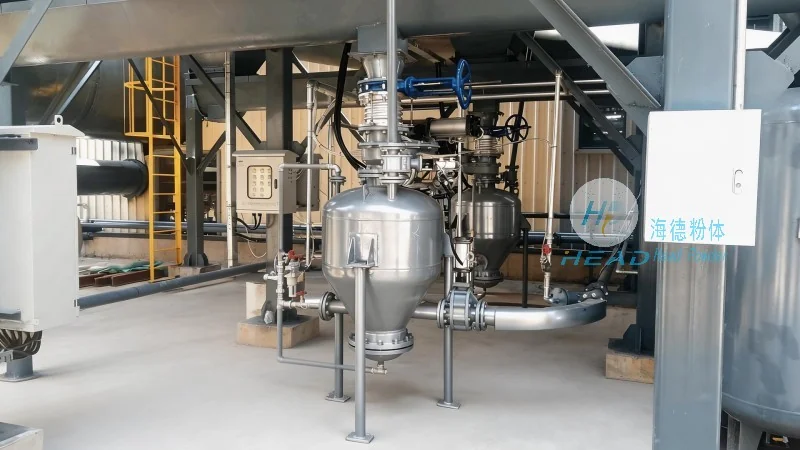
The working principle of bulk bag pneumatic conveying lines is based on the fundamental physics of fluid dynamics and particle transport. The system operates by creating a pressure differential between the discharge point and the receiving point. In a positive pressure system, the air compressor supplies compressed air to the conveying line, pushing the material forward. In a negative pressure system, a vacuum pump creates a vacuum that pulls the material through the line. The choice between positive and negative pressure depends on factors such as material properties, system layout, and operational requirements. The conveying line is equipped with filters to remove any dust or debris from the air stream, ensuring that the material remains clean and free from contamination. Additionally, the system may include a cyclone separator or a bag filter to further enhance air purification and material recovery.
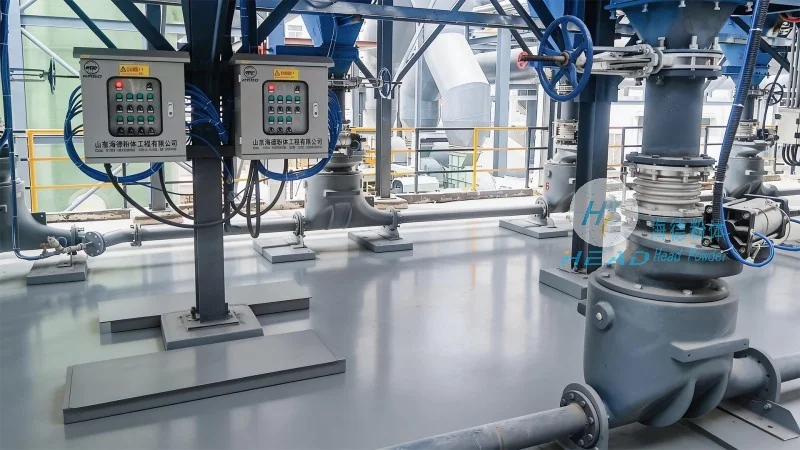
Several critical components work together to ensure the smooth operation of bulk bag pneumatic conveying lines. The bulk bag discharger, or super sack discharger, is responsible for safely opening and emptying the bulk bag. It typically includes a hopper, a discharge valve, and a sealing mechanism to prevent dust leakage. The air compressor or vacuum pump provides the necessary air pressure or vacuum to move the material. The filter system, including a pre-filter and a main filter, removes particles from the air stream, protecting the compressor and ensuring clean material transfer. The receiving hopper or silo collects the material and may include a level sensor to monitor the material level. The control panel manages the operation of the system, allowing for start, stop, and monitoring of key parameters such as pressure, flow rate, and material level.
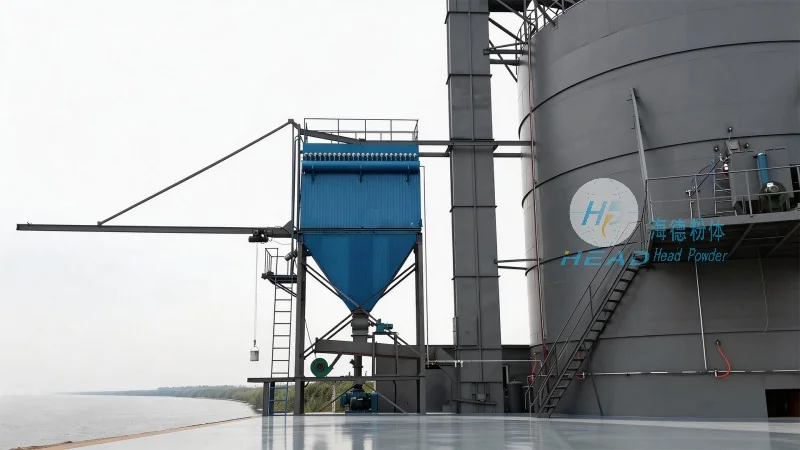
Bulk bag pneumatic conveying lines offer numerous benefits for industrial material handling. These include high efficiency in material transfer, reduced labor costs compared to manual handling, and improved safety by minimizing exposure to dust and other hazards. The systems are also flexible, allowing for easy integration with existing processing equipment and the ability to handle a wide range of material types. Applications include the transport of food ingredients, pharmaceutical powders, chemical additives, and mineral ores. The technology is particularly suitable for applications where product purity and contamination control are paramount, such as in the food and pharmaceutical industries.
Bulk bag pneumatic conveying lines are advanced material handling systems that combine efficiency, reliability, and safety. By understanding the operation process and working principles, users can optimize their material transfer operations and ensure consistent performance. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality bulk bag pneumatic conveying solutions tailored to the specific needs of various industries. With a focus on innovation and customer satisfaction, HeadPowder continues to deliver reliable and efficient systems that meet the demands of modern industrial applications. Based in Shandong, China, HeadPowder leverages its expertise to design and manufacture systems that enhance productivity and safety in material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top