Rare earth materials are critical components in modern industrial applications, and efficient material handling is essential for optimizing production lines. Pneumatic conveying systems offer a reliable and flexible solution for transporting rare earth powders and granules. This article provides an in-depth look at the operation process and working principle of such systems, highlighting the key components, operational steps, and technical advantages.
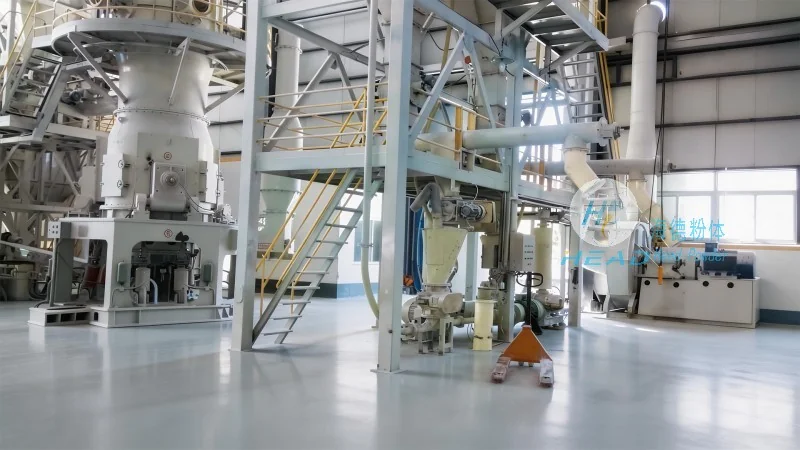
HeadPowder, a leading provider of material handling solutions, specializes in designing and manufacturing advanced pneumatic conveying systems. With a focus on precision and efficiency, the company has established itself as a trusted partner for industries dealing with rare earth materials. HeadPowder Engineering Co., Ltd. is headquartered in Shandong, China, and serves clients globally with tailored solutions that meet their specific operational needs.
The core components of a rare earth pneumatic conveying system include the material hopper, feeder, air compressor, conveying line, and receiver. The material hopper is designed to store the rare earth powder or granules, ensuring a consistent feed to the system. The feeder, typically a rotary valve or screw feeder, controls the flow rate of the material into the conveying line. The air compressor generates the necessary pressure to move the material through the system, while the conveying line (usually made of stainless steel or plastic) transports the material from the hopper to the receiver. The receiver collects the material and may include a dust collection system to ensure environmental compliance.
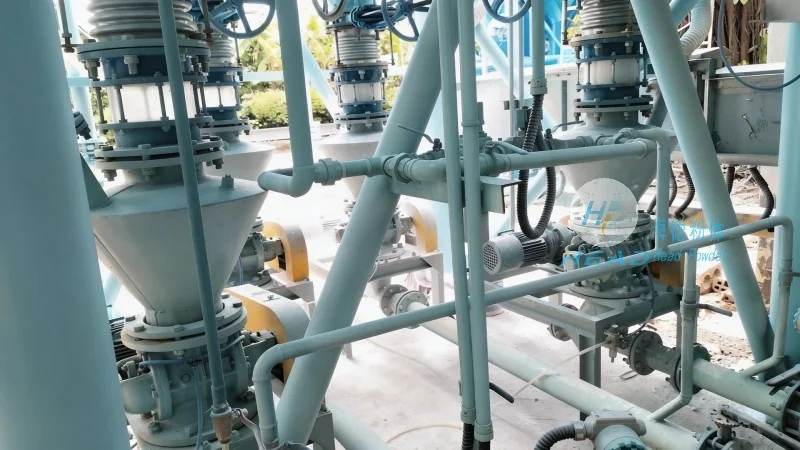
The operation process of a rare earth pneumatic conveying system involves several sequential steps. First, the rare earth material is loaded into the material hopper. The feeder then regulates the material flow, ensuring a steady supply to the conveying line. The air compressor is activated, generating the required air pressure to create a flow of air through the system. As the air flows through the conveying line, it entrains the rare earth particles, forming a slurry-like mixture that is transported to the receiver. The receiver collects the material, and the air is typically filtered and recycled back to the system to improve energy efficiency. This continuous process allows for the efficient and safe transportation of rare earth materials over long distances or within complex production facilities.
The working principle of a pneumatic conveying system is based on the principle of fluidization and particle suspension. When air is introduced into the conveying line at a sufficient velocity, it creates a low-pressure zone that draws the rare earth particles into the air stream. The particles are then suspended in the air and transported through the system. The velocity of the air must be high enough to overcome the gravitational forces acting on the particles but low enough to prevent particle degradation or wear on the system components. The system's design, including the size of the conveying line and the air pressure, is optimized to achieve the best balance between material transport efficiency and energy consumption.
HeadPowder's rare earth pneumatic conveying systems offer several technical advantages that make them ideal for handling sensitive materials like rare earth powders. These systems provide a dust-free and enclosed environment, which is crucial for maintaining material purity and ensuring worker safety. The enclosed design also reduces the risk of material contamination and environmental pollution. Additionally, the systems are highly flexible, allowing for easy integration into existing production lines and adaptation to changing operational requirements. The use of stainless steel components ensures corrosion resistance, which is essential for handling corrosive or moisture-sensitive rare earth materials. The energy-efficient design, with features like air recycling and optimized pressure control, reduces operational costs and minimizes environmental impact.
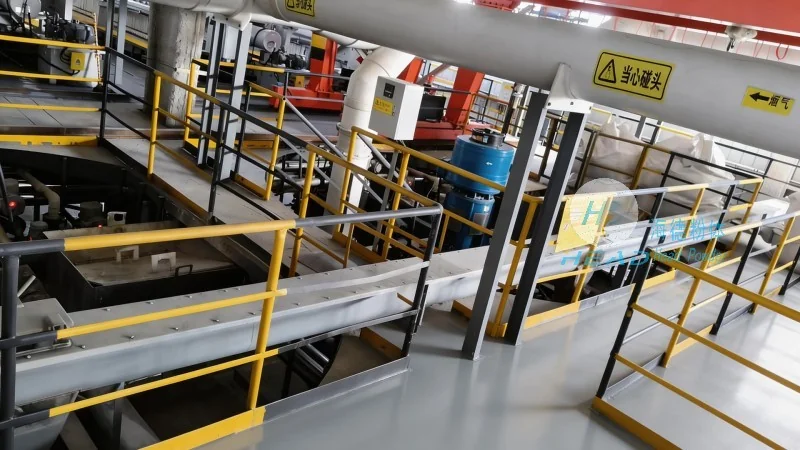
Rare earth pneumatic conveying systems are widely used in various applications within the rare earth industry. These include the transportation of rare earth oxides, rare earth metals, and rare earth compounds from processing plants to storage facilities or to downstream manufacturing processes. The systems are also used in the handling of rare earth concentrates and intermediate products, ensuring a smooth and continuous flow of materials throughout the production cycle. The reliability and efficiency of these systems contribute to improved production throughput and reduced downtime, which are critical factors for the success of rare earth processing operations.
HeadPowder Engineering Co., Ltd. provides advanced rare earth pneumatic conveying systems that combine cutting-edge technology with robust design. By understanding the operation process and working principle of these systems, industries can optimize their material handling processes, enhance productivity, and ensure compliance with environmental and safety standards. With a focus on quality and customer satisfaction, HeadPowder continues to deliver innovative solutions that meet the evolving needs of the rare earth industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top