Efficient handling of fly ash is crucial in modern power generation and industrial processes, and the pneumatic conveying system for fly ash silos plays a vital role in achieving this goal. This system, developed by Shandong HeadPowder Engineering Co., Ltd., a leading company in the field, ensures reliable and safe transportation of fly ash from storage silos to processing or disposal units. The following content provides a detailed overview of the operation process and working principle of this advanced system.
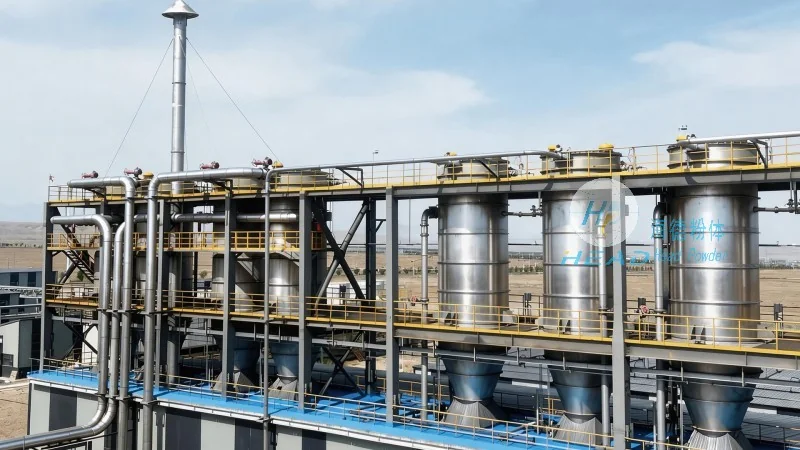
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier specializing in pneumatic conveying equipment and related solutions. With its headquarters located in Shandong, China, the company has built a strong reputation for delivering high-quality, customized systems tailored to the specific needs of clients in the power, cement, and other industrial sectors. HeadPowder's expertise lies in designing and implementing efficient material handling solutions that enhance operational efficiency and reduce downtime.
The fly ash silo pneumatic conveying system consists of several key components, each playing a critical role in the overall operation. These components include the fly ash silo (storage vessel), the pneumatic conveying pipeline, the air compressor or blower unit, the control system, and the receiving hopper or processing equipment. The silo is designed to store large quantities of fly ash, providing a stable and controlled environment for material storage. The conveying pipeline is typically made of durable materials such as stainless steel or high-density polyethylene to withstand the abrasive nature of fly ash and the pressure from the air flow. The air compressor or blower generates the necessary air pressure to move the fly ash particles through the pipeline, while the control system monitors and regulates the flow rate, pressure, and other operational parameters to ensure safe and efficient operation.
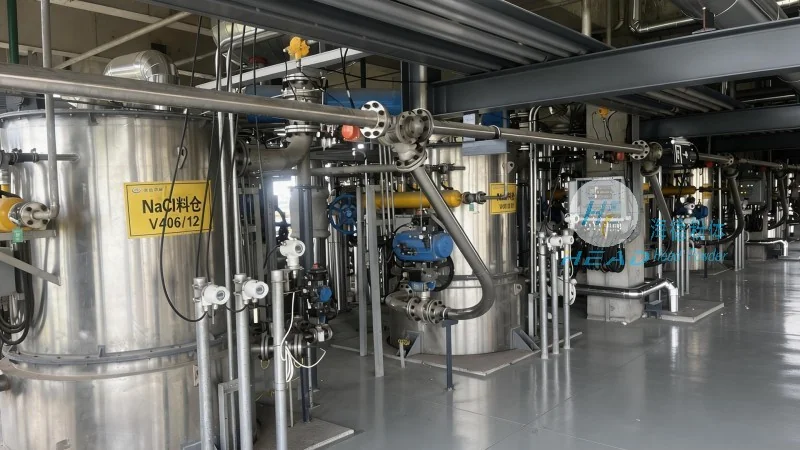
The operation of the fly ash silo pneumatic conveying system follows a systematic process that ensures smooth and continuous material transport. The process begins with the loading of fly ash into the silo, which is typically done using a hopper or a conveyor system. Once the silo is filled, the control system activates the air compressor, which starts to generate compressed air. The compressed air is then introduced into the conveying pipeline, creating a pressure differential that propels the fly ash particles from the silo to the receiving end. As the air flows through the pipeline, it entrains the fly ash particles, forming a slurry-like mixture that moves through the system. The receiving hopper or processing equipment is positioned at the end of the pipeline, where the fly ash is deposited and then further processed or disposed of according to the client's requirements. The entire process is automated and can be controlled remotely, allowing operators to monitor and adjust the system parameters as needed to maintain optimal performance.
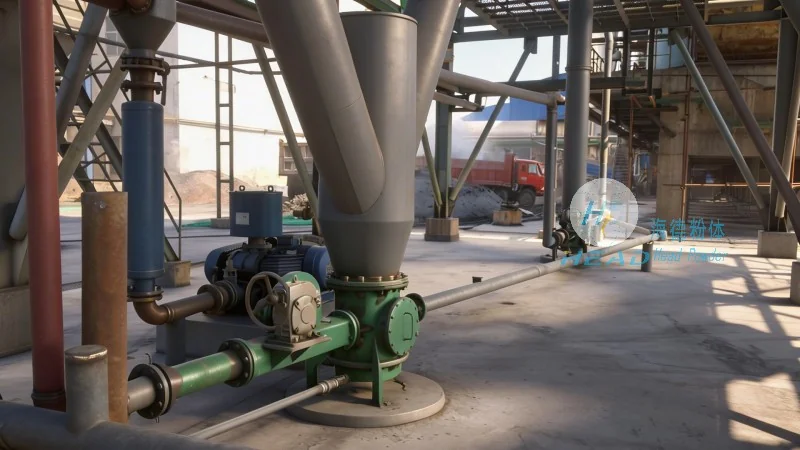
The working principle of the pneumatic conveying system is based on the principle of fluidization and particle entrainment. When compressed air is introduced into the conveying pipeline, it creates a low-pressure zone that draws the fly ash particles from the silo into the pipeline. The air flow velocity is carefully controlled to ensure that the particles are fully entrained and transported without causing excessive wear or blockages in the pipeline. The system operates under either positive pressure or negative pressure (or a combination of both), depending on the specific application and the distance between the silo and the receiving equipment. Positive pressure systems are commonly used for short-distance conveying, while negative pressure systems are preferred for longer distances or when the material needs to be transported from multiple silos to a central processing unit. The control system continuously monitors the pressure and flow rate, adjusting the air supply to maintain a stable and efficient conveying process. This ensures that the fly ash is transported safely and efficiently, minimizing the risk of dust emissions and material loss.
The fly ash silo pneumatic conveying system offers several advantages over traditional methods such as bucket elevators or belt conveyors. These advantages include higher conveying capacity, lower maintenance costs, and reduced risk of material contamination. The system is also more flexible, as it can be easily modified or expanded to accommodate changes in production needs. The system is widely used in power plants, cement factories, and other industrial facilities where fly ash needs to be transported from storage silos to processing or disposal units. By using this system, clients can improve their operational efficiency, reduce labor costs, and enhance the overall safety of their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top