Principles and Working Scene Characteristics of White and Gray Material Conveying
Release time:2026-09-19 08:01:31
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
White and gray materials, such as lime, gypsum, and other powders, are widely used in industrial processes. The efficient and reliable transportation of these materials is crucial for maintaining production efficiency and ensuring product quality. This article explores the fundamental principles behind white and gray material conveying systems and highlights key working scene characteristics that define their application in various industrial settings.
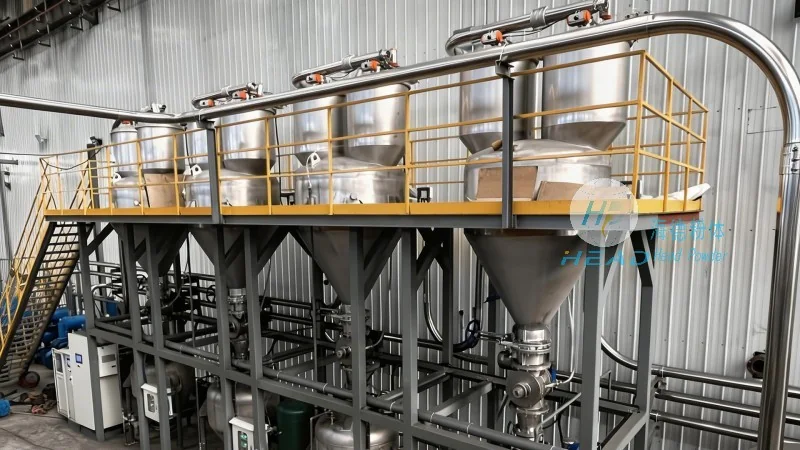
Core Principles of Material Conveying
The primary principle of white and gray material conveying is to transport bulk materials from one location to another with minimal loss, contamination, and energy consumption. Key principles include:
- Continuous and uniform flow control to prevent material buildup or clogging.
- Seal integrity to avoid dust emissions and maintain environmental compliance.
- Energy efficiency through optimized system design and operation.
- Flexibility to accommodate different material properties and operational requirements.
These principles are achieved through the use of specialized equipment like screw conveyors, pneumatic conveyors, and bucket elevators, each tailored to the specific characteristics of white and gray materials. For instance, screw conveyors are ideal for handling free-flowing powders with low to moderate moisture content, while pneumatic systems excel in transporting fine powders over longer distances with minimal maintenance.
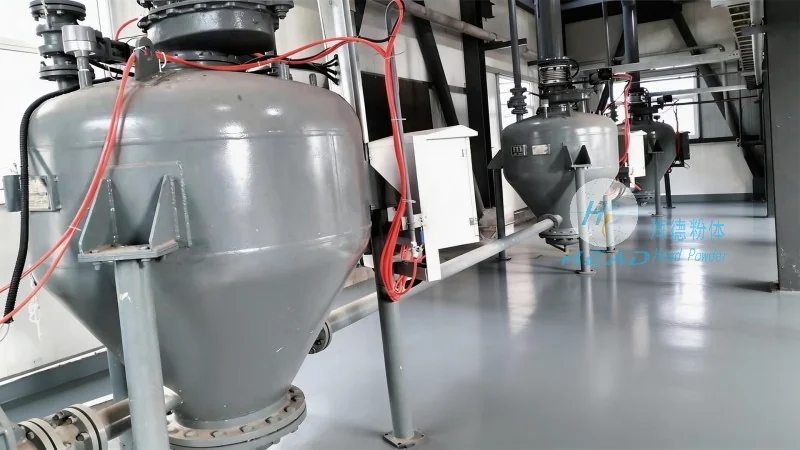
Working Scene Characteristics
The working scene characteristics of white and gray material conveying systems are defined by several factors that influence system selection and performance. These include:
- Material Properties: The physical and chemical properties of the material, such as particle size, moisture content, and flowability, directly impact the choice of conveying equipment. For example, cohesive materials may require special designs to prevent blockages, while lightweight powders may need higher air velocities in pneumatic systems.
- Application Requirements: The specific application, such as raw material feeding, product transport, or waste removal, dictates the system's design. In cement production, for instance, conveying systems must handle large volumes of raw materials and ensure consistent feed rates to the kiln.
- Environmental and Safety Considerations: Modern conveying systems prioritize dust control and safety. Enclosed systems and dust collection mechanisms are common to comply with environmental regulations and protect personnel from airborne particles.
- Space and Layout Constraints: The available space and layout of the facility influence the system's configuration. Horizontal, vertical, or combined horizontal-vertical designs are used to fit within the operational area while maintaining efficient material flow.
Application Examples in Industrial Settings
White and gray material conveying systems are integral to numerous industrial processes across various sectors. Some common applications include:
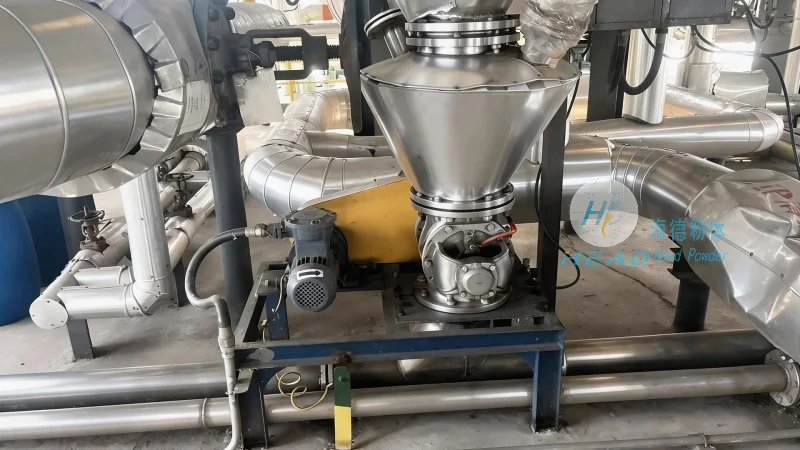
- Cement and Concrete Production: Conveying raw materials like limestone, clay, and gypsum from storage to processing units. The systems must handle large volumes and ensure consistent material quality for cement production.
- Pharmaceutical and Food Processing: Transporting powders like limestone or gypsum in food and pharmaceutical manufacturing. Here, hygiene and contamination control are critical, requiring sealed and sanitary conveying systems.
- Chemical Manufacturing: Handling chemicals and additives in chemical plants. The systems must be robust and resistant to corrosion, especially when dealing with acidic or caustic materials.
- Mineral Processing: Conveying minerals and ores from crushing and grinding stages to storage or further processing. The systems must handle abrasive materials and prevent wear on components.
Key Features of Effective Conveying Solutions
Effective white and gray material conveying solutions from Shandong HeadPowder Engineering Co., Ltd. (headpowder) incorporate several key features that enhance performance and reliability. These include:
- Customized System Design: Tailored to specific material properties and application requirements, ensuring optimal performance and minimal downtime.
- Advanced Control Systems: Integrated control panels and sensors provide real-time monitoring and automatic adjustments to maintain consistent flow rates and system efficiency.
- Durable and Corrosion-Resistant Components: High-quality materials and coatings protect against wear and corrosion, extending the system's service life.
- Energy-Efficient Operation: Optimized designs and energy-saving features reduce operational costs while maintaining performance.
- Comprehensive Support and Maintenance: Headpowder offers technical support, maintenance services, and spare parts to ensure long-term system reliability.
Conclusion
White and gray material conveying systems are essential for efficient industrial operations, and understanding their principles and working scene characteristics is critical for selecting the right equipment. With a focus on customization, durability, and efficiency, companies like Shandong HeadPowder Engineering Co., Ltd. provide reliable solutions that meet the diverse needs of modern industries. By adhering to the core principles of material handling and leveraging advanced technology, these systems ensure smooth, safe, and cost-effective transportation of white and gray materials in various applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
