Long-distance powder conveying systems are critical in various industrial applications, enabling the efficient transport of bulk powders over significant distances. These systems are designed to handle materials such as cement, coal, flour, and other fine particulate materials, ensuring reliable and consistent performance in demanding environments. The technology behind these systems combines mechanical engineering principles with advanced control systems to optimize material handling processes.
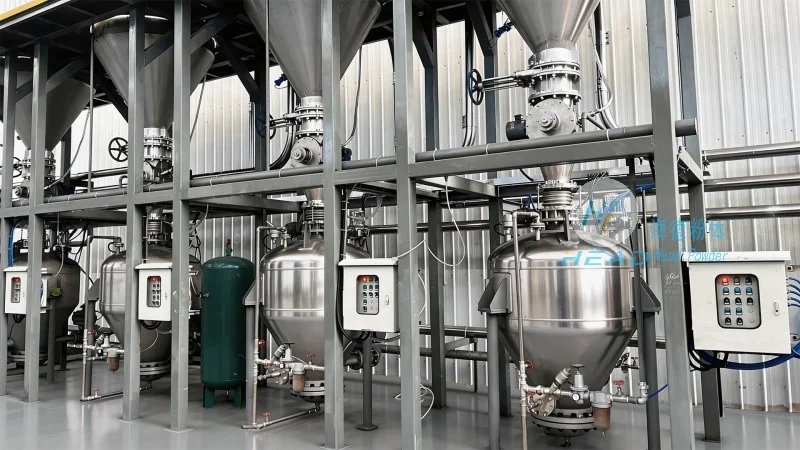
The fundamental principle of long-distance powder conveying involves the use of pneumatic or mechanical methods to move bulk materials. Pneumatic conveying systems utilize compressed air to create a flow that transports the powder through pipelines, while mechanical systems rely on screw conveyors, belt conveyors, or bucket elevators. The choice of system depends on factors like material properties, required distance, and operational conditions. For instance, pneumatic systems are ideal for high-volume, low-density materials, whereas mechanical systems may be preferred for abrasive or high-density powders.
Long-distance powder conveying systems consist of several key components that work in tandem to ensure smooth operation. The primary components include the material feed hopper, which stores and feeds the powder into the system; the conveying pipeline, which transports the material; and the control unit, which regulates the flow and pressure. Additionally, systems may include dust collectors, silos, and safety valves to maintain operational safety and material quality. Each component is engineered to withstand the specific stresses of the material being conveyed, ensuring durability and long-term reliability.
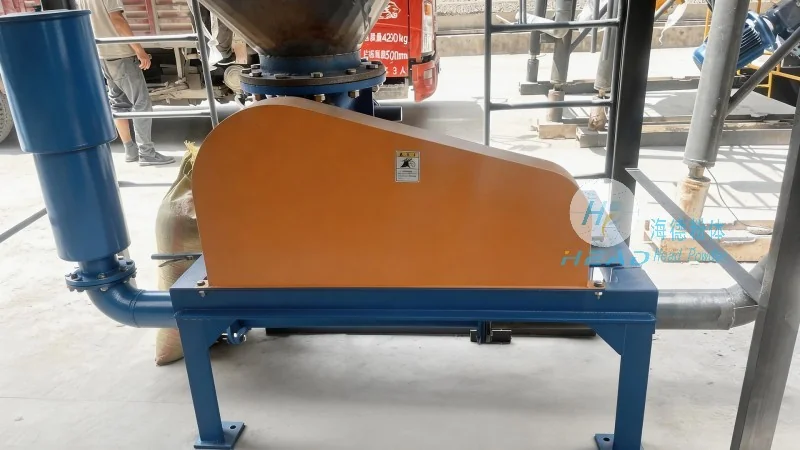
Long-distance powder conveying systems find extensive applications across multiple industries. In the cement industry, these systems are used to transport raw materials and finished products over long distances, improving production efficiency and reducing transportation costs. The food industry also benefits from these systems, as they enable the safe and hygienic handling of flour, sugar, and other food powders. Additionally, in the chemical and pharmaceutical sectors, these systems are crucial for transporting raw materials and intermediates, ensuring precise dosing and minimal contamination. The versatility of long-distance powder conveying systems makes them indispensable in modern industrial operations.
Implementing long-distance powder conveying systems offers several advantages over traditional material handling methods. One of the primary benefits is the reduction in labor costs, as automated systems minimize the need for manual handling. Additionally, these systems enhance safety by eliminating the risks associated with manual material transport, such as dust exposure and physical strain. The efficiency of long-distance conveying also leads to improved production throughput, as materials can be moved quickly and consistently. Furthermore, the systems are designed to be energy-efficient, reducing operational costs and environmental impact. These advantages make long-distance powder conveying systems a preferred choice for industries seeking to optimize their material handling processes.
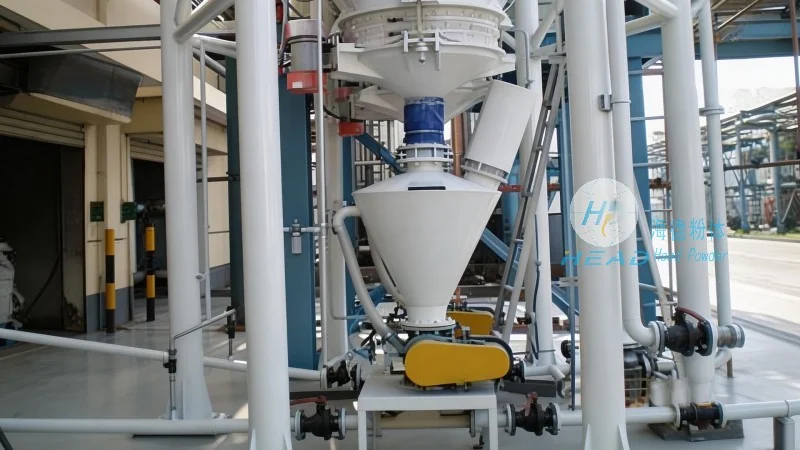
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized long-distance powder conveying systems tailored to the specific needs of clients. The company, operating under the brand name headpowder, leverages advanced engineering expertise to develop solutions that meet the unique requirements of various industries. Whether for short or long-distance applications, the systems can be scaled to handle varying material volumes and distances. The company’s commitment to quality and innovation ensures that each system is built to withstand the demands of industrial environments, providing reliable performance over extended periods. With a focus on customer satisfaction and technical excellence, headpowder delivers tailored solutions that enhance operational efficiency and productivity.
Long-distance powder conveying systems represent a significant advancement in material handling technology, offering efficient and reliable solutions for transporting bulk powders. The principles and components of these systems are continuously evolving, driven by advancements in engineering and control technology. As industries continue to seek more efficient and sustainable operations, the demand for advanced powder conveying systems is expected to grow. Shandong HeadPowder Engineering Co., Ltd., with its expertise and commitment to quality, remains at the forefront of developing innovative solutions that meet the evolving needs of the market. By leveraging the latest technologies and engineering practices, the company ensures that its systems provide long-term value and contribute to the success of its clients’ operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top