Rice husk, a byproduct of rice processing, is increasingly recognized as a valuable raw material in various industrial applications. The efficient and reliable transportation of rice husk powder is crucial for optimizing production processes and enhancing overall operational efficiency. This article explores the fundamental principles underlying rice husk powder conveying systems and highlights the key characteristics of different working scenarios where such systems are applied.
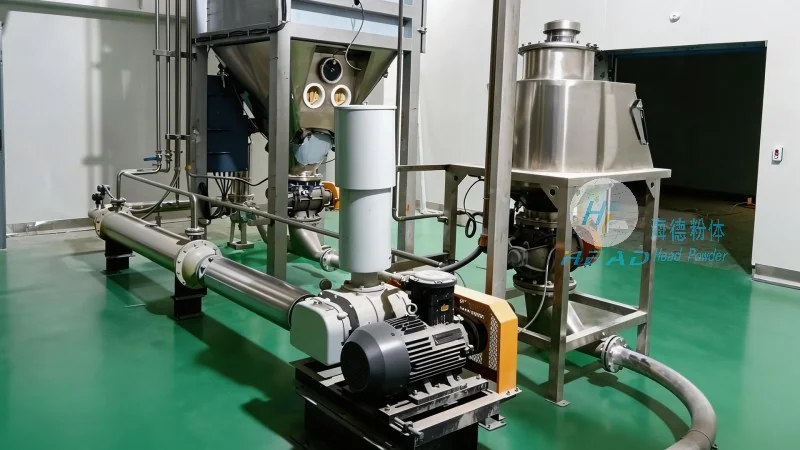
The primary principle of rice husk powder conveying involves the movement of fine particles, such as rice husk, from one location to another within industrial facilities. This process can be achieved through several methods, with the most common being pneumatic conveying and mechanical conveying. Pneumatic conveying utilizes air or other gases to transport the powder, leveraging pressure differentials or vacuum to move the material. Mechanical conveying, on the other hand, relies on physical components like screws, belts, or buckets to transport the powder. The choice of conveying method depends on factors such as the particle size, moisture content, and the distance over which the powder needs to be transported.
For rice husk powder, which typically has a relatively uniform particle size and moderate moisture content, pneumatic conveying is often preferred due to its ability to handle fine powders efficiently and with minimal product degradation. The system generally consists of a hopper, a conveyor line, and a receiver. The hopper stores the rice husk powder, while the conveyor line transports it to the receiver. The air flow is controlled to ensure the powder is conveyed without clogging or excessive pressure drops. This method is particularly effective for long-distance conveying and for applications where dust control is a priority.
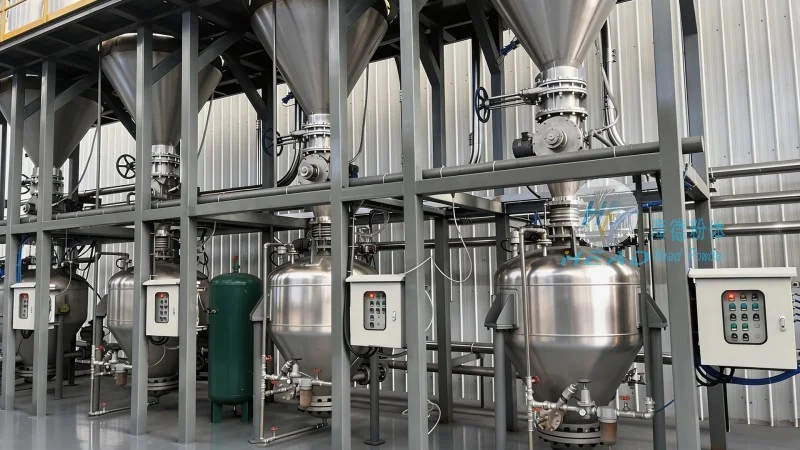
The working scene characteristics of rice husk powder conveying systems vary significantly based on the specific industrial application and the scale of operation. These characteristics include factors such as the volume of material to be conveyed, the distance between the source and destination, the environmental conditions, and the required level of automation. In biomass energy production, for example, large volumes of rice husk powder are transported from storage silos to combustion or gasification units. The conveying system must be capable of handling high throughput rates while maintaining consistent flow rates to ensure stable operation of the downstream processes.
In the field of environmental remediation and waste management, rice husk powder is often used as a sorbent for air purification or as a component in composting processes. The conveying system in this scenario may need to operate in more controlled environments, with features like dust collection and filtration to prevent environmental contamination. The system must also be designed to handle varying particle sizes and moisture levels, as the raw material may be subject to different processing conditions.
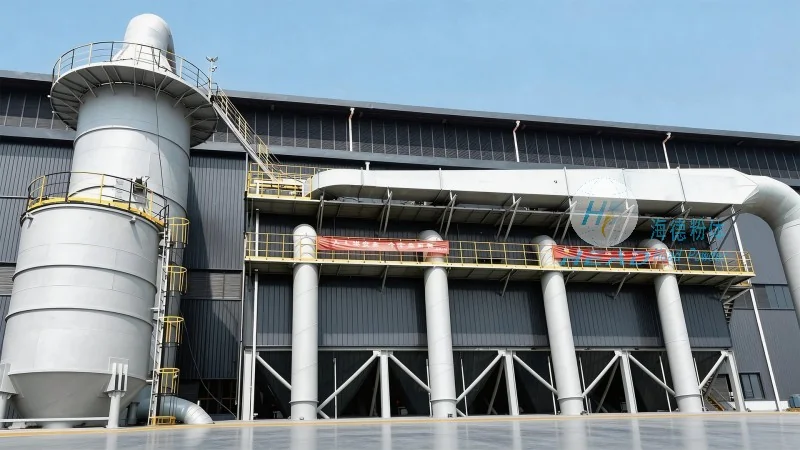
Rice husk powder conveying systems are widely applied across multiple industries, each with its unique requirements and operational parameters. In the agricultural and food processing sector, rice husk is used as a raw material for animal feed or as a component in the production of biofuels. The conveying system must be hygienic and easy to clean to meet food safety standards. In the construction industry, rice husk powder can be used as a filler in composite materials or as a component in insulation products. The system must be robust and capable of handling abrasive particles to ensure long-term durability.
In the chemical and pharmaceutical industries, rice husk powder is sometimes used as a raw material for the production of chemicals or as a filter aid. The conveying system in these applications must be designed to prevent contamination and to maintain the purity of the powder. This often involves the use of closed systems and specialized materials to avoid cross-contamination with other substances.
Over the years, technological advancements have significantly improved the efficiency and reliability of rice husk powder conveying systems. Modern systems often incorporate advanced control systems that monitor and adjust the conveying parameters in real-time, ensuring optimal performance. Sensors are used to detect flow rates, pressure drops, and other critical parameters, providing operators with immediate feedback and allowing for quick adjustments if necessary. Additionally, the use of high-efficiency motors and energy-saving designs has reduced the operational costs of the conveying systems, making them more economically viable for industrial applications.
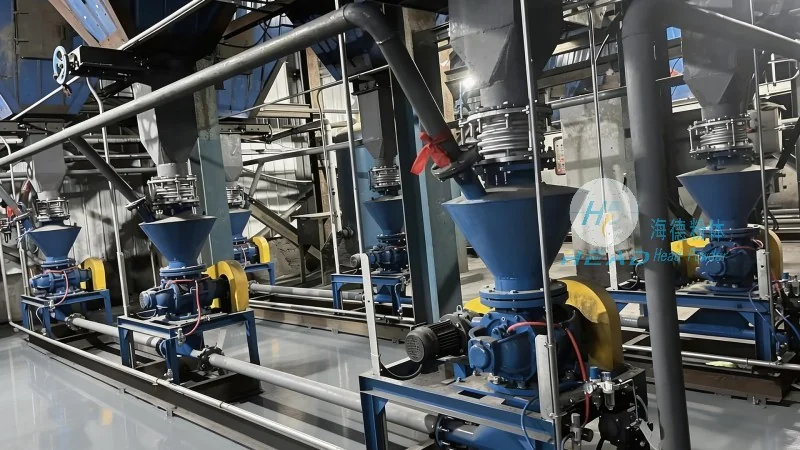
Another significant advancement is the development of flexible and modular conveying systems. These systems can be easily reconfigured to accommodate changes in production volume or to adapt to different working scenarios. This modularity allows companies to scale their operations without the need for extensive system overhauls, providing greater flexibility and cost savings.
Efficient rice husk powder conveying is essential for maximizing the utilization of this valuable byproduct and for optimizing industrial processes. The principles and working scene characteristics discussed above highlight the importance of selecting the appropriate conveying method and system design for specific applications. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design, manufacturing, and installation of advanced powder conveying systems tailored to the unique needs of various industries. With a focus on innovation and customer satisfaction, the company delivers high-quality solutions that enhance operational efficiency and contribute to sustainable industrial practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top