For food processing industries, especially those involved in cocoa products, efficient and reliable material handling is crucial. Cocoa powder, with its fine particle size and hygienic requirements, demands specialized conveying solutions. Pneumatic conveying systems have emerged as a preferred method for transporting cocoa powder due to their ability to maintain product quality while ensuring operational efficiency. This article explores the fundamental principles behind cocoa powder pneumatic conveying and highlights key application scenarios where such systems excel.
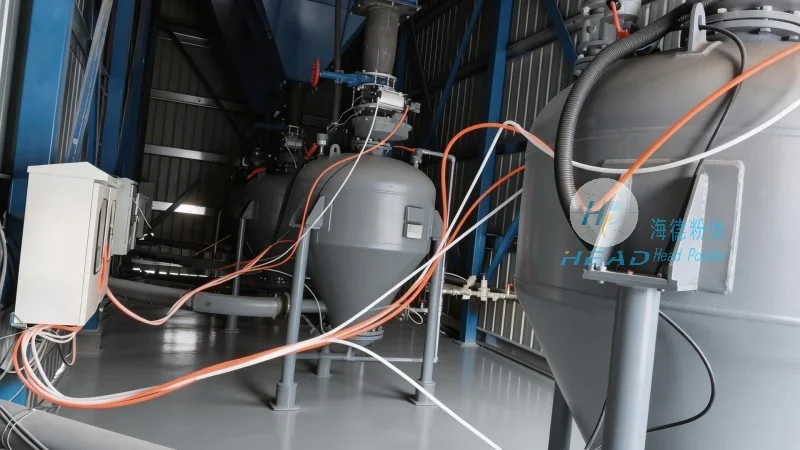
Pneumatic conveying operates by using air to transport bulk materials through a pipeline. The process can be categorized into two main types: aspiration (or suction) conveying and pressure (or blow) conveying. In aspiration systems, a vacuum is created at the inlet to draw material into the pipeline, while pressure systems use compressed air to push material forward. For cocoa powder, which is sensitive to moisture and contamination, the choice of system depends on factors such as material flow rate, distance, and the need for product containment.
The key components of a typical cocoa powder pneumatic conveying system include the inlet hopper, airlock feeder, conveying line, separator, and discharge outlet. The inlet hopper collects the cocoa powder, and the airlock feeder ensures a controlled, continuous flow into the pipeline. The conveying line transports the powder mixed with air, while the separator separates the powder from the air at the discharge end, often using cyclone or bag filters to maintain product purity. This closed-loop system minimizes exposure to external contaminants and ensures compliance with food safety standards.
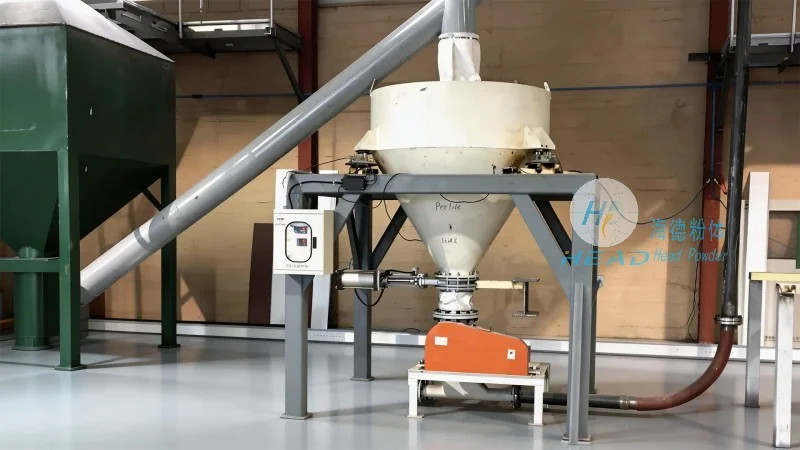
Cocoa powder pneumatic conveying is widely adopted in various industrial settings, particularly in the food and beverage sector. One primary application is in cocoa processing plants, where large volumes of cocoa powder need to be moved between storage silos, processing units, and packaging lines. The system’s ability to handle fine powders without clogging or degradation makes it ideal for maintaining product consistency. For example, in chocolate manufacturing, cocoa powder is often conveyed from storage tanks to mixing machines, where it is combined with other ingredients to form the base of chocolate products.
Another critical application is in food processing facilities that require hygienic and dust-free environments. Pneumatic conveying systems are designed with stainless steel components and sealed pipelines, reducing the risk of cross-contamination and ensuring that cocoa powder remains free from external particles. This is particularly important in facilities that handle multiple product lines or operate under strict regulatory standards, such as those in the EU or FDA guidelines. The system’s flexibility also allows for easy integration with existing production lines, minimizing downtime during installation or maintenance.
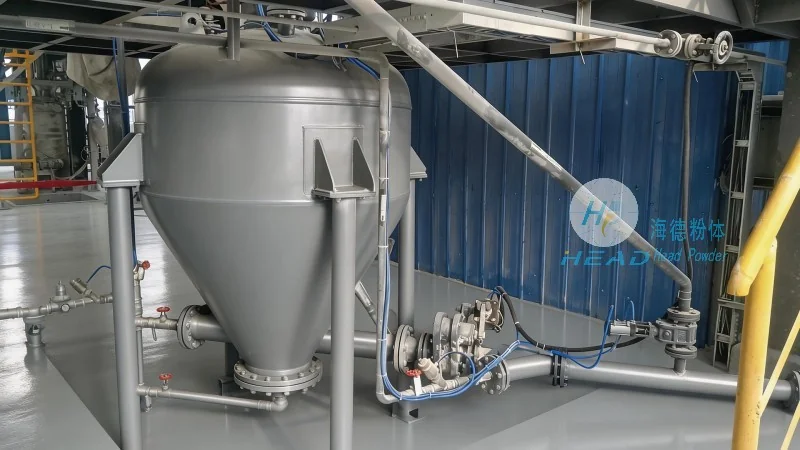
In addition to industrial applications, pneumatic conveying is used in research and development labs for testing new cocoa powder formulations. Researchers can precisely control the flow rate and particle size distribution using these systems, enabling accurate analysis of product properties. The ability to handle small batches of cocoa powder with high precision makes it a valuable tool in R&D, where product quality and consistency are paramount.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of cocoa powder applications. The company’s expertise lies in understanding the unique challenges of handling fine, hygienic powders, such as cocoa, and developing solutions that address these challenges effectively.
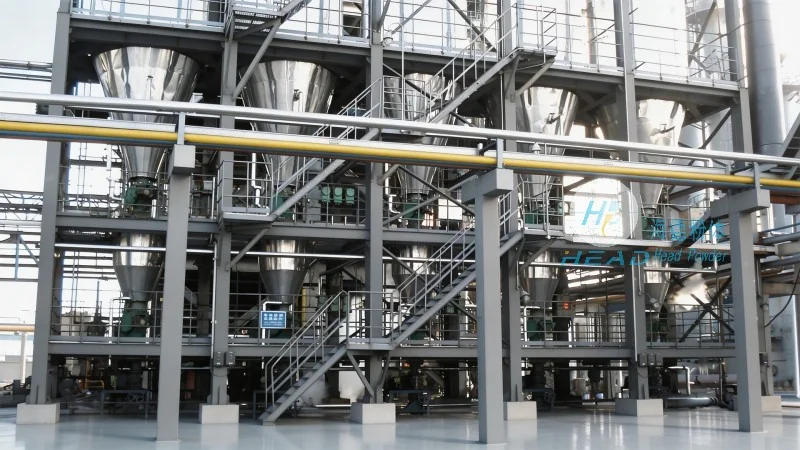
HeadPowder’s systems are engineered with high-efficiency separators that ensure minimal product loss and maximum air recovery. The company uses advanced materials, such as stainless steel and food-grade plastics, to construct components that are resistant to corrosion and easy to clean, meeting the stringent hygiene requirements of the food industry. Additionally, the company offers modular designs that allow for scalability, enabling clients to expand their conveying systems as their production needs grow.
The company’s approach to pneumatic conveying for cocoa powder emphasizes energy efficiency and operational reliability. By optimizing air flow rates and system pressure, HeadPowder’s solutions reduce energy consumption while maintaining consistent material transport. This not only lowers operational costs but also contributes to a more sustainable manufacturing process. Furthermore, the company provides comprehensive support, including installation, maintenance, and technical training, ensuring that clients can maximize the performance of their conveying systems over their lifespan.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top