This article provides an in-depth look at the working principle and key features of sugar material pneumatic conveying equipment, a critical component in the sugar processing industry. The equipment is designed to efficiently transport sugar cane or processed sugar materials through a pneumatic system, offering advantages in terms of speed, hygiene, and operational flexibility. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality solutions tailored to the specific needs of sugar processing facilities.
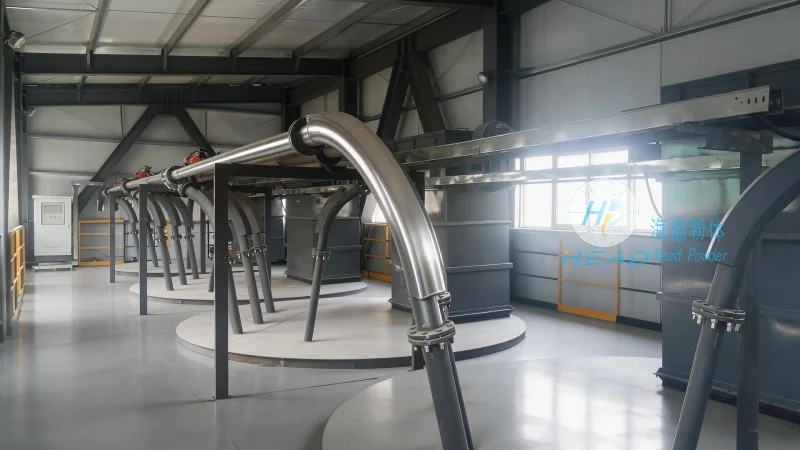
The core mechanism of sugar material pneumatic conveying equipment involves the use of air to transport bulk materials. The system typically operates by drawing air and sugar material into a hopper or feeding chamber. A fan or blower generates the necessary air pressure, which then propels the sugar particles through a pipeline network. The process can be categorized into two main types: dilute-phase and dense-phase conveying. Dilute-phase systems use higher air velocities to move materials quickly, while dense-phase systems employ lower velocities and higher pressure to ensure gentle handling of the sugar, minimizing product degradation and dust generation. The conveying line may include components such as cyclones, filters, and silos to separate the material from the air and store it efficiently. The entire system is controlled by a programmable logic controller (PLC) to regulate air flow, pressure, and material feed rates, ensuring consistent and reliable operation.
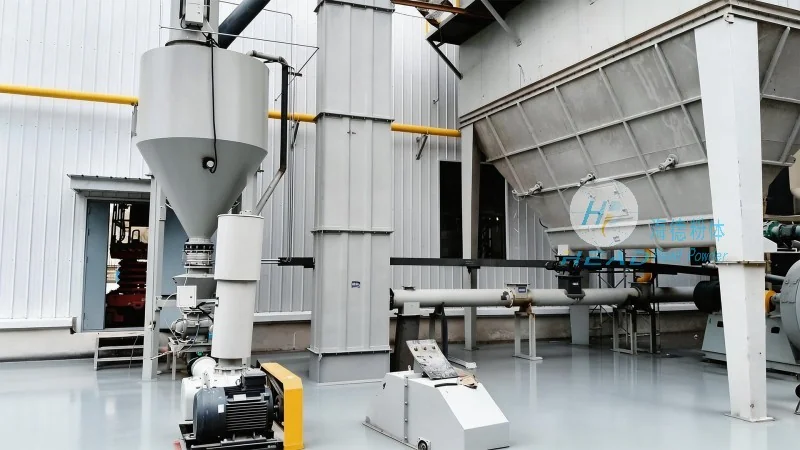
Shandong HeadPowder Engineering Co., Ltd. offers pneumatic conveying systems for sugar materials with several notable features that enhance performance and user experience. One of the primary advantages is the ability to handle fine or granular sugar without the need for mechanical components like belts or buckets, which can cause contamination or wear. The system is also highly hygienic, as it operates in a closed environment, preventing dust exposure and maintaining product purity. Additionally, the equipment is designed for easy maintenance, with accessible components and minimal downtime. The use of air as the conveying medium allows for flexible installation, as the pipeline can be routed around obstacles, and the system can be scaled to accommodate varying production volumes. Another key feature is the integration of dust collection and filtration systems, which ensures compliance with environmental regulations and maintains a clean working environment. The equipment also offers energy efficiency, as the air pressure and flow can be optimized to minimize power consumption while maintaining effective material transport.
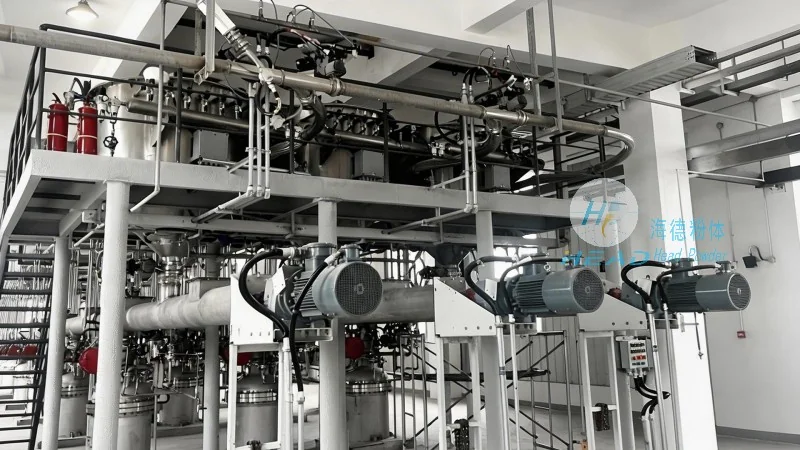
Sugar material pneumatic conveying equipment is widely used in various stages of sugar production, from raw sugar cane handling to refined sugar storage. In the initial stages, the system can transport freshly harvested sugar cane from the field to processing plants, reducing the need for manual handling and improving operational safety. During the refining process, the equipment efficiently moves sugar crystals through filtration and drying stages, ensuring consistent quality. The closed system also helps in maintaining temperature control, which is crucial for preserving the quality of the final product. For storage, the conveying system can transfer sugar from processing units to silos or packaging areas, enabling smooth inventory management. The benefits of using pneumatic conveying in sugar processing include increased productivity, reduced labor costs, improved product quality, and enhanced safety in the workplace. The system's ability to handle different sugar forms, such as granulated or powdered sugar, makes it versatile for various applications within the industry.
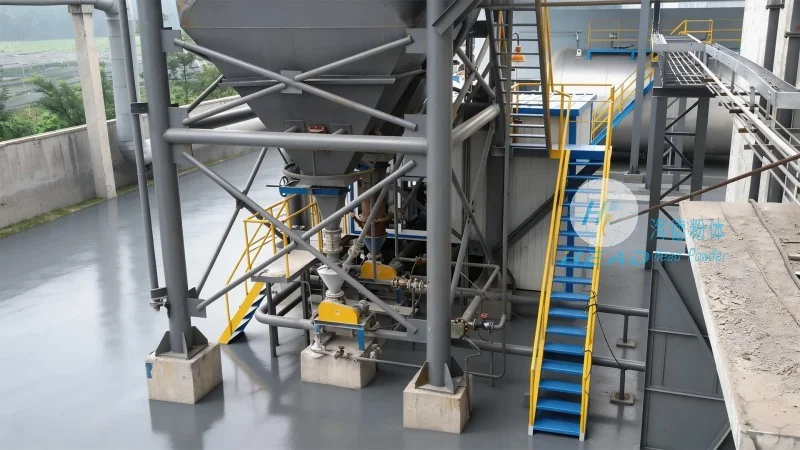
Shandong HeadPowder Engineering Co., Ltd. understands that each sugar processing facility has unique requirements, and therefore, offers customized pneumatic conveying solutions. The company provides comprehensive technical support, including site surveys and system design, to ensure that the equipment meets the specific needs of the client. Their team of engineers and technicians work closely with customers to develop solutions that optimize material flow, minimize energy consumption, and enhance overall operational efficiency. The company also offers after-sales support, including maintenance services and spare parts availability, to ensure the long-term performance of the equipment. By partnering with Shandong HeadPowder Engineering Co., Ltd., sugar processing plants can benefit from reliable, efficient, and cost-effective conveying systems that contribute to their overall success.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top