Multi-functional bulk material pneumatic conveying equipment represents a sophisticated solution for the efficient handling and transportation of various bulk materials in industrial settings. This equipment is designed to meet diverse operational requirements, offering flexibility and reliability in material processing applications. The technology behind such systems leverages the principles of pneumatic transport, where materials are conveyed through a pipeline using compressed air or other gas streams.
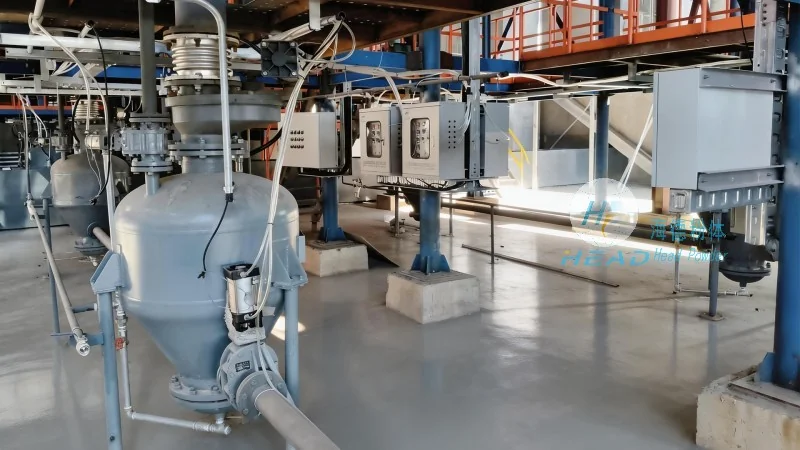
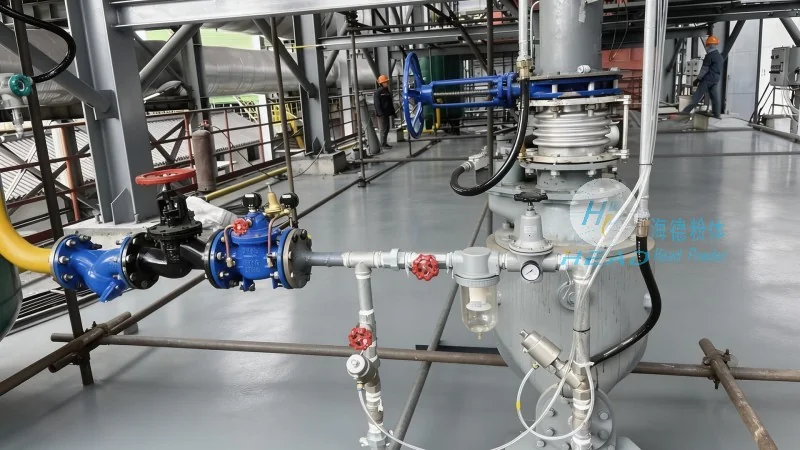
The core working principle of multi-functional pneumatic conveying equipment involves the creation of a flow of air or gas within a closed pipeline system. Materials, such as powders, granules, or fine particles, are introduced into the system either by gravity or through a feeding mechanism. The air stream, typically generated by a blower or compressor, carries the material particles along the pipeline. This process can be categorized into different modes, including dilute phase and dense phase conveying, each tailored to specific material characteristics and operational needs. In dilute phase systems, the material is dispersed as individual particles in the air stream, while in dense phase systems, the material is conveyed in a more concentrated form, often with higher air-to-material ratios. The equipment is equipped with components like feeders, cyclones, filters, and control valves to manage the flow, ensure material separation, and maintain system efficiency.
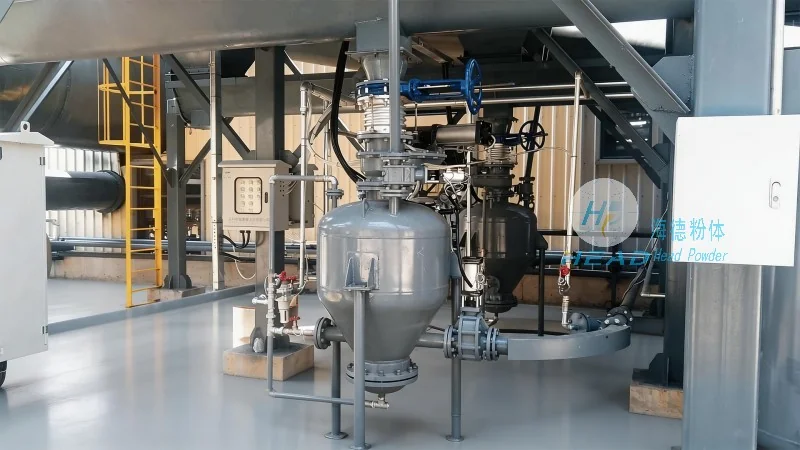
Multi-functional pneumatic conveying systems offer several distinct advantages that make them suitable for a wide range of industrial applications. One of the primary features is their ability to handle a broad spectrum of materials, including fine powders, abrasive particles, and even sensitive products that require gentle handling. The equipment is designed to minimize material degradation and contamination, ensuring product integrity throughout the conveying process. Another notable feature is the flexibility in system configuration, allowing for both short and long-distance transportation, as well as vertical and horizontal movement. This adaptability makes the equipment ideal for complex production lines where material flow needs to be integrated with other processes. Additionally, the systems are equipped with advanced control mechanisms that enable precise regulation of air pressure, flow rate, and material feed, enhancing operational efficiency and reducing energy consumption. The robust construction and durable components ensure long-term reliability, minimizing downtime and maintenance costs. Furthermore, the equipment is engineered to comply with safety standards, incorporating features like pressure relief valves and dust collection systems to maintain a safe working environment.
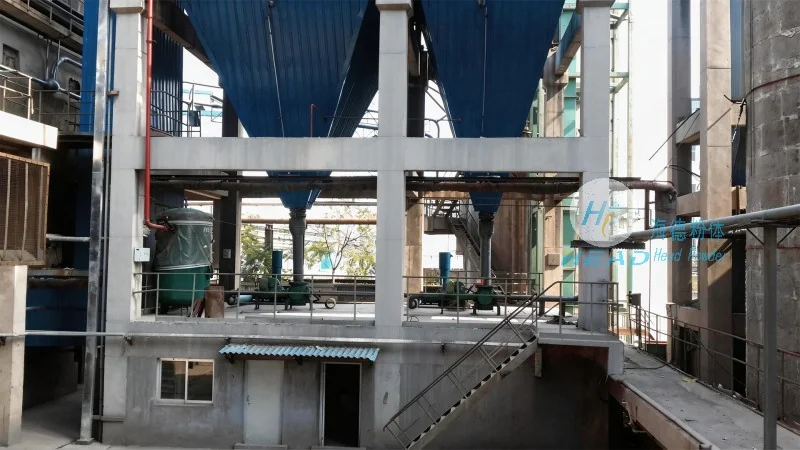
As a leading manufacturer in the field of bulk material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and supply of high-quality multi-functional pneumatic conveying equipment. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for industries requiring efficient and reliable material transport solutions. HeadPowder's products are engineered to meet international standards and are tailored to the specific needs of clients, ensuring optimal performance and durability. The company's headquarters is located in Shandong, China, where a team of experienced engineers and technicians work tirelessly to develop cutting-edge solutions that address the evolving demands of the industrial sector. By leveraging advanced technology and rigorous quality control processes, HeadPowder delivers equipment that not only meets but exceeds industry expectations, providing long-term value to its customers.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top