For industrial applications involving sulfur material handling, a pneumatic conveying system offers an efficient and reliable solution. This technology is particularly valuable in processes where bulk sulfur needs to be transported from one location to another within a facility or between different sites. The system's design and operation are tailored to handle the unique properties of sulfur, ensuring safe and effective material transfer.
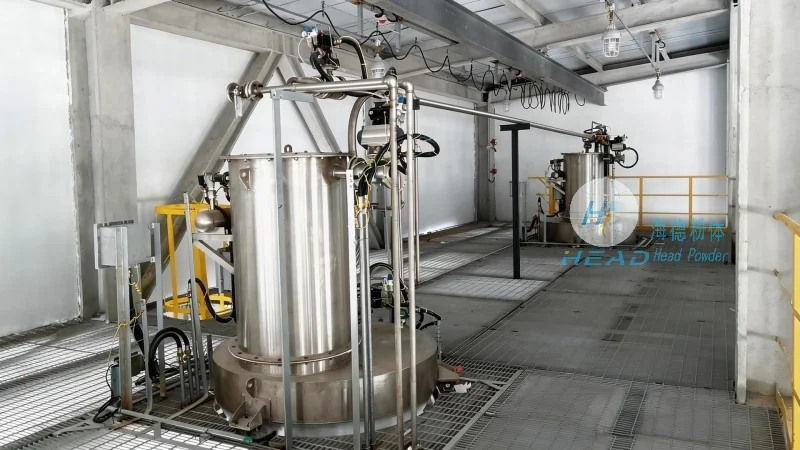
A sulfur material pneumatic conveying system is a type of bulk material handling equipment that uses compressed air or other gases to transport solid particles through a pipeline. Unlike traditional mechanical conveying methods, such as belt conveyors or screw conveyors, pneumatic systems can handle materials that are difficult to move with mechanical means, including sulfur, which may have varying particle sizes and moisture content. The system typically consists of a feeding device, a conveying line, a control system, and a discharge unit. Each component works in tandem to ensure smooth and continuous material transport.
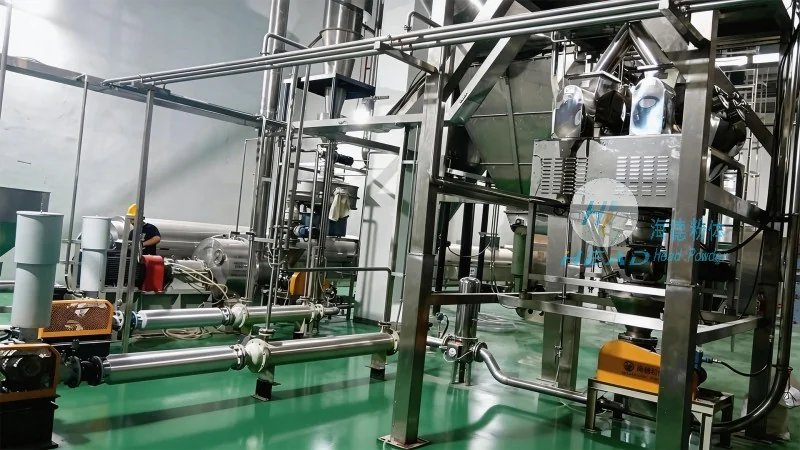
The core of a sulfur material pneumatic conveying system lies in its operation based on the principle of fluidization and suspension. The process begins with the sulfur material being fed into the system, often through a hopper or a feeder that ensures a consistent flow rate. Compressed air is then introduced into the conveying line, creating a flow that lifts and transports the sulfur particles. The air velocity within the pipeline is carefully controlled to maintain the material in a suspended state, preventing it from settling or clogging the system. The conveying line may include bends, expansions, or other components that require adjustments to the air flow to maintain optimal transport conditions. The system's control system monitors parameters such as air pressure, flow rate, and material level, ensuring that the operation remains stable and efficient. When the material reaches the discharge point, the air flow is adjusted to allow the sulfur to be deposited into the receiving container or process unit.
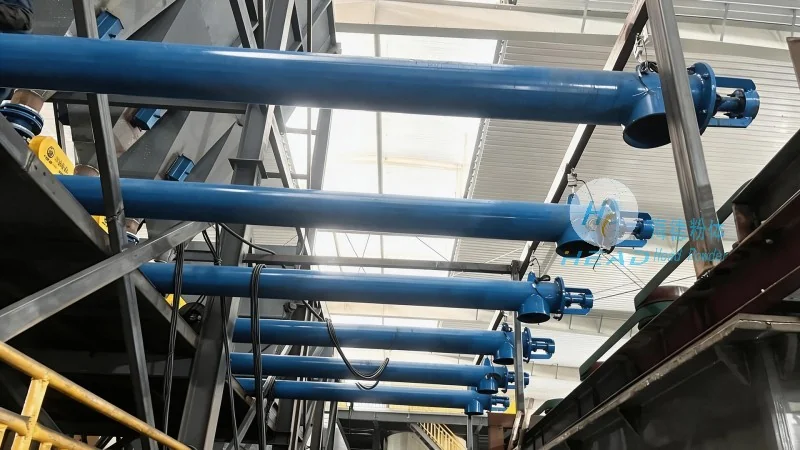
Several key features distinguish a sulfur material pneumatic conveying system from other handling solutions. First, the system offers a high degree of flexibility in terms of layout and installation. It can be configured to follow the existing infrastructure of a facility, minimizing the need for extensive civil works. Second, the system is highly efficient in terms of energy consumption, as it uses compressed air to move the material, which can be more economical than mechanical conveyors, especially for long-distance or high-volume transport. Third, the system provides excellent material containment, as the entire transport process occurs within a sealed pipeline, reducing the risk of dust emissions and environmental contamination. Fourth, the system is easy to maintain and operate, with minimal moving parts that require regular servicing. Additionally, the system can be integrated with other process equipment, such as storage tanks or reactors, to form a complete material handling solution. The durability of the system components, particularly those in contact with sulfur, is also a critical feature, as sulfur can be corrosive and abrasive. Materials like stainless steel or specialized coatings are used to ensure long-term performance and reliability.
Sulfur material pneumatic conveying systems are widely used in various industrial applications, including the chemical industry, where sulfur is used as a raw material for the production of sulfuric acid, fertilizers, and other chemicals. In the petrochemical sector, the system is employed to transport sulfur from storage facilities to processing units. The system is also utilized in the mining industry, where sulfur is extracted from ore and needs to be transported to processing plants. The benefits of using such a system in these applications include improved safety, as the material is contained within the pipeline, reducing the risk of accidents or environmental hazards. Additionally, the system enhances productivity by enabling continuous and automated material transport, reducing downtime and labor costs. The system's ability to handle varying sulfur properties, such as different particle sizes or moisture levels, makes it a versatile solution for diverse industrial needs.
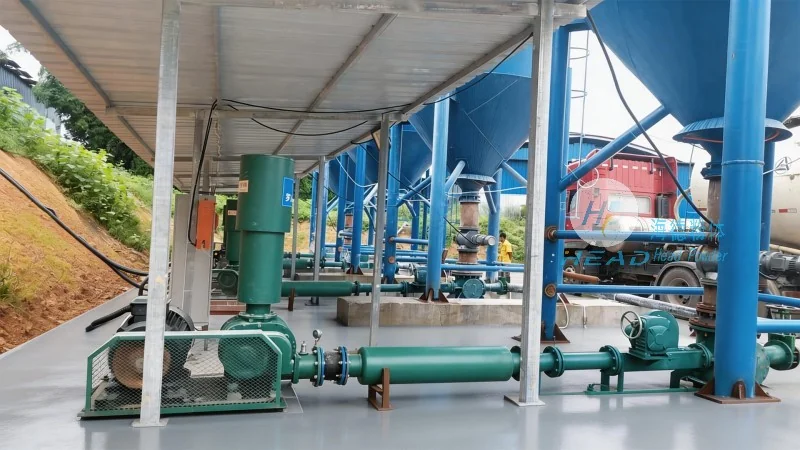
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of pneumatic conveying systems and related equipment. With years of experience in the industry, the company specializes in designing and manufacturing customized solutions for bulk material handling, including systems for sulfur and other challenging materials. HeadPowder's expertise lies in understanding the unique requirements of each application and providing tailored solutions that meet the specific needs of clients. The company's products are known for their high quality, durability, and efficiency, making them a trusted choice for industrial facilities worldwide. HeadPowder's commitment to innovation and customer satisfaction has established it as a key player in the pneumatic conveying equipment market. The company's facilities are located in Shandong, China, where it employs a team of skilled engineers and technicians who work closely with clients to develop and implement effective material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top