HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for soil and powder materials. This article provides an in-depth exploration of the working principle and key features of such systems, highlighting their efficiency and practical applications in various industries.
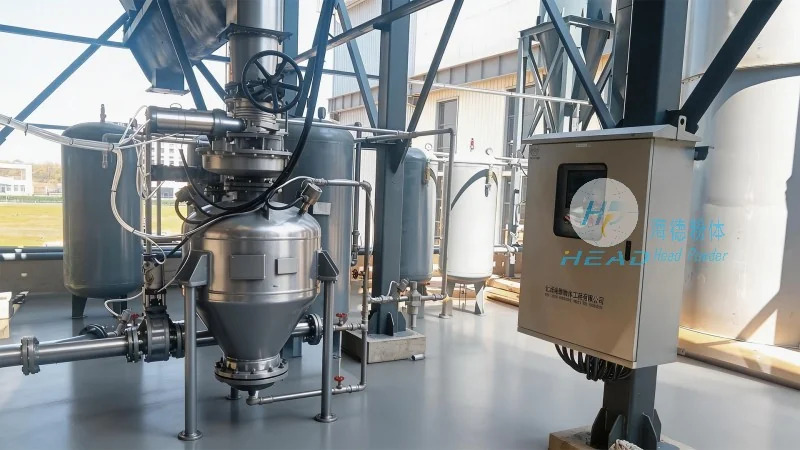
Pneumatic conveying systems are essential for the transport of dry, fine materials like soil powders over long distances or within complex processing facilities. These systems utilize air pressure to move materials through pipelines, offering a flexible and often more cost-effective alternative to traditional mechanical conveying methods. HeadPowder's systems are engineered to handle the unique challenges of soil powders, including their variable particle sizes, moisture content, and potential for dust generation.
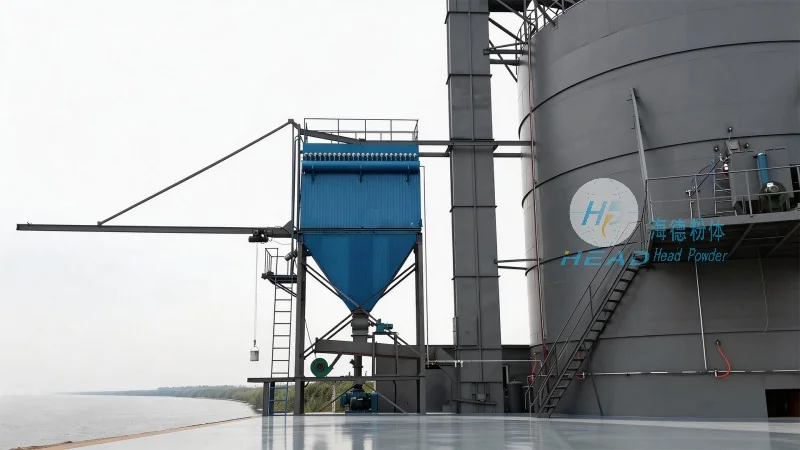
The core mechanism of a pneumatic conveying system involves the generation of airflow within a pipeline, which then lifts and transports the material. In the case of soil powder systems, the process typically begins with material feeding into a hopper or feeder. From there, the material is introduced into the pipeline, often with the assistance of a rotary valve or feeder, ensuring a consistent flow. The system then uses a blower or compressor to create the necessary air pressure, which propels the soil powder through the pipeline. The design of the system, including the choice of blower type (positive displacement or centrifugal), pipeline diameter, and bends, is critical to maintaining optimal airflow and material transport efficiency. The system may also incorporate features such as air separation or cyclone separators at the discharge end to separate the material from the air stream, ensuring clean material delivery and reducing air consumption.
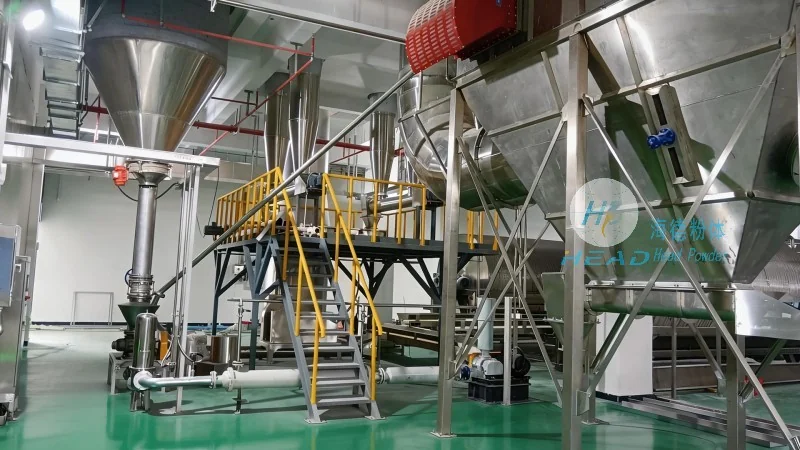
HeadPowder's soil powder pneumatic conveying systems are characterized by several key features that enhance performance and reliability. One of the primary advantages is the ability to transport materials in a closed system, which minimizes dust exposure and environmental contamination. This is particularly important for soil powders, which can be fine and easily airborne. The systems are also designed for high efficiency, with optimized airflow and pipeline configurations that reduce energy consumption while maintaining consistent material flow rates. Another notable feature is the flexibility of the system, allowing for easy integration with existing processing equipment or expansion to accommodate increased material handling needs. The use of durable materials, such as stainless steel or specialized coatings, ensures longevity and resistance to corrosion, especially when handling soil powders that may contain moisture or acidic components. Additionally, the systems are equipped with monitoring and control features, enabling operators to adjust parameters in real-time and maintain optimal performance. This includes pressure sensors, flow meters, and automated controls that help prevent system overloads or blockages, ensuring continuous and reliable operation.
Soil powder pneumatic conveying systems are widely used in various industries where the handling of fine, dry materials is required. In the construction industry, these systems are used for transporting soil, sand, and other aggregates from stockpiles to processing plants or construction sites. In the agricultural sector, they can be employed for the transport of soil samples or fertilizer powders between storage and application areas. The mining industry also benefits from such systems for transporting ore dust or fine mineral powders. Furthermore, in the environmental and waste management fields, pneumatic conveying systems are used for the transport of soil from remediation sites or for the handling of waste materials in recycling facilities. The versatility of HeadPowder's systems makes them suitable for a range of applications, from small-scale operations to large industrial plants, providing a reliable solution for material transport needs.
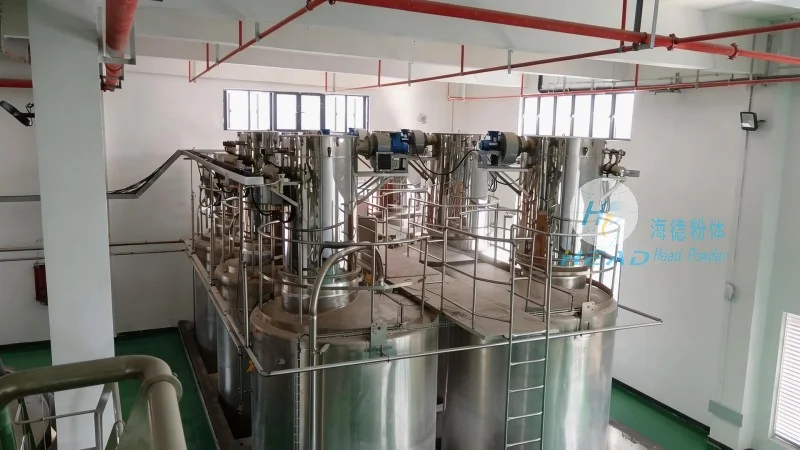
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of advanced pneumatic conveying systems for soil and powder materials. By focusing on the working principle and key features of these systems, HeadPowder ensures that their solutions are efficient, reliable, and tailored to the specific needs of their clients. The company's expertise in system design, material selection, and integration allows them to deliver high-performance pneumatic conveying solutions that enhance productivity and reduce operational costs. With a commitment to quality and innovation, HeadPowder continues to be a leader in the field of material handling technology, providing effective solutions for the transport of soil powders and other fine materials across various industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top