For industrial applications that require the efficient and safe handling of bulk powders, the powder silo pneumatic conveying system stands out as a critical solution. This system is designed to transport dry powders from storage silos to processing units or other destinations within a facility. The core of this technology lies in the pneumatic conveying method, which utilizes compressed air to move materials through a network of pipes and components.
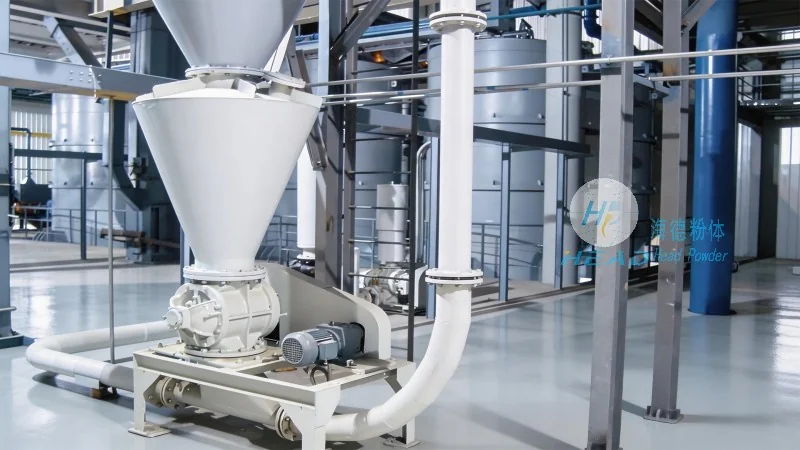
The operation of a powder silo pneumatic conveying system begins with the material being stored in a silo. The system then draws the powder from the silo using a vacuum or pressure source, depending on the specific design. Compressed air is introduced into the system, creating a flow that propels the powder particles through the pipeline. The air-powder mixture travels through the conveying line, which may include bends, filters, and control valves, before being deposited at the destination. The entire process is automated, ensuring consistent and reliable material transfer without the need for manual intervention.
One of the primary advantages of this system is its ability to handle a wide range of powder types, from fine powders to bulkier materials. The design allows for minimal product degradation, as the material is not subjected to mechanical stress during transport. Additionally, the system offers high efficiency in terms of energy consumption and throughput, making it suitable for high-volume production environments. Safety is another critical feature, as the enclosed system prevents dust emissions and protects personnel from exposure to powders. The modular nature of the system also facilitates easy integration with existing industrial setups, reducing installation time and costs.
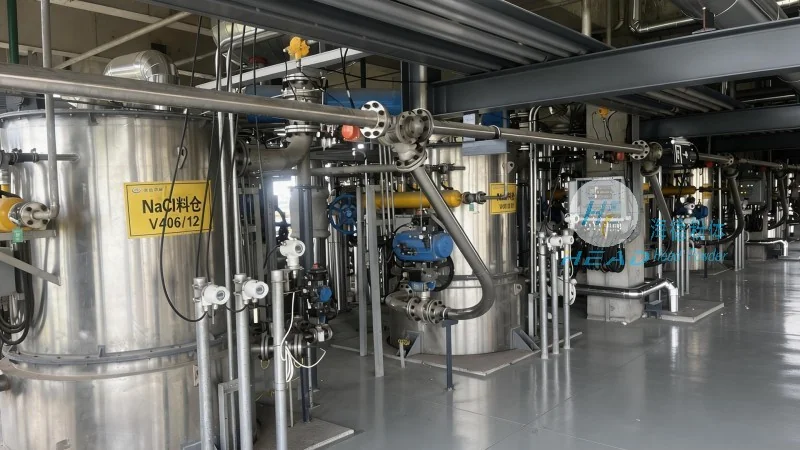
As a leading manufacturer in the field of powder handling equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner for industries such as pharmaceuticals, food processing, chemicals, and more. HeadPowder's commitment to quality is evident in its adherence to international standards and rigorous testing protocols, ensuring that each system meets the highest performance and safety requirements. The company's headquarters is located in Shandong, China, where its team of experts continuously develops new solutions to meet evolving industry needs.
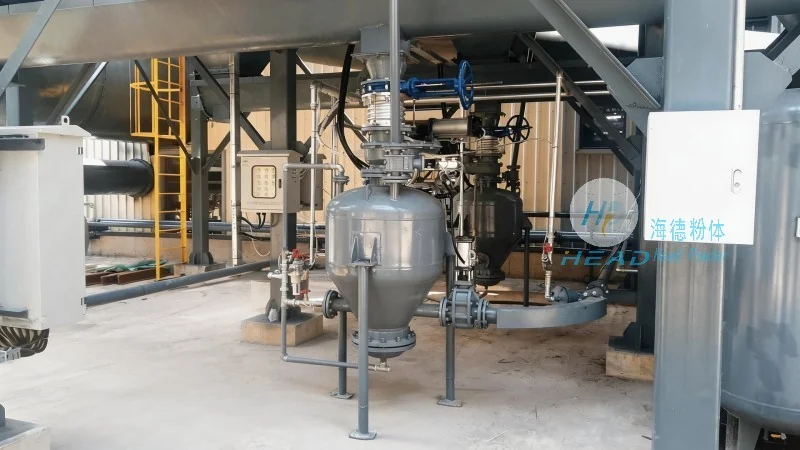
Powder silo pneumatic conveying systems are widely used across various industries due to their versatility and reliability. In the pharmaceutical sector, for example, the system ensures the safe and hygienic transfer of active ingredients and excipients, maintaining product purity. In the food industry, it helps in the efficient handling of powders like flour, sugar, and spices, while preserving their quality and flavor. The chemical industry benefits from the system's ability to handle abrasive and corrosive powders without damaging the equipment. Overall, the benefits of these systems include improved productivity, reduced labor costs, enhanced safety, and compliance with environmental regulations.
Understanding the working principle and features of powder silo pneumatic conveying systems is essential for industries seeking to optimize their material handling processes. The combination of efficient pneumatic technology and robust design makes this system a superior choice for transporting bulk powders. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can leverage these advanced solutions to enhance their operational efficiency and meet the demands of modern industrial production. By investing in such systems, companies can achieve sustainable growth while maintaining high standards of safety and quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top