HeadPowder, a professional provider of activated carbon powder conveying systems, specializes in delivering efficient and reliable solutions for the transportation of activated carbon powders. Based in Shandong, China, the company leverages advanced engineering and industry expertise to meet diverse industrial needs. This article explores the working principle and key features of such systems, providing insights into their functionality and benefits.
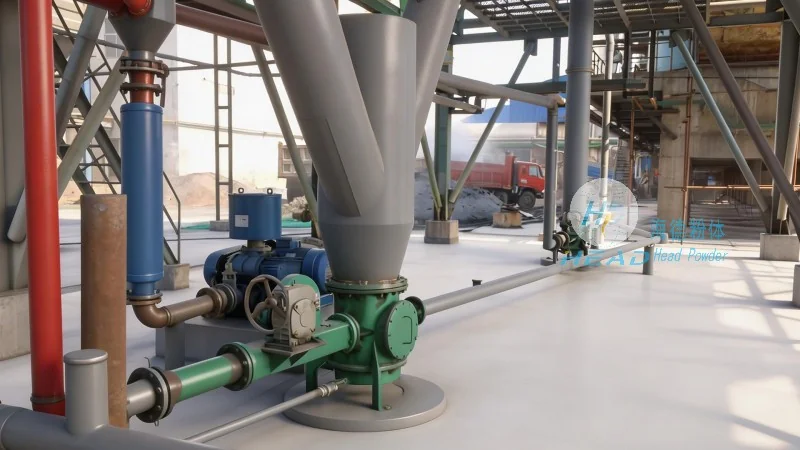
HeadPowder Engineering Co., Ltd. is a prominent manufacturer and supplier of activated carbon powder conveying systems. With a strong presence in Shandong, China, the company has established itself as a trusted partner for industries requiring safe and efficient powder handling. The company’s commitment to quality, innovation, and customer satisfaction drives the development of cutting-edge solutions tailored to specific operational requirements.
The activated carbon powder conveying system operates on principles designed to handle the unique characteristics of activated carbon powders, such as their fine particle size, light weight, and tendency to create dust. The system typically consists of several key components, including a hopper for material storage, a conveyor mechanism (either pneumatic or mechanical), and a control unit for regulating the flow. The process begins with the activated carbon powder being fed into the hopper, where it is then transferred to the conveyor. In pneumatic systems, compressed air is used to create a flow that transports the powder through a network of pipes, ensuring minimal contact with the environment and reducing the risk of dust dispersion. Mechanical systems, on the other hand, rely on screw conveyors or belt systems to move the powder, often in a closed loop to maintain containment. The control unit monitors parameters like pressure, flow rate, and temperature, adjusting the system to maintain optimal performance and prevent issues like blockages or overloading.
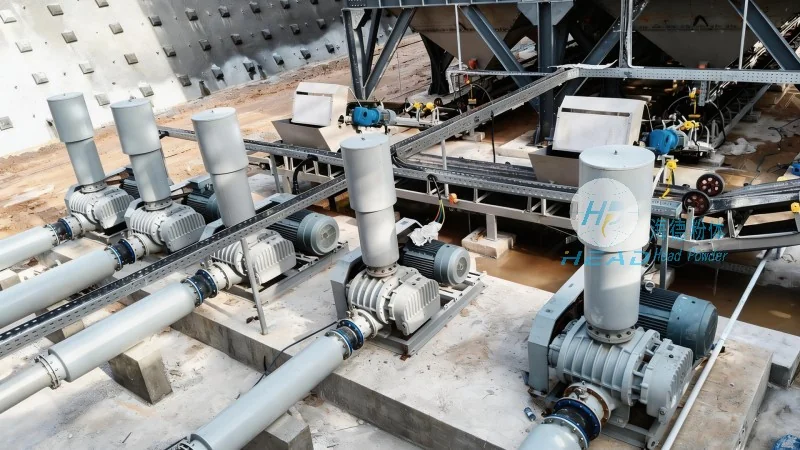
The activated carbon powder conveying system developed by HeadPowder offers several distinct features and advantages that enhance operational efficiency and safety. One of the primary features is its ability to maintain a closed environment, which significantly reduces dust emissions and minimizes the risk of contamination. This is crucial for industries where air quality and material purity are critical, such as in water treatment, air purification, and chemical processing. The system also ensures low material loss during transportation, as the enclosed design prevents powder spillage and leakage. Another key advantage is its adaptability to various operational scales, from small-scale applications to large industrial plants. The modular design allows for easy expansion or integration with existing infrastructure, making it suitable for both new installations and retrofitting in existing facilities.
Efficiency is a core aspect of the activated carbon powder conveying system, with several factors contributing to its high performance. The system’s design optimizes the flow of powder, reducing energy consumption by minimizing pressure drops and ensuring consistent material transport. Advanced control technologies, such as variable frequency drives, allow for precise regulation of the conveyor speed, adapting to changes in material load and preventing overexertion on the equipment. This not only improves energy efficiency but also extends the lifespan of the components. Additionally, the system incorporates features like automatic cleaning and maintenance alerts, which help in reducing downtime and ensuring continuous operation. The use of high-quality materials in the construction of the conveyor components, such as corrosion-resistant metals and durable plastics, further enhances the system’s longevity and reliability.
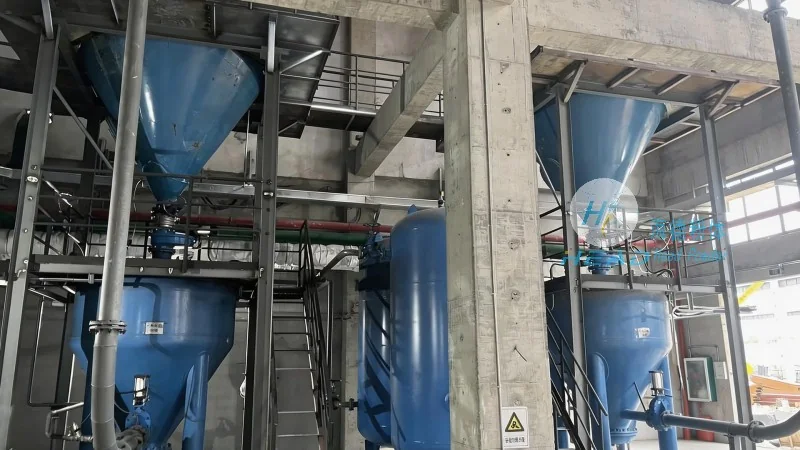
HeadPowder’s activated carbon powder conveying system places a strong emphasis on environmental and safety considerations. The closed-loop design and dust control mechanisms comply with stringent environmental regulations, ensuring that the operation does not contribute to air pollution or soil contamination. The system is equipped with safety features like pressure relief valves and emergency shut-off mechanisms, which protect both personnel and equipment from potential hazards. Furthermore, the use of activated carbon, a widely recognized adsorbent, aligns with sustainable practices, as it can be regenerated and reused, reducing waste and environmental impact. The company’s commitment to safety and environmental responsibility is reflected in its adherence to international standards and continuous improvement of its products.
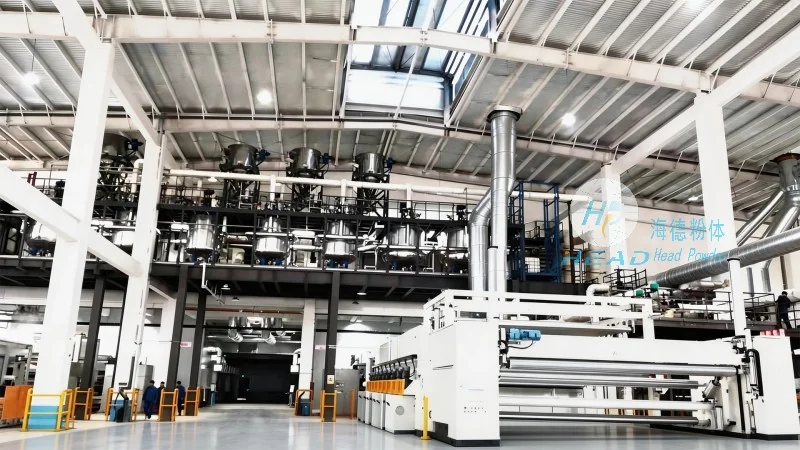
HeadPowder understands that different industries have unique requirements, and the activated carbon powder conveying system is designed to offer flexibility in customization. The company works closely with clients to understand their specific needs, whether it’s for a small laboratory-scale system or a large-scale industrial setup. Customization options include adjustments to the conveyor capacity, material handling speed, and integration with other processing equipment. The system can be tailored to handle different types of activated carbon powders, including powdered activated carbon (PAC) used in water treatment and air purification, as well as other fine powders that require similar handling. This adaptability makes the system suitable for a wide range of applications, from industrial wastewater treatment to air filtration in manufacturing plants.
In summary, the activated carbon powder conveying system from HeadPowder Engineering Co., Ltd. combines advanced technology, robust design, and user-friendly features to provide reliable and efficient solutions for the transportation of activated carbon powders. The system’s working principle, centered on enclosed and controlled material handling, ensures minimal environmental impact and high operational efficiency. Key features such as dust control, low material loss, and adaptability to various scales make it an ideal choice for industries seeking sustainable and safe powder handling solutions. With a strong presence in Shandong, China, HeadPowder continues to innovate and deliver high-quality products that meet the evolving needs of the market, solidifying its position as a leader in the activated carbon powder conveying industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top